

Technical Parameters and Conveying System for Nanopowders
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for nanopowder processing, with a focus on precise technical parameters and efficient conveying systems. This article explores the critical aspects of nanopowder technical specifications and the engineering processes involved in their handling and transportation.
Key Technical Parameters of Nanopowders
When working with nanopowders, understanding their fundamental technical parameters is essential for ensuring optimal performance and safety in industrial applications. These parameters include particle size distribution, which directly impacts the powder's surface area and reactivity. The average particle diameter, often measured in nanometers, is a primary indicator of the powder's physical properties. For instance, a narrower particle size distribution can lead to more consistent material behavior, while a broader range may affect flow characteristics and compaction. Additionally, density and bulk density are crucial for storage and handling, as they influence how the powder behaves in containers and during transport. The chemical composition and purity levels are also vital, as impurities can alter the powder's performance in end-use applications. Shandong HeadPowder Engineering Co., Ltd. adheres to strict quality control measures to ensure that all nanopowders meet the required specifications, guaranteeing reliability for clients across various industries.
Conveying System Design and Functionality
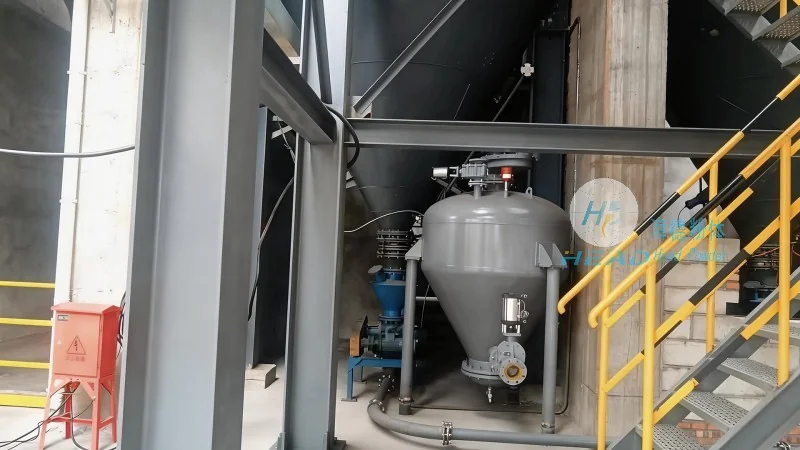
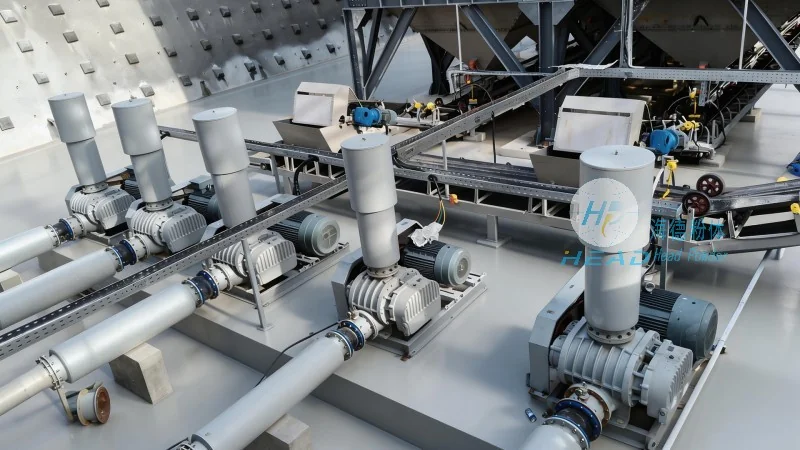
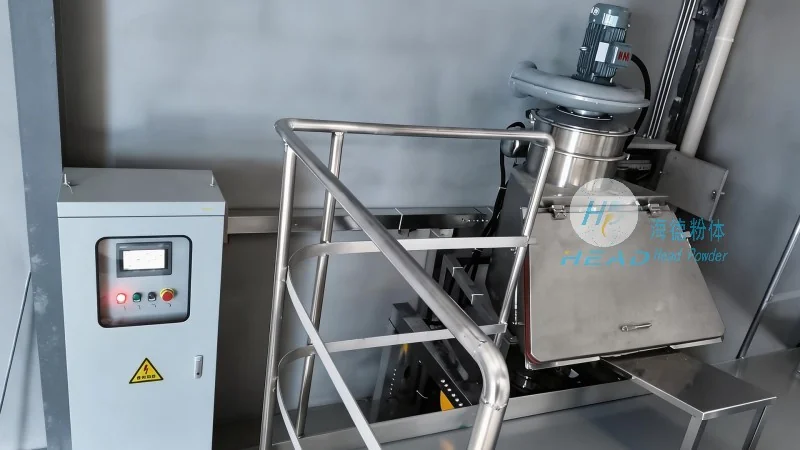
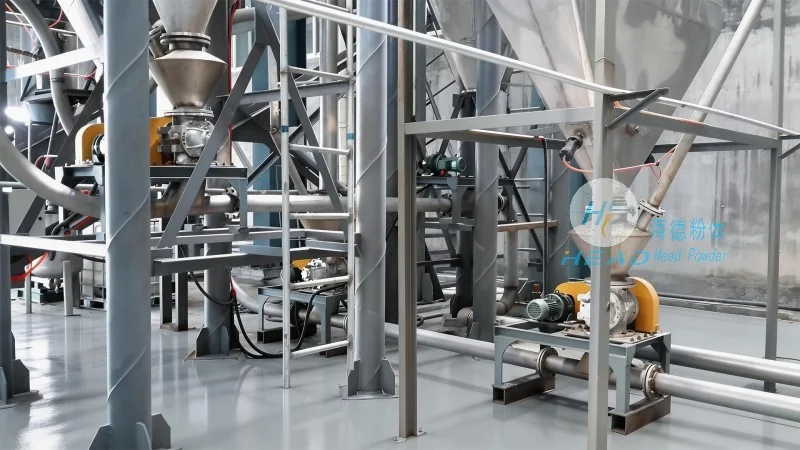
The efficient transportation of nanopowders requires specialized conveying systems that minimize particle degradation and maintain product integrity. At Shandong HeadPowder Engineering Co., Ltd., our conveying systems are engineered to handle the unique challenges posed by nanopowders, such as their fine particle size and tendency to agglomerate. The systems typically incorporate components like rotary valves, airlocks, and pneumatic or mechanical conveyors. Rotary valves are used to control the flow of powder from storage silos to processing equipment, ensuring a consistent and controlled discharge. Airlocks, often equipped with filters, prevent dust leakage and maintain a clean environment. Pneumatic conveying systems, which use compressed air to transport the powder, are particularly effective for handling fine powders, as they minimize particle attrition and prevent contamination. Mechanical conveyors, such as screw conveyors or belt conveyors, are also utilized in some applications, especially for larger volumes or when the powder is less sensitive to air flow. Our engineers design each conveying system based on the specific nanopowder characteristics, ensuring that the process is both efficient and safe. The integration of these components into a cohesive system allows for seamless material handling from storage to processing, enhancing overall operational efficiency.
Process Integration and Industrial Applications
The technical parameters of nanopowders and the design of conveying systems are closely linked to the broader industrial processes in which they are used. For example, in the production of advanced materials like ceramics or composites, the particle size and distribution of the nanopowder directly affect the final product's mechanical properties and thermal stability. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to tailor both the nanopowder specifications and the conveying system to meet the specific requirements of their end-use applications. This integration ensures that the powder is delivered in the correct form and quantity, supporting high-quality manufacturing outcomes. The company's expertise in process engineering enables the optimization of the entire workflow, from raw material handling to final product delivery. By focusing on the precise technical parameters and reliable conveying systems, Shandong HeadPowder Engineering Co., Ltd. supports industries such as electronics, pharmaceuticals, and aerospace, where the quality of nanopowders is paramount. The combination of rigorous quality control and advanced engineering ensures that clients receive products that meet their exact needs, contributing to the success of their operations.