

What is a Bulk Material Mixing Pneumatic Conveying System? What Are Its Design Principles?
Bulk material mixing pneumatic conveying systems are specialized industrial equipment designed to transport and blend various dry bulk materials efficiently. These systems utilize air as the conveying medium to move powders, granules, and other particulate materials from one location to another while simultaneously ensuring a uniform mixture. The core function of such systems is to combine different raw materials in precise ratios, which is crucial for applications in pharmaceuticals, food processing, chemical manufacturing, and other industries where consistency and quality control are paramount. By leveraging the principles of pneumatic transport, these systems offer a cost-effective and reliable solution for material handling and mixing, addressing the challenges of traditional mechanical methods.
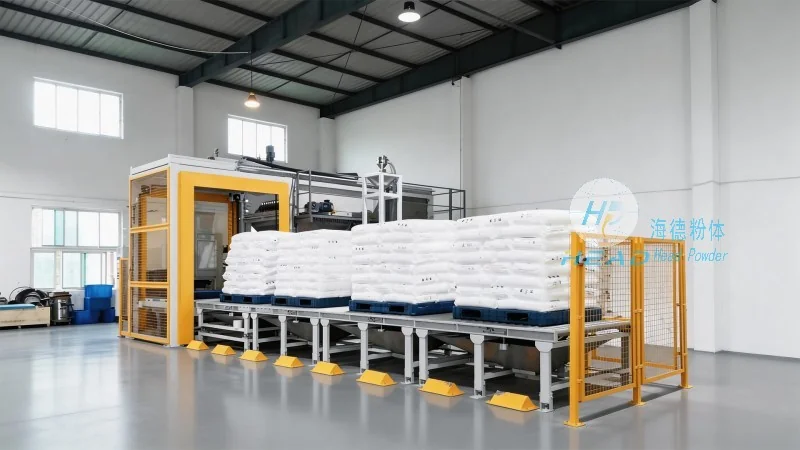
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in the design, development, and production of advanced pneumatic conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking reliable solutions for material transport and mixing. HeadPowder's facilities are located in Shandong, China, where the company leverages its expertise and state-of-the-art technology to deliver customized equipment tailored to specific industrial needs. The company's team of engineers and technicians work closely with clients to understand their unique requirements, ensuring that the final product meets both functional and performance standards.
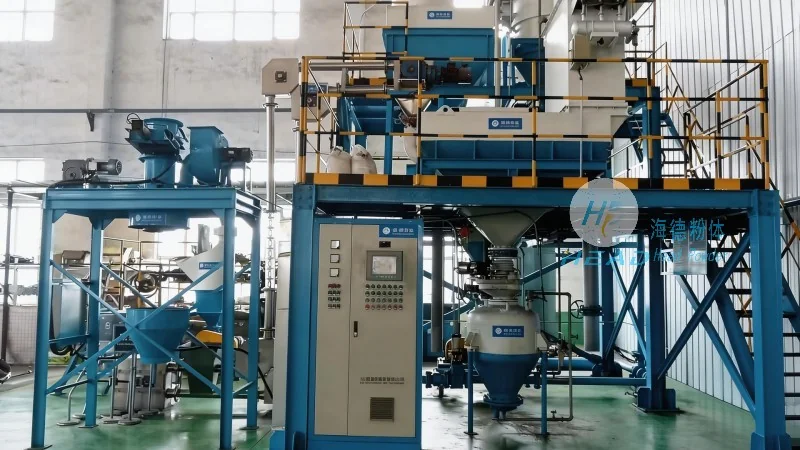
The Design Principles of Pneumatic Conveying Systems for Material Mixing
The design of a bulk material mixing pneumatic conveying system involves several key principles that ensure optimal performance and efficiency. The primary design considerations include the selection of the appropriate conveying method (e.g., pressure or vacuum systems), the determination of the air velocity and pressure required to move the material, and the configuration of the system components such as the hopper, ducts, and mixing chambers. A critical aspect of the design is the integration of mixing mechanisms, which may include rotary valves, agitators, or special duct designs that promote thorough blending of the materials as they are conveyed. The system must also account for factors like material properties (e.g., particle size, density, and flowability) and the desired mixing ratio to achieve the required homogeneity. Engineers at HeadPowder employ advanced computational fluid dynamics (CFD) and material flow analysis to optimize the system design, ensuring that the conveying process is both efficient and gentle on the materials being handled.
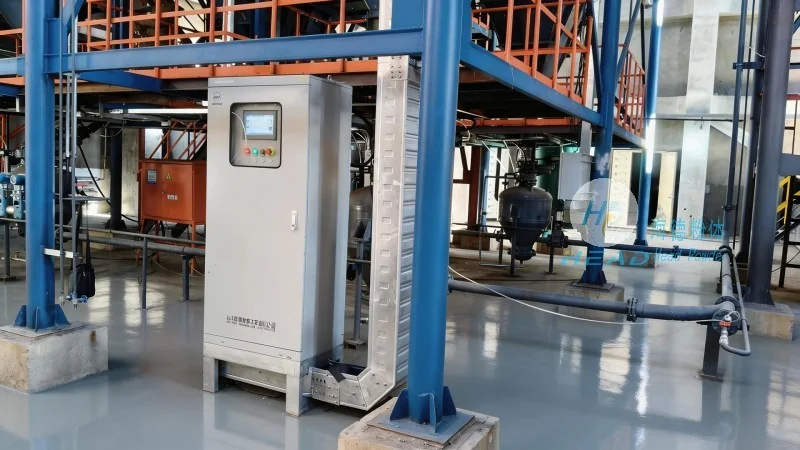
Key Features and Benefits of Bulk Material Mixing Pneumatic Conveying Systems
Bulk material mixing pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These systems eliminate the need for mechanical components like belts or screws, reducing maintenance costs and minimizing the risk of material contamination. The use of air as the conveying medium allows for gentle handling of delicate materials, preventing degradation or agglomeration. Additionally, the systems can be designed for both pressure and vacuum operations, providing flexibility in material handling applications. The ability to mix materials in real-time during the conveying process ensures that the final product meets strict quality standards, which is essential for industries where product consistency is critical. Furthermore, pneumatic conveying systems are highly scalable, allowing for easy expansion or modification to accommodate changing production needs without significant downtime.
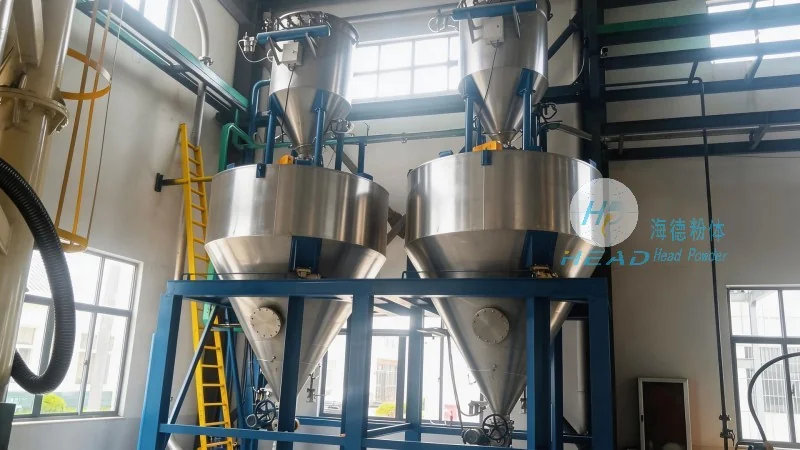
Customization and Application Examples
HeadPowder understands that each industrial application has unique requirements, and therefore, offers comprehensive customization options for bulk material mixing pneumatic conveying systems. The company works with clients to develop solutions that address specific challenges, such as handling abrasive materials, managing high temperatures, or ensuring compliance with regulatory standards. For example, in the pharmaceutical industry, where product purity is non-negotiable, HeadPowder designs systems with stainless steel components and closed-loop conveying to prevent contamination. In the food processing sector, the systems are equipped with sanitary design features to meet food safety regulations. These tailored solutions demonstrate HeadPowder's commitment to providing reliable and efficient equipment that enhances operational efficiency and product quality.