

What is a Chocolate Powder Conveyor? What Are Its Design Principles?
Chocolate powder conveyors are specialized equipment designed to handle and transport chocolate powder efficiently in industrial settings. These systems are crucial for chocolate manufacturers, as they ensure the smooth and hygienic movement of chocolate powder from storage to processing areas. The design of these conveyors is tailored to meet the unique characteristics of chocolate powder, such as its fine particle size, hygroscopic nature, and the need for contamination-free handling. Understanding the function and design principles of chocolate powder conveyors is essential for optimizing production processes and maintaining product quality.
Key Design Principles of Chocolate Powder Conveyors
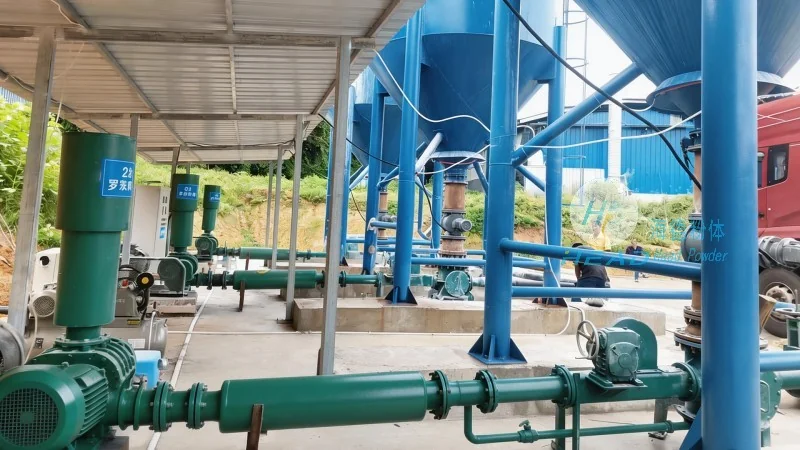
The design of a chocolate powder conveyor is based on several critical principles that address the specific challenges of handling chocolate powder. First, the conveyor must ensure minimal product degradation, which includes preventing clumping, agglomeration, and moisture absorption. This is achieved through the use of gentle handling mechanisms, such as belt conveyors with soft materials or pneumatic systems that use low-pressure air to move the powder without causing damage. Second, the conveyor must maintain a hygienic environment, which is vital in food processing industries. Materials used in the construction of the conveyor, such as stainless steel, are chosen for their resistance to corrosion and ease of cleaning. Additionally, the design incorporates features like smooth surfaces and minimal dead zones to prevent the accumulation of chocolate powder, which could lead to contamination or spoilage.
Components and Working Mechanisms of Chocolate Powder Conveyors
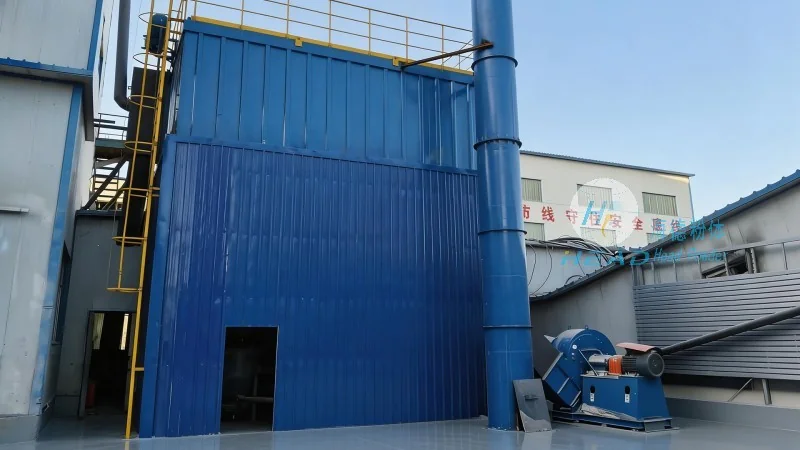
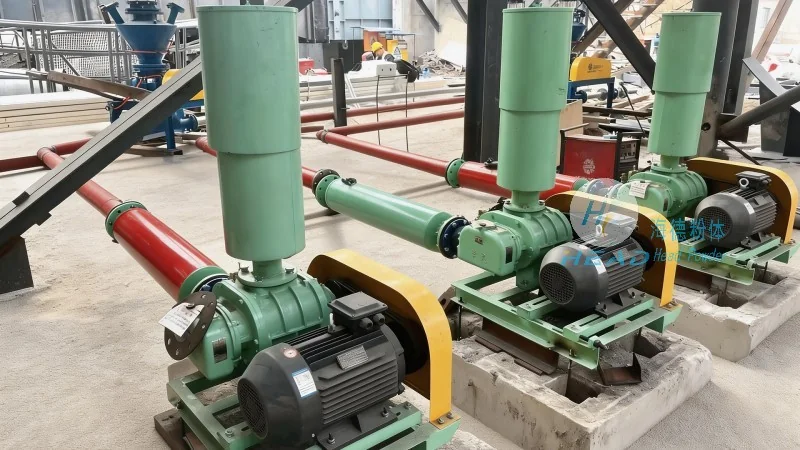
Chocolate powder conveyors typically consist of several key components that work together to achieve efficient powder transport. The primary components include a hopper for material storage, a conveyor belt or pneumatic tube, and a control system for operation. The hopper is designed to hold a large quantity of chocolate powder while maintaining a consistent flow into the conveyor. The conveyor belt, often made of food-grade rubber or plastic, moves the powder gently from the hopper to the processing area. In pneumatic systems, compressed air is used to create a flow of air that carries the chocolate powder through a tube, ensuring a dust-free and efficient transfer. The control system allows operators to adjust the speed and direction of the conveyor, ensuring precise control over the powder flow and preventing overloading or blockages.
Applications and Benefits of Chocolate Powder Conveyors
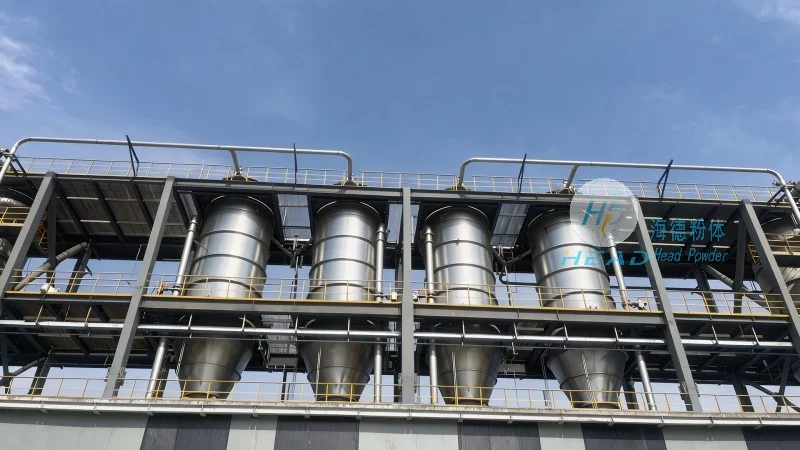
Chocolate powder conveyors are widely used in various stages of chocolate production, from raw material handling to final product packaging. They are essential in factories where chocolate powder is used to make confectionery items, such as truffles, cookies, and chocolate bars. The benefits of using these conveyors include improved efficiency in material handling, reduced labor costs, and enhanced product quality. By minimizing the risk of product contamination and degradation, chocolate powder conveyors help manufacturers maintain high standards of food safety and consistency. Additionally, the design of these systems allows for easy integration into existing production lines, making them a cost-effective solution for modern chocolate manufacturing facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of specialized powder handling equipment, including chocolate powder conveyors. With a focus on innovation and quality, HeadPowder has developed advanced conveyor systems that meet the demanding requirements of the chocolate industry. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest technology and skilled workforce. HeadPowder's commitment to customer satisfaction and product excellence has made it a trusted partner for chocolate manufacturers worldwide, providing reliable and efficient solutions for their powder handling needs.