

What is a Stone Aggregate Powder Conveying System Equipment? What Are Its Design Principles?
For industries dealing with stone aggregates and powder materials, efficient and reliable material handling systems are crucial. The stone aggregate powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd. based in China, represents a sophisticated solution designed to address the challenges of transporting bulk materials like stone aggregates and fine powders. This equipment is engineered to ensure smooth, continuous operation while maintaining high levels of material integrity and system efficiency.
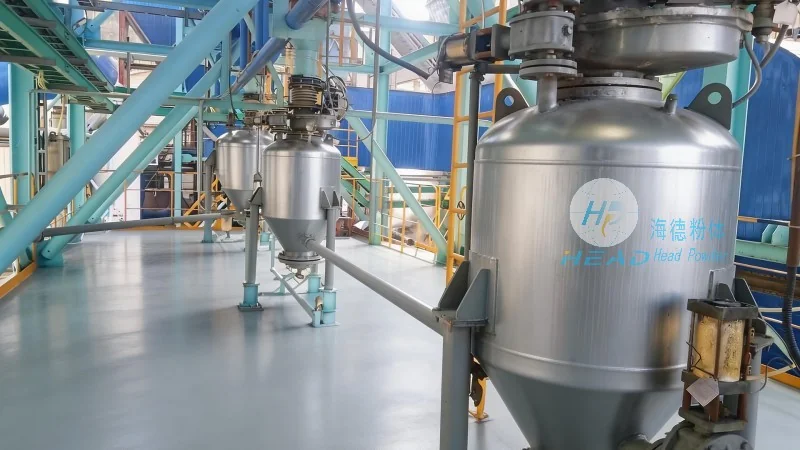
Understanding the Core Components of the Stone Aggregate Powder Conveying System
The stone aggregate powder conveying system typically consists of several key components that work in tandem to facilitate material transport. These components include a hopper for material storage, a feeding mechanism to control the flow of material into the system, a conveying unit (such as a screw conveyor, pneumatic conveyor, or belt conveyor) that moves the material through the system, and a discharge mechanism to release the material at the desired location. Each component is carefully designed to handle the specific characteristics of stone aggregates and powder materials, ensuring optimal performance and minimal downtime.
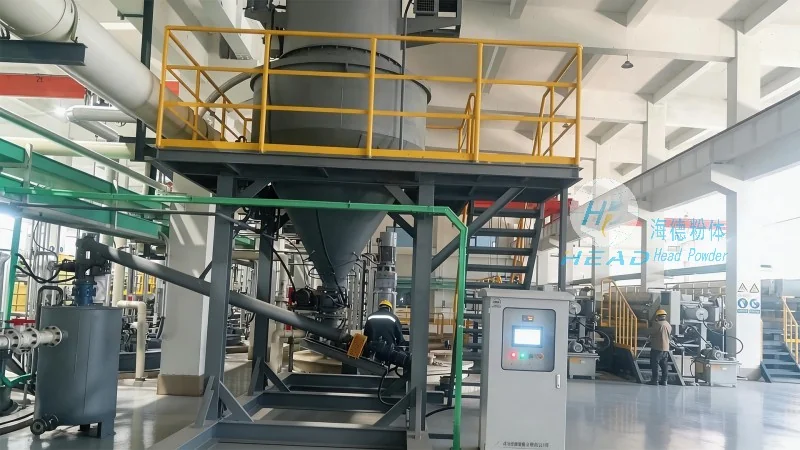
Design Principles Behind the Stone Aggregate Powder Conveying System
The design principles of the stone aggregate powder conveying system are centered on several critical factors. First, the system must be capable of handling a wide range of material types, from coarse stone aggregates to fine powders, without causing blockages or degradation of the material. This is achieved through the use of specialized materials for the conveying components and the incorporation of features like adjustable feeding rates and variable speed drives. Second, the system is designed for high efficiency and low energy consumption. By optimizing the conveying mechanism and reducing friction, the system minimizes power usage while maintaining high throughput rates. Third, safety and maintenance are integral to the design. The system incorporates safety features such as overload protection and emergency stop buttons, and its modular construction allows for easy maintenance and component replacement.
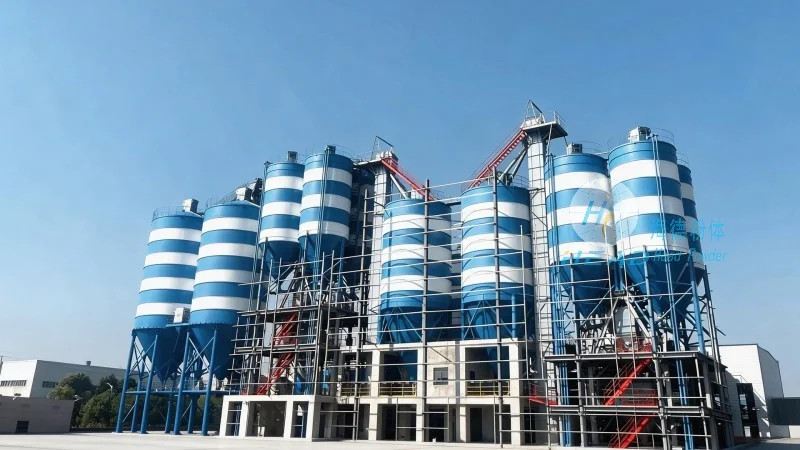
Key Features and Advantages of the Stone Aggregate Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into the stone aggregate powder conveying system to enhance its functionality and user experience. One of the key features is the ability to handle both dry and wet materials, making it versatile for various industrial applications. The system also offers adjustable conveying speeds, allowing operators to customize the flow rate based on the specific requirements of the process. Additionally, the equipment is designed for easy integration into existing production lines, with standard interfaces for control systems and material feeding mechanisms. The advantages of this system include improved material handling efficiency, reduced labor costs, and enhanced safety for operators. By automating the material transport process, the system minimizes the risk of human error and ensures consistent material quality throughout the production cycle.
Applications and Industries Benefiting from the Stone Aggregate Powder Conveying System
The stone aggregate powder conveying system is widely used in various industries that require the transport of bulk materials. In the construction industry, it is used to move stone aggregates and cement powders for concrete production. In the mining sector, it helps in transporting crushed ore and fine powders from processing plants to storage or further processing facilities. The system is also utilized in the chemical and pharmaceutical industries for transporting raw materials and finished products. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial plants. By providing a reliable and efficient means of material transport, the system contributes to increased productivity and reduced operational costs for these industries.
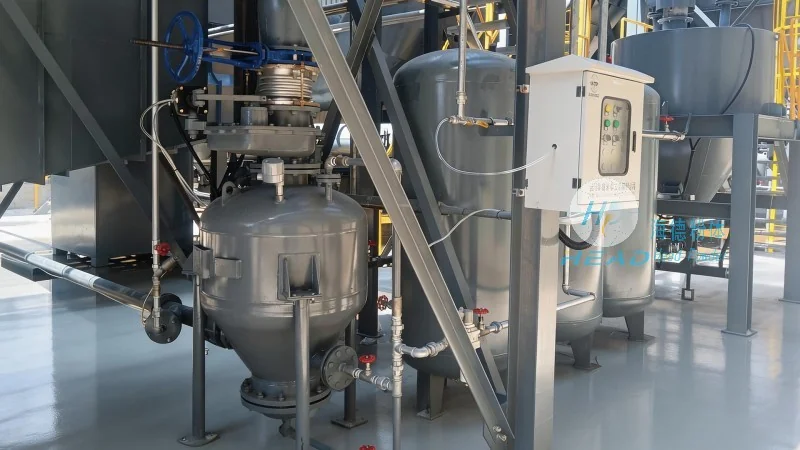
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in China, specializes in the design and manufacturing of advanced material handling equipment, including the stone aggregate powder conveying system. The company's commitment to innovation and quality has made its products a trusted choice for industries worldwide. The stone aggregate powder conveying system, with its robust design and efficient operation, offers a reliable solution for the transportation of stone aggregates and powder materials. By adhering to strict quality standards and providing comprehensive technical support, Shandong HeadPowder Engineering Co., Ltd. ensures that its customers receive the best possible service and support for their material handling needs.