

What is a Brown Sugar Powder Pneumatic Conveying Machine? What Are Its Design Principles?
When it comes to handling brown sugar in industrial settings, the brown sugar powder pneumatic conveying machine has emerged as a critical piece of equipment. This device is specifically engineered to transport brown sugar powder efficiently and reliably, ensuring that the process of moving this valuable ingredient is both effective and safe. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. from China has been at the forefront of developing advanced solutions for powder handling, with a strong focus on precision and performance.
Product Overview
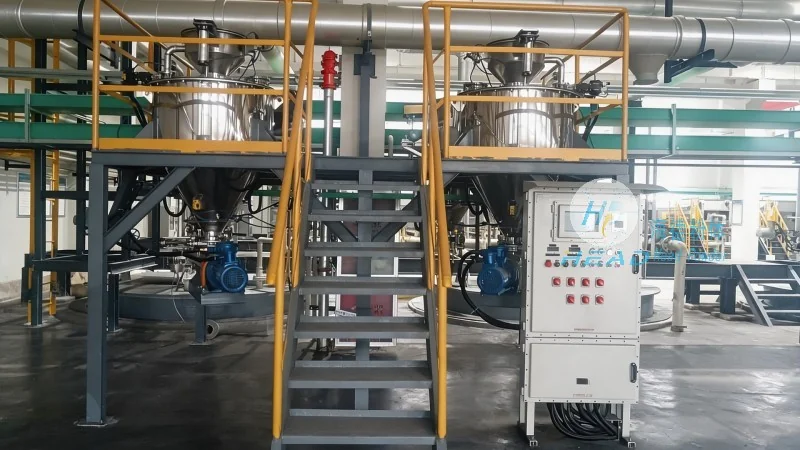
The brown sugar powder pneumatic conveying machine is a specialized system designed to transport brown sugar powder through a pressurized or vacuum system. Unlike traditional mechanical conveyors, this equipment utilizes air or gas to move the powder, offering advantages such as reduced contamination, minimal product degradation, and the ability to handle materials that are sensitive to moisture or temperature changes. The machine is particularly suited for applications where the brown sugar powder needs to be moved over long distances or through complex layouts without the need for multiple transfer points.
Design Principles
The design of the brown sugar powder pneumatic conveying machine is based on fundamental principles of fluid dynamics and material handling. The core components include a hopper for material storage, a conveyor line with appropriate ducting, and a control system that regulates the air flow. The system operates by creating a pressure differential, either by blowing air into the system (positive pressure) or by creating a vacuum (negative pressure). This differential causes the brown sugar powder to be carried along with the air stream, ensuring a consistent and controlled flow. The design also incorporates features such as cyclone separators and filters to separate the powder from the air, preventing dust accumulation and maintaining air quality. The machine is built with materials that are resistant to corrosion and wear, ensuring durability and long-term performance.
Technical Specifications
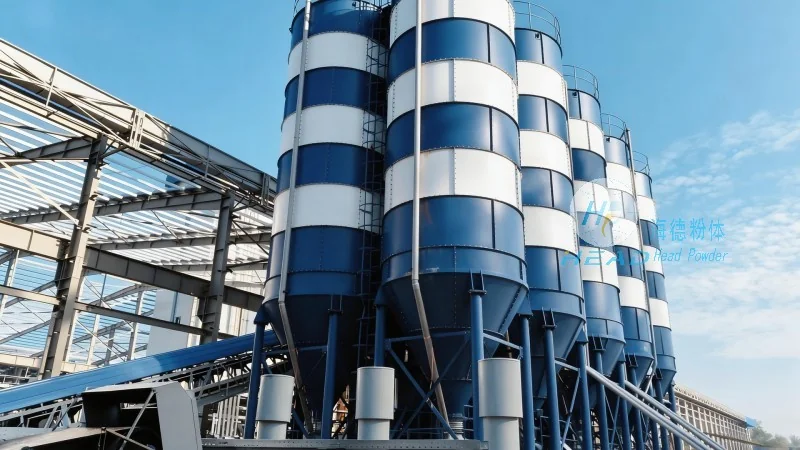
Shandong HeadPowder Engineering Co., Ltd. offers a range of brown sugar powder pneumatic conveying machines with varying capacities and configurations to meet different industrial needs. The machines are available in different sizes, from small-scale units for laboratory or pilot applications to large-scale systems for full production lines. Key technical specifications include the conveying capacity, which can range from a few kilograms per hour to several tons per hour, depending on the model. The system also features adjustable air flow rates, allowing for precise control over the speed of powder movement. The equipment is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents and ensure operator safety. The design incorporates easy maintenance components, such as quick-release fittings and accessible filter systems, to minimize downtime and maintenance costs.
Application Scenarios
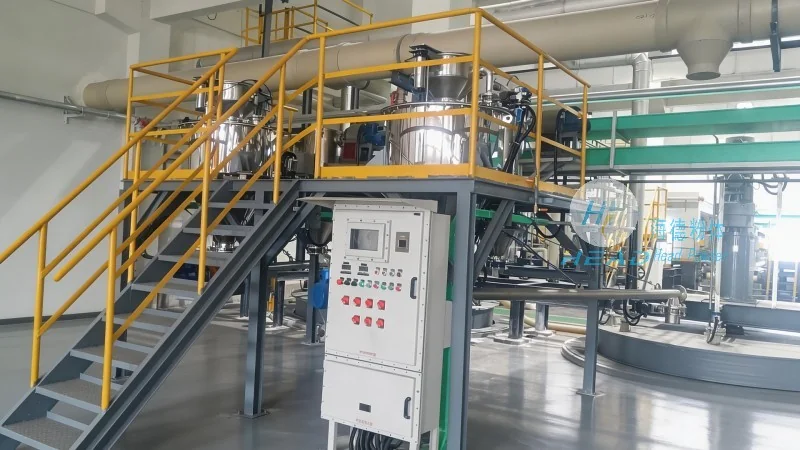
Brown sugar powder pneumatic conveying machines are widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, these machines are commonly employed in sugar refineries and confectionery factories to transport brown sugar powder from storage silos to processing lines. The equipment is also used in the pharmaceutical sector to handle brown sugar as an ingredient in formulations, ensuring that the powder is transferred without contamination or degradation. Additionally, in chemical plants, the machine can be used to transport brown sugar powder as a raw material for various chemical processes, where precise control over the material flow is essential.
Advantages of Using a Brown Sugar Powder Pneumatic Conveying Machine
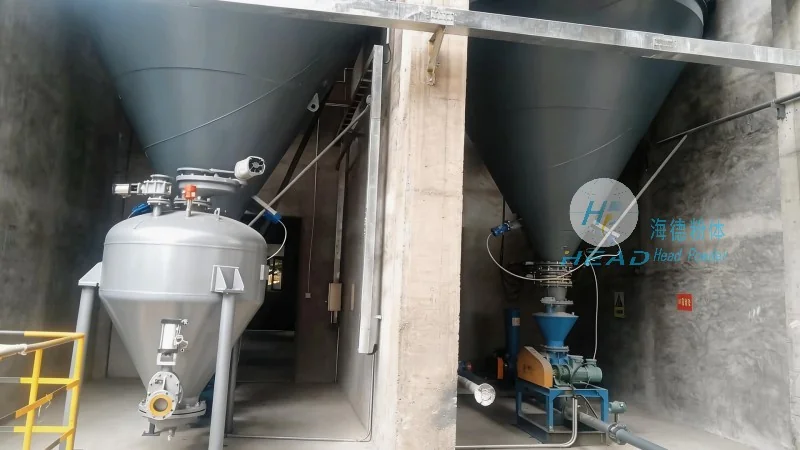
There are several advantages to using a brown sugar powder pneumatic conveying machine over traditional methods. One of the primary benefits is the reduction in product contamination, as the enclosed system prevents exposure to external elements. This is particularly important for brown sugar, which is a sensitive ingredient that can easily absorb moisture or odors. Another advantage is the ability to handle the powder over long distances without the need for multiple transfer points, which can reduce the overall cost and complexity of the system. The machine also offers improved safety, as there are no moving parts in direct contact with the powder, minimizing the risk of injury. Furthermore, the system is highly efficient, with minimal energy consumption compared to other conveying methods. The design also allows for easy integration with other processing equipment, making it a versatile solution for various industrial applications.
Conclusion
The brown sugar powder pneumatic conveying machine is an essential piece of equipment for any industrial operation that handles brown sugar powder. With its advanced design and reliable performance, this machine ensures that the transportation of brown sugar is done efficiently, safely, and with minimal risk of contamination. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. from China continues to innovate and provide high-quality solutions that meet the evolving needs of the industry. By investing in a brown sugar powder pneumatic conveying machine, businesses can enhance their operational efficiency, improve product quality, and ensure compliance with industry standards.