

Working Principle and Characteristics of Dye Pneumatic Conveying Equipment
When it comes to efficiently transporting dye powders in industrial settings, the choice of equipment plays a crucial role in maintaining product quality, operational efficiency, and overall process reliability. Pneumatic conveying systems have emerged as a preferred solution for handling dye materials due to their ability to minimize contamination risks, reduce material degradation, and enable seamless integration into production lines. This article delves into the working principle and key characteristics of dye pneumatic conveying equipment, providing insights into how these systems operate and the advantages they offer to manufacturers.
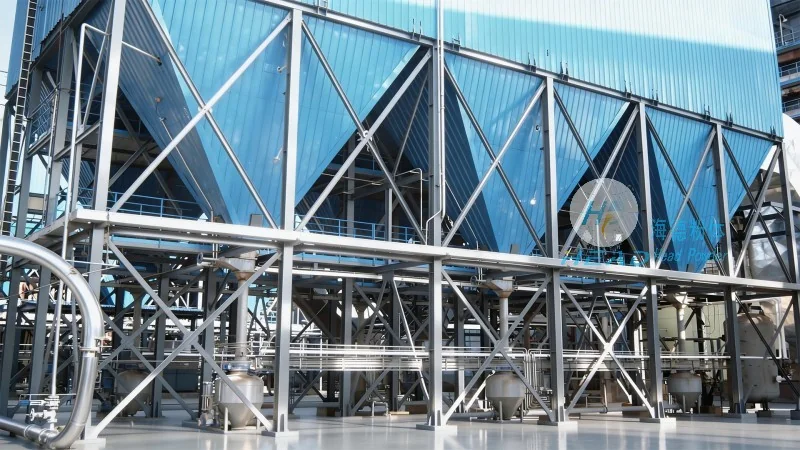
Understanding the Working Principle of Dye Pneumatic Conveying Equipment
The core of a dye pneumatic conveying system lies in its ability to transport solid particles, such as dye powders, using compressed air or other gases. The process typically involves several key components and steps that work in tandem to ensure effective material transfer. At its foundation, the system relies on the principle of creating a pressure differential between the conveying line and the ambient environment. This is achieved by using a blower or compressor to generate high-pressure air, which then propels the dye particles through the pipeline.
During operation, the dye powder is introduced into the conveying line either by gravity feed or through a hopper. The compressed air, introduced at a specific pressure and velocity, creates a flow that lifts and transports the particles. The design of the system, including the type of air nozzle, the size of the conveying line, and the velocity of the air, all contribute to the efficiency of the material transfer. The air flow can be categorized into two main types: dilute phase and dense phase, each offering different advantages depending on the specific requirements of the dye being transported.
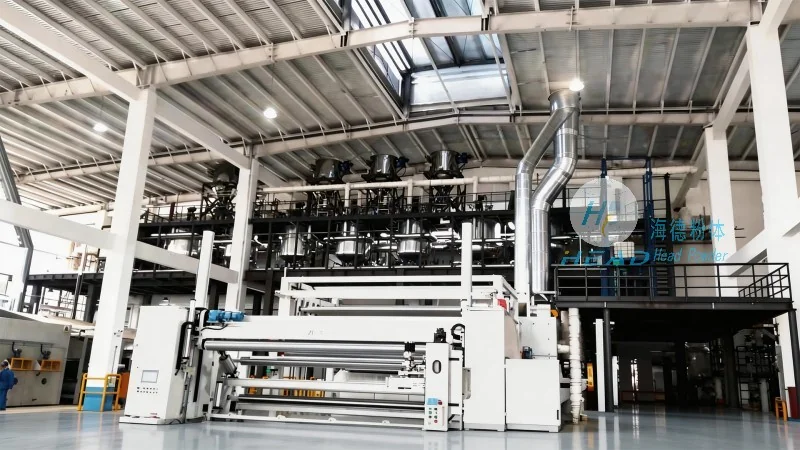
Key Characteristics of Dye Pneumatic Conveying Equipment
Several distinct characteristics define the performance and suitability of dye pneumatic conveying equipment for industrial applications. These features not only enhance operational efficiency but also contribute to the preservation of the dye's quality and consistency. The first notable characteristic is the ability to handle fine and abrasive dye powders without causing degradation or caking. Pneumatic systems are particularly effective in preventing particle agglomeration, which can occur in traditional mechanical conveying methods. This is achieved through the use of appropriate air velocities and pipeline designs that maintain the particles in a suspended state.
Another critical characteristic is the system's ability to minimize contamination risks. Unlike mechanical conveyors that may come into direct contact with the dye, pneumatic systems use enclosed pipelines, reducing the exposure of the material to external contaminants. This is especially important for dyes used in pharmaceutical or food industries, where product purity is paramount. The enclosed design also helps in maintaining the color integrity of the dye, preventing any color shift due to exposure to air or moisture.
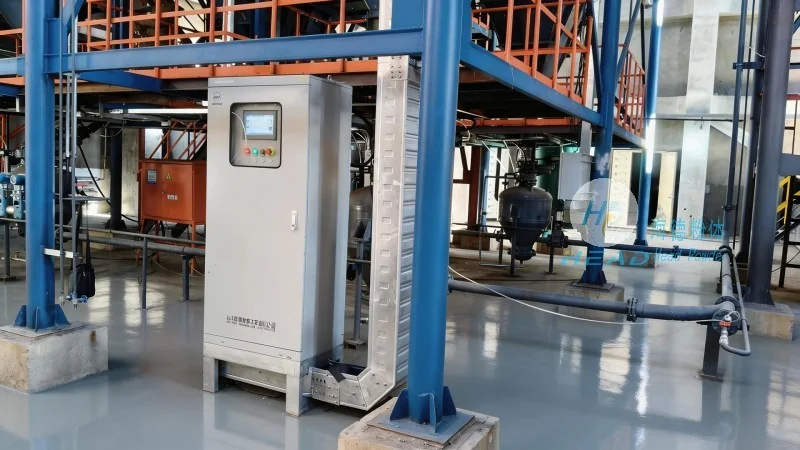
Operational flexibility is another key characteristic of dye pneumatic conveying equipment. These systems can be easily adapted to handle varying quantities of dye, from small batches to large-scale production runs. The ability to adjust air pressure and flow rates allows for precise control over the conveying speed, ensuring that the material is transported at the optimal rate without causing excessive wear on the equipment or degradation of the product. Additionally, the modular design of many pneumatic conveying systems enables easy integration with existing production lines, reducing downtime during installation and maintenance.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of pneumatic conveying equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized solutions tailored to the unique needs of dye manufacturers. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking reliable and efficient dye handling systems. HeadPowder's expertise lies in designing and manufacturing pneumatic conveying equipment that meets the stringent requirements of the dye industry, ensuring that each system is optimized for performance, durability, and cost-effectiveness.
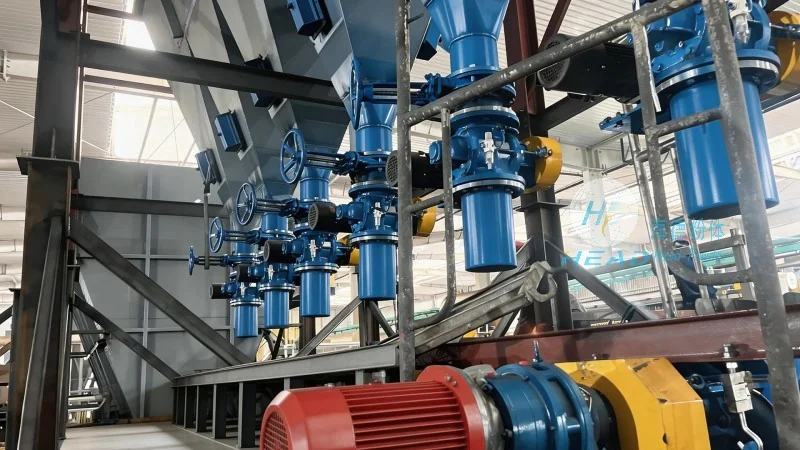
HeadPowder's product line includes a range of pneumatic conveying systems, from simple dilute phase units to complex dense phase systems, all engineered to handle various types of dye powders. The company's team of engineers and technicians works closely with clients to understand their specific operational challenges and develop solutions that enhance productivity while maintaining product quality. By leveraging advanced technology and rigorous quality control processes, HeadPowder ensures that each piece of equipment is built to withstand the demands of industrial environments, providing long-term reliability and minimal maintenance requirements.
HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility equipped with the latest production equipment and testing capabilities. This infrastructure enables the company to produce high-quality pneumatic conveying systems that comply with international standards and meet the diverse needs of global clients. The company's dedication to customer satisfaction and technical excellence has earned it a reputation as a leading supplier in the pneumatic conveying industry, with a focus on delivering solutions that drive operational efficiency and profitability for its clients.