

Working Principle and Features of Suction-Pressure Mixed Pneumatic Conveying Systems
For industrial applications requiring efficient material handling, the suction-pressure mixed pneumatic conveying system stands out as a versatile solution. This technology combines the advantages of both suction and pressure conveying methods, offering enhanced flexibility and performance in transporting various bulk materials. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to meet diverse industrial needs.
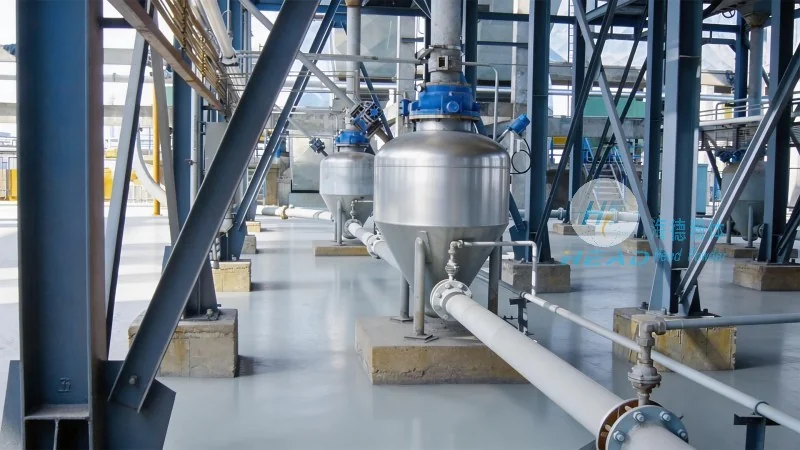
Understanding the Working Principle of Suction-Pressure Mixed Pneumatic Conveying Systems
The core of a suction-pressure mixed pneumatic conveying system lies in its dual-mode operation, which integrates both suction and pressure stages to optimize material transport. The system typically starts with a suction phase where air is drawn into the conveying line to pick up material from the source. This initial stage ensures that even fine or light materials are effectively captured and moved. Once the material is in the line, the system transitions to a pressure phase, where compressed air is introduced to push the material forward, ensuring continuous and reliable transport to the destination. This hybrid approach allows for the handling of a wide range of materials, from powders to granules, with minimal loss and high efficiency.
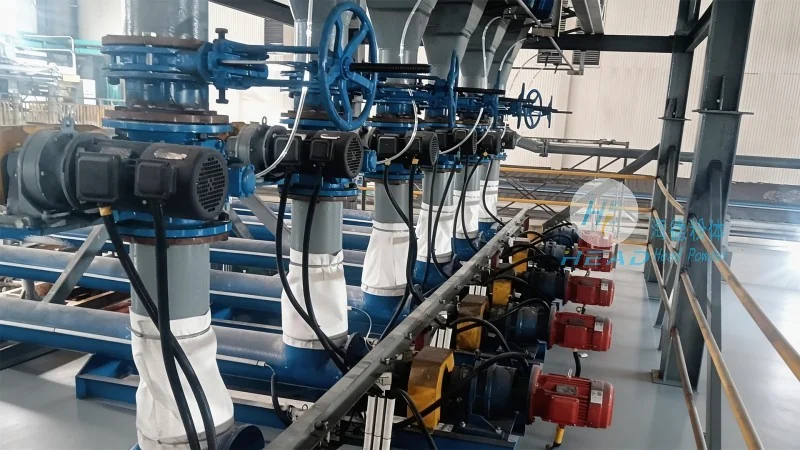
Key Features and Advantages of Suction-Pressure Mixed Pneumatic Conveying Systems
One of the primary features of this system is its ability to handle materials with varying properties. The suction mode is particularly effective for materials that are difficult to convey using traditional pressure systems alone, such as those with low bulk density or high moisture content. By combining suction and pressure, the system can maintain consistent flow rates and reduce the risk of material degradation or blockages. Another significant advantage is the reduced energy consumption compared to purely pressure-based systems. The hybrid operation allows for lower air pressure requirements, leading to energy savings and lower operational costs. Additionally, the system offers improved flexibility in layout design, as it can accommodate longer conveying distances and multiple transfer points without compromising performance. The modular design also facilitates easy maintenance and upgrades, ensuring long-term reliability and performance.
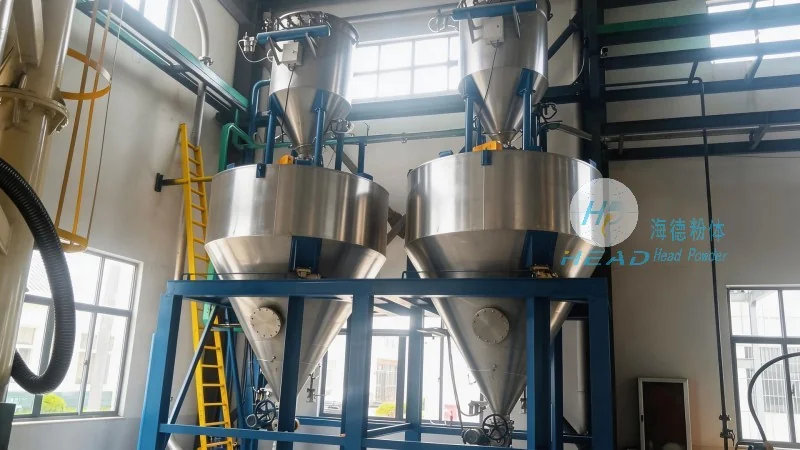
Applications and Industries Benefiting from Suction-Pressure Mixed Pneumatic Conveying Systems
The versatility of suction-pressure mixed pneumatic conveying systems makes them suitable for a wide array of industries. In the pharmaceutical sector, these systems are used for the transport of sensitive powders, ensuring contamination-free handling and maintaining product integrity. In the food industry, they are employed for conveying ingredients like flour, sugar, and spices, where hygiene and product quality are paramount. The chemical industry also benefits from this technology for handling various powders and granules, including those that are corrosive or reactive. Furthermore, in the mining and minerals sector, the system is utilized for transporting raw materials from storage to processing units, enhancing operational efficiency and safety. The ability to handle diverse materials and adapt to different operational conditions makes it an indispensable tool in modern industrial material handling.
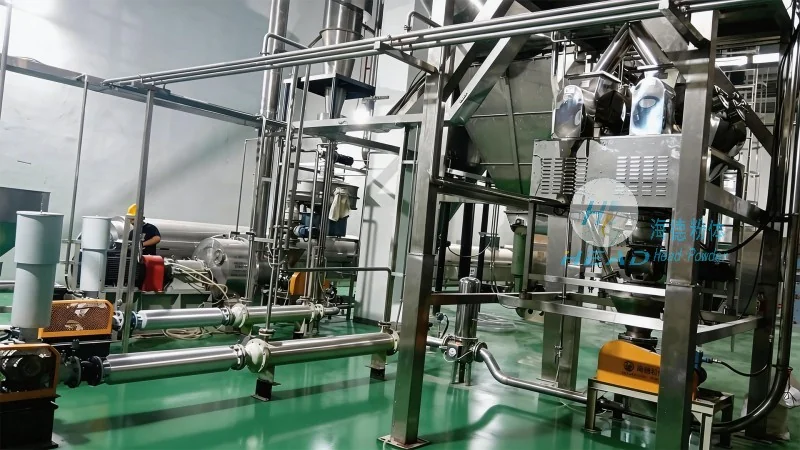
Customization and Technical Support from Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial application has unique requirements. Therefore, they offer customized solutions tailored to specific needs, ensuring optimal performance and efficiency. The company provides comprehensive technical support, from initial system design and installation to ongoing maintenance and troubleshooting. Their team of experts works closely with clients to understand their material handling challenges and develop solutions that address them effectively. With a focus on quality and innovation, HeadPowder ensures that their suction-pressure mixed pneumatic conveying systems are built to withstand the demands of industrial environments, providing reliable and long-lasting performance. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner in the material handling industry.