

Working Principle and Features of Sorghum Distillers' Grain Pneumatic Conveying Line
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the processing of sorghum distillers' grain. This article delves into the operational mechanics and key attributes of such systems, providing a comprehensive overview for industry professionals seeking efficient material handling solutions.
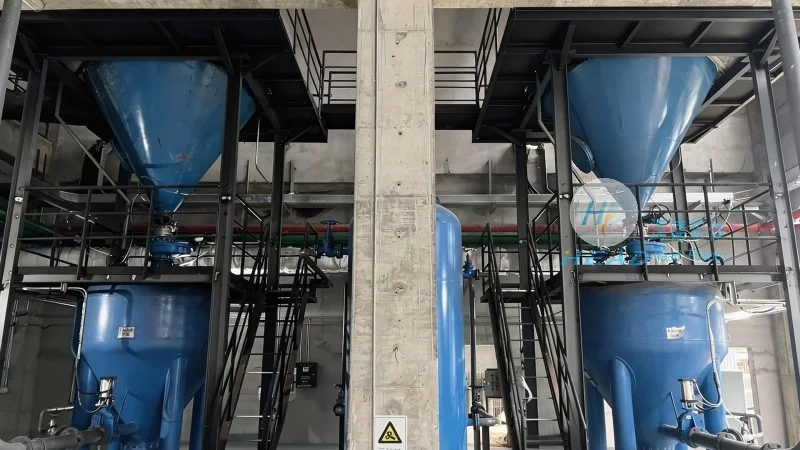
Understanding the Working Principle of Sorghum Distillers' Grain Pneumatic Conveying Lines
The core function of a sorghum distillers' grain pneumatic conveying line is to transport bulk materials, specifically the solid residues from the distillation process, from one location to another within a facility. The system operates by utilizing compressed air or gas to create a flow that propels the material through a pipeline network. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and operational downtime. The process typically involves a series of steps: material feeding, air injection, and transport through the pipeline, with the air serving as the primary medium for movement. The system is designed to handle the specific characteristics of sorghum distillers' grain, such as its moisture content and particle size, ensuring efficient and reliable transport without degradation of the material.
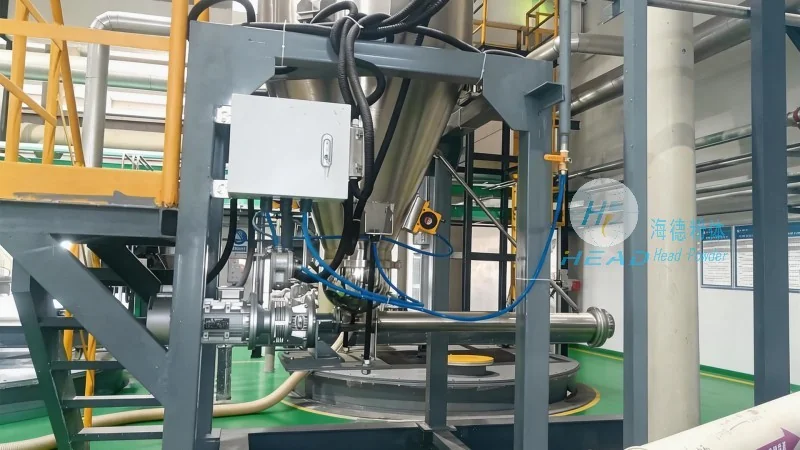
Key Features of Sorghum Distillers' Grain Pneumatic Conveying Systems
Several distinct features set these pneumatic conveying systems apart from traditional material handling methods. Firstly, the system offers high flexibility in terms of layout and integration with existing plant infrastructure. This adaptability allows for customized solutions that fit the unique spatial constraints and operational needs of a distillery. Secondly, the technology provides excellent dust control, which is crucial for maintaining a safe and clean working environment in food and beverage processing facilities. The enclosed pipeline design minimizes the release of airborne particles, enhancing both worker safety and compliance with environmental regulations. Additionally, the system's ability to handle varying material flow rates makes it suitable for both continuous and intermittent production cycles, ensuring consistent performance regardless of production demands. Another notable feature is the reduced risk of material contamination, as the enclosed system prevents cross-contamination with other substances or environmental elements. This is particularly important for products intended for human consumption or animal feed. Furthermore, the energy efficiency of pneumatic conveying systems contributes to lower operational costs over time, making them a cost-effective choice for long-term use.
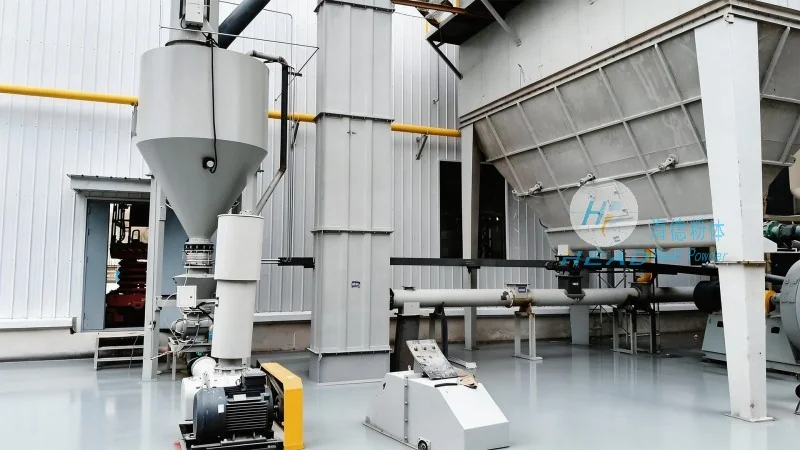
Operational Advantages and Practical Applications
Implementing a sorghum distillers' grain pneumatic conveying line offers numerous operational advantages. The primary benefit is the significant reduction in labor costs associated with manual handling of bulk materials. By automating the transport process, the system minimizes the need for manual labor, thereby improving overall productivity and reducing the risk of workplace injuries. The system also enhances process control, allowing for precise regulation of material flow rates and pressure levels, which is critical for maintaining consistent product quality. In practical applications, these systems are commonly used in the post-distillation phase of sorghum processing, where the distillers' grain is transported from the stillage tanks to storage silos or further processing units. The efficiency of the system ensures that the material is moved quickly and reliably, preventing spoilage or degradation that could occur with slower, manual handling methods. Moreover, the system's scalability allows for expansion as production volumes increase, providing a long-term solution that grows with the business.
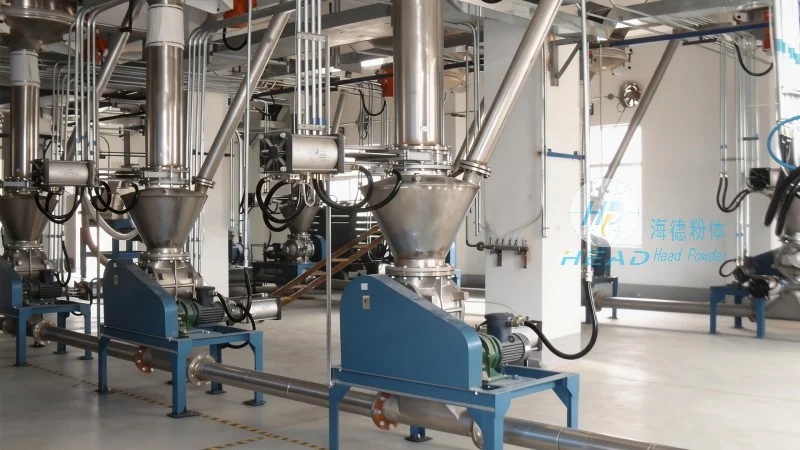
Conclusion and Company Expertise
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a trusted partner in the design and installation of pneumatic conveying systems for the sorghum distillers' grain industry. The company's expertise lies in tailoring solutions that meet the specific requirements of each client, ensuring optimal performance and reliability. By leveraging advanced engineering principles and years of industry experience, HeadPowder delivers systems that not only enhance operational efficiency but also contribute to a safer and more sustainable working environment. For businesses seeking to improve their material handling processes, the sorghum distillers' grain pneumatic conveying line represents a cutting-edge solution that combines technology, efficiency, and safety.