

Working Principle and Features of Mobile Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of advanced powder handling equipment. Among their product portfolio, the mobile powder conveying system stands out as a versatile solution for efficient material transport in various industrial applications. This article delves into the working principle and key features of such systems, highlighting how they enhance operational efficiency and flexibility for businesses dealing with bulk powders.
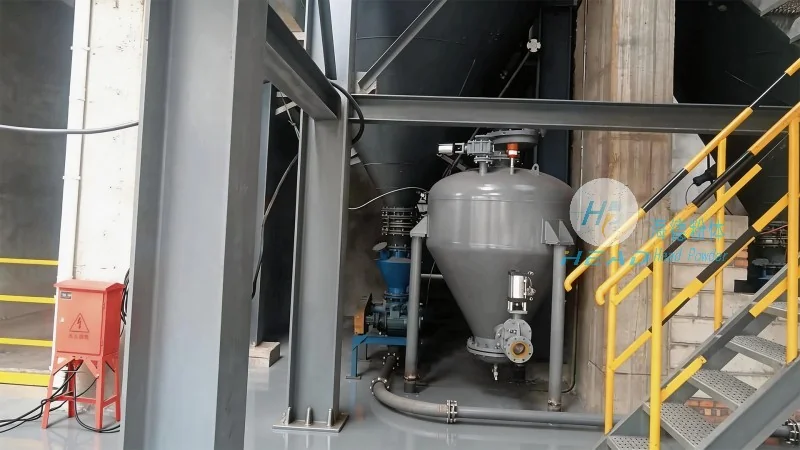
Understanding the Working Principle of Mobile Powder Conveying Systems
The mobile powder conveying system operates on the principle of pneumatic transport, utilizing compressed air or vacuum to move bulk powders from a source to a destination. The system typically comprises several core components, including a powerful air compressor or vacuum pump, a hopper for material storage, a conveying pipe network, and a control panel for system management. When activated, the system draws powder from the hopper and propels it through the pipes using air pressure or suction, depending on the configuration. This process ensures that powders are transported with minimal dust generation and high efficiency, making it suitable for a wide range of materials, from fine powders to bulk solids.
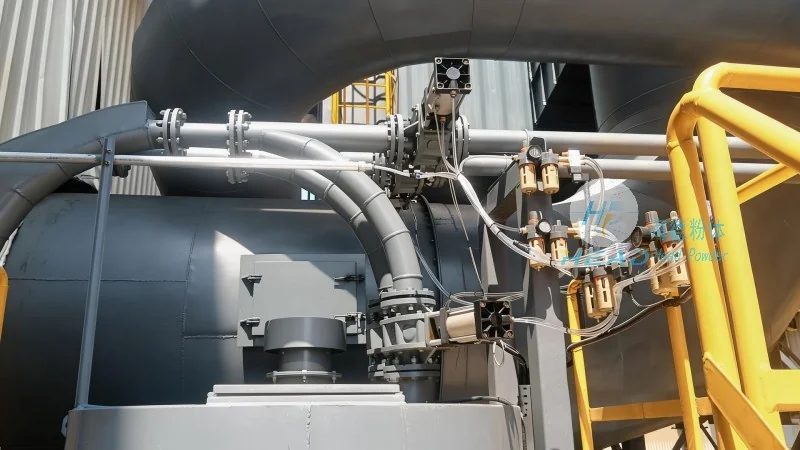
Key Features of Mobile Powder Conveying Systems
One of the most notable features of the mobile powder conveying system is its portability. Unlike fixed systems, these units are designed to be easily moved and repositioned as needed, allowing for flexible operation in different work areas. This mobility is particularly advantageous in industries where production lines or storage locations may change frequently, such as construction sites, mining operations, or on-site mixing facilities. Additionally, the system is equipped with adjustable speed controls and pressure settings, enabling operators to customize the conveying rate based on the specific characteristics of the powder being handled—whether it is lightweight, abrasive, or sensitive to moisture.
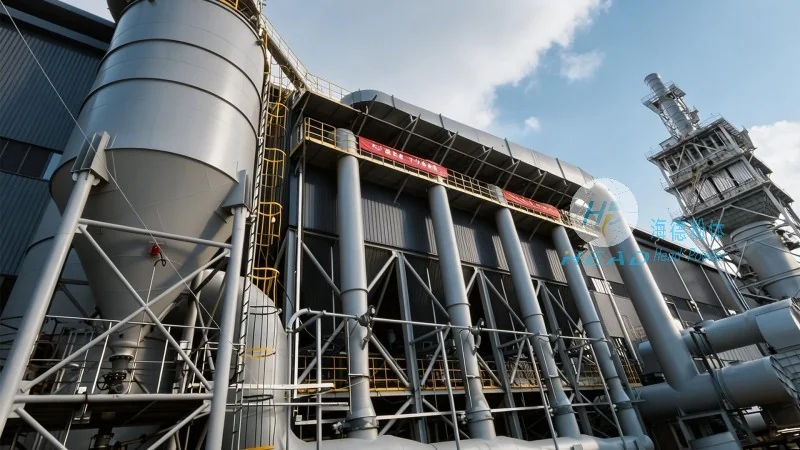
Another critical feature is the system's ability to handle diverse powder types with consistent performance. Shandong HeadPowder Engineering Co., Ltd. has engineered these systems to accommodate various particle sizes, densities, and flow properties, ensuring reliable transport without clogging or degradation of the material. The robust construction, often made from corrosion-resistant materials like stainless steel, further enhances durability and longevity, reducing maintenance costs over time. Furthermore, the mobile design incorporates safety features, such as automatic shut-off mechanisms and dust containment systems, to comply with industrial safety standards and protect both personnel and the environment.
Applications and Benefits in Industrial Settings
The mobile powder conveying system finds extensive application in sectors where bulk powder handling is essential, including pharmaceuticals, food processing, chemical manufacturing, and construction. In pharmaceutical production, for instance, the system ensures hygienic and contamination-free transport of raw materials, meeting stringent regulatory requirements. In the food industry, it maintains product purity and prevents cross-contamination, which is crucial for maintaining quality standards. For construction projects, the system facilitates the efficient delivery of cement, sand, and other dry mixtures to job sites, improving workflow and reducing labor costs. The benefits of using such a system extend beyond mere efficiency; it also contributes to improved workplace safety by minimizing manual handling of powders and reducing dust exposure.
Conclusion and Company Overview
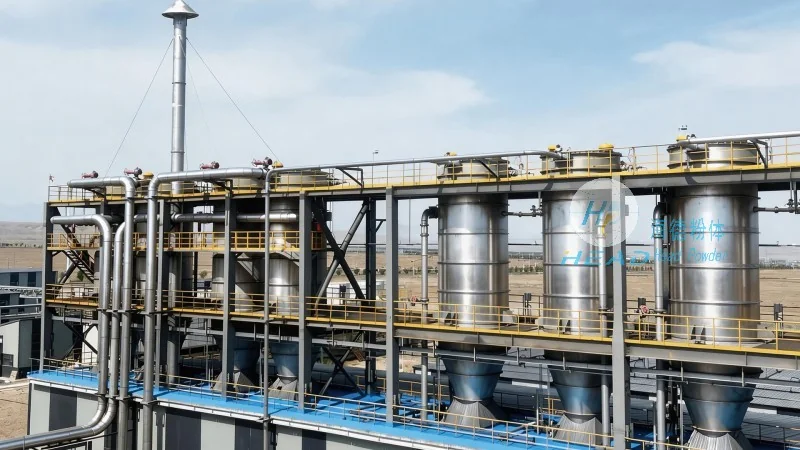
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in the field of powder handling technology, offering mobile powder conveying systems that combine advanced engineering with practical design. By understanding the working principle and leveraging the key features of these systems, businesses can enhance their operational capabilities, reduce downtime, and achieve greater productivity in their powder handling processes. With a strong commitment to quality and customer satisfaction, HeadPowder remains a trusted partner for industries seeking reliable and efficient solutions for their material transport needs.