

Working Principle and Features of Coal Ash Powder Conveyors
Coal ash powder conveyors represent a critical component in the industrial landscape, particularly for facilities that generate or utilize coal ash as a byproduct of coal combustion. These systems are engineered to efficiently transport fine particulate materials, ensuring safe, reliable, and cost-effective handling of coal ash. Understanding the underlying working principles and distinctive features of such conveyors is essential for selecting the most suitable equipment for specific operational needs. The headpowder company, Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in the design, manufacturing, and supply of these advanced conveyor systems, catering to the diverse requirements of industrial clients.
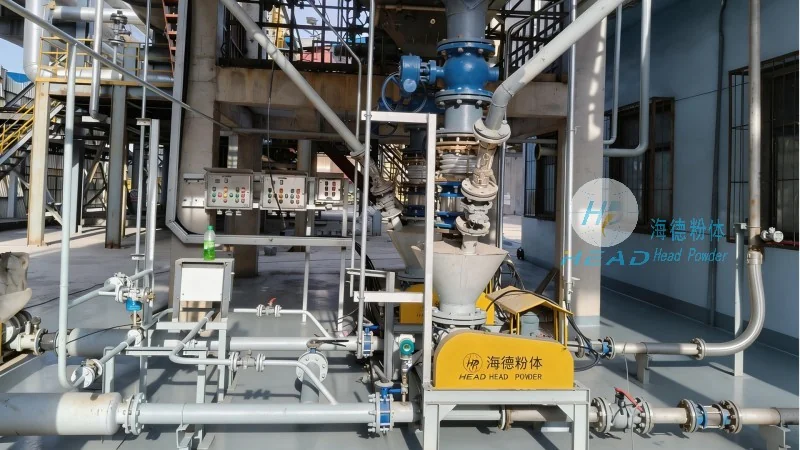
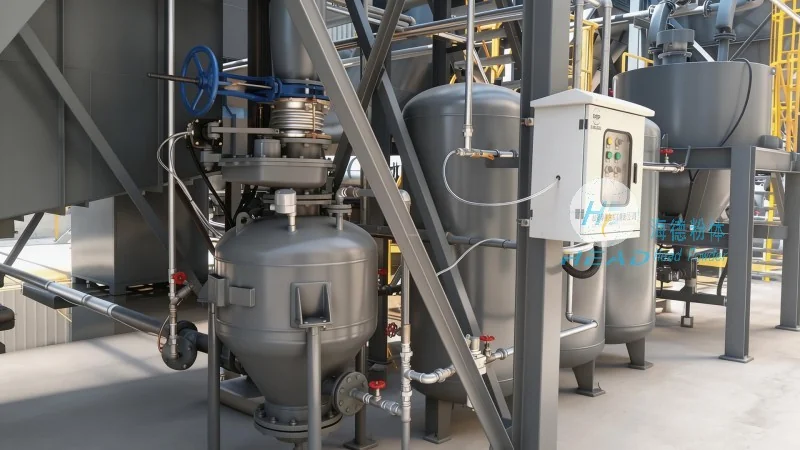
Working Principle of Coal Ash Powder Conveyors
The fundamental working principle of coal ash powder conveyors revolves around the use of air or mechanical forces to move fine particulate materials through a pipeline. The process typically begins with the feeding of coal ash into the conveyor system. A key initial component is the feeder or airlock, which regulates the flow of material into the conveying line, preventing overfeeding and ensuring consistent input. From there, the material is propelled through the pipeline using either positive pressure (air or gas) or negative pressure (suction). Positive pressure systems utilize compressed air to push the material forward, while negative pressure systems use suction to draw the material through the line. The choice between these methods depends on factors such as the material's properties (e.g., particle size, moisture content), the distance to be conveyed, and the required flow rate. The system is designed to maintain a consistent flow, minimizing clogging and ensuring reliable operation. The headpowder team leverages advanced engineering to optimize the conveyor design, ensuring that the system operates efficiently under various conditions. For instance, the company's expertise in material handling allows for the customization of conveyor components to suit specific coal ash characteristics, enhancing overall performance.
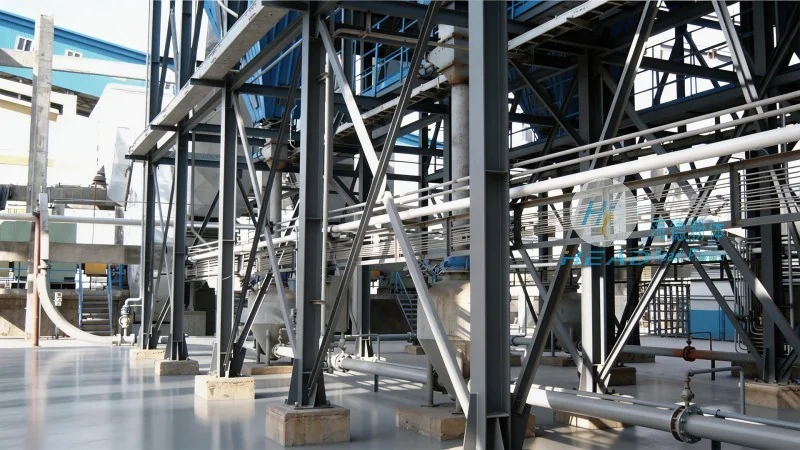
Key Features of Coal Ash Powder Conveyors
Coal ash powder conveyors from headpowder are distinguished by several key features that enhance their performance, durability, and operational efficiency. One of the primary features is their robust construction, utilizing high-quality materials such as stainless steel or corrosion-resistant alloys to withstand the abrasive nature of coal ash particles. This design minimizes wear and tear, extending the equipment's service life and reducing long-term maintenance costs. Another critical feature is the system's ability to maintain a consistent flow rate, which is vital for downstream processes like storage or processing. Advanced control systems are integrated into the conveyor, allowing for real-time monitoring and adjustment of the flow, ensuring optimal performance. Additionally, the conveyors are equipped with safety features, including pressure relief valves and emergency shut-off mechanisms, to prevent accidents and protect personnel from potential hazards. The company's commitment to quality control ensures that each conveyor meets stringent industry standards, providing reliable and safe operation. Furthermore, the design incorporates flexibility, enabling easy integration with existing industrial infrastructure and the ability to adapt to changing operational requirements.
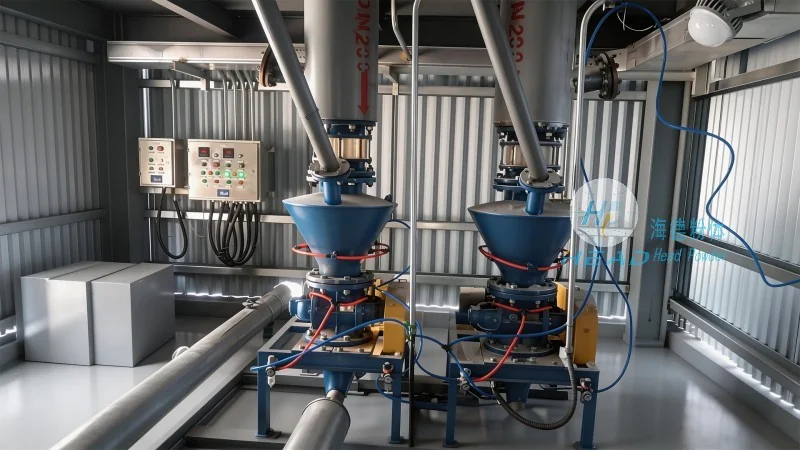
Applications and Benefits in Industrial Settings
Coal ash powder conveyors find extensive applications in power plants, cement manufacturing facilities, and other industrial sites where coal ash needs to be transported from one location to another. The primary benefit of using these conveyors is the significant reduction in labor costs associated with manual handling of coal ash, which improves workplace safety and reduces the risk of accidents. The equipment also minimizes material loss and contamination, ensuring that the coal ash is delivered to its destination in a clean and efficient manner, which is crucial for downstream processing. Furthermore, the conveyors can be integrated with storage silos or processing units to create a seamless material handling system, enhancing overall operational efficiency. The headpowder company's expertise in customizing conveyor systems allows clients to tailor the equipment to their specific needs, ensuring maximum efficiency and cost-effectiveness. For example, in a power plant, the conveyor can be integrated with the ash handling system to transport ash from the boiler to the storage area, streamlining the process and reducing downtime. The company's focus on customer satisfaction and technical support ensures that clients receive comprehensive solutions that meet their operational goals. The use of coal ash powder conveyors not only improves operational efficiency but also contributes to environmental sustainability by facilitating the proper disposal or utilization of coal ash, aligning with industrial best practices.