

Working Principle and Features of Molybdenum Oxide Material Handling Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems tailored for molybdenum oxide applications. The company's expertise lies in creating efficient, reliable, and safe systems that meet the stringent requirements of the molybdenum oxide industry. This article explores the working principle and key features of their molybdenum oxide material handling systems, providing insights into how these systems operate and the advantages they offer to users.
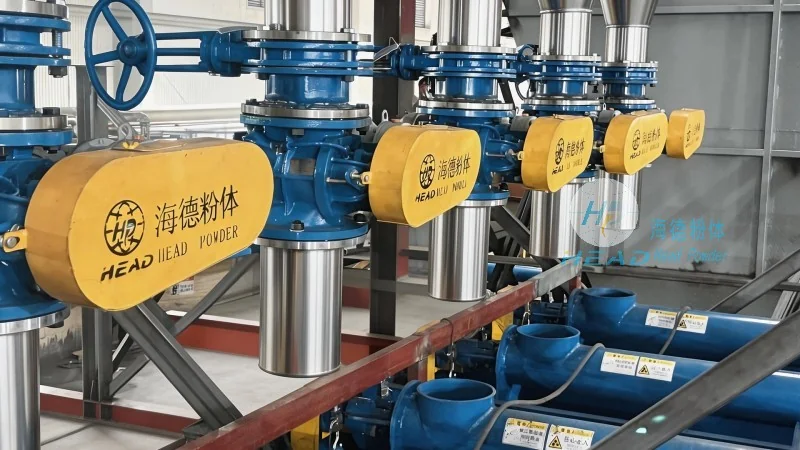
Overview of Molybdenum Oxide Material Handling Systems
Molybdenum oxide material handling systems are engineered to transport, store, and manage molybdenum oxide powders and related materials efficiently. These systems are typically composed of several interconnected components, including feeders, conveyors, storage silos, and control systems. The design of each component is optimized to handle the unique properties of molybdenum oxide, such as its fine particle size, reactivity, and potential for dust generation. By integrating these components into a cohesive system, HeadPowder ensures seamless material flow from raw material input to final product discharge.
Working Principle of the Material Handling System
The operation of a molybdenum oxide material handling system begins with the feeding of raw molybdenum oxide into the system. A feeder, often a rotary or vibratory type, regulates the flow rate of the material into the conveyor. The conveyor then transports the material to the storage silo or processing unit. In some systems, additional processing steps, such as blending or drying, may be integrated to enhance the material's quality. The control system monitors key parameters, including flow rate, pressure, and temperature, ensuring that the system operates within safe and optimal conditions. This closed-loop control mechanism allows for precise management of the material handling process, minimizing waste and maximizing productivity.
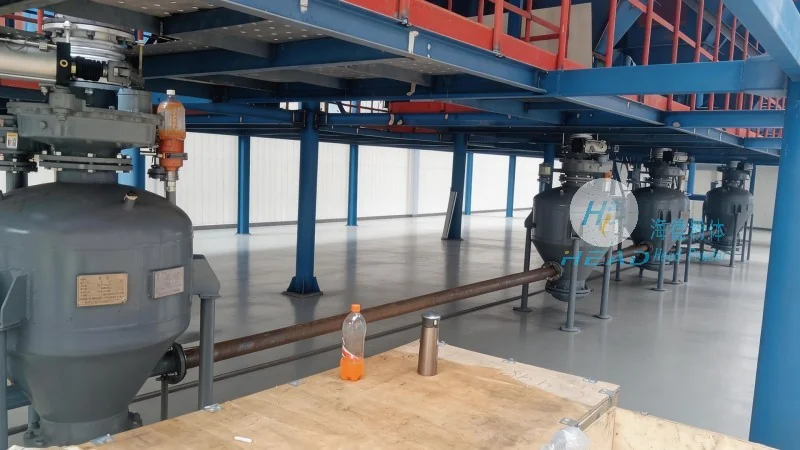
Key Features of the Molybdenum Oxide Material Handling System
HeadPowder's molybdenum oxide material handling systems are distinguished by several key features that enhance performance and reliability. Firstly, the systems are designed with dust suppression measures to mitigate the health and safety risks associated with handling fine powders. This includes enclosed conveyor systems, dust collection units, and proper ventilation to maintain a safe working environment. Secondly, the equipment is constructed from materials resistant to corrosion and wear, ensuring long-term durability and minimal maintenance. Thirdly, the systems incorporate advanced automation and control technologies, allowing for real-time monitoring and adjustment of operational parameters. This automation not only improves efficiency but also reduces the need for manual intervention, lowering the risk of human error. Additionally, the systems are scalable, enabling customization to meet the specific needs of different production scales and applications. Whether for small-scale laboratory use or large-scale industrial production, HeadPowder's systems can be tailored to fit the requirements of the user.
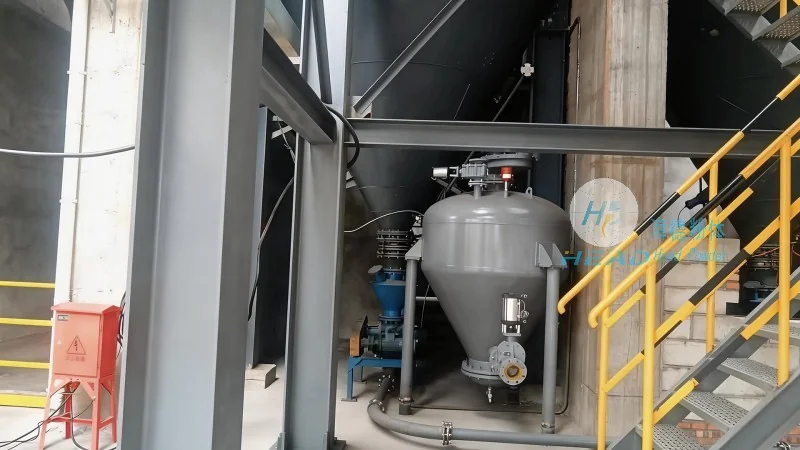
Benefits of Using Molybdenum Oxide Material Handling Systems
The implementation of a molybdenum oxide material handling system offers numerous benefits to industrial operations. By streamlining the material flow process, these systems reduce downtime and increase overall productivity. The precise control over material handling minimizes material loss and waste, leading to cost savings. Furthermore, the safety features integrated into the system protect workers from exposure to harmful dust and other hazards, improving workplace safety. The durability of the equipment ensures long-term reliability, reducing the frequency of maintenance and replacement costs. For companies operating in the molybdenum oxide industry, investing in a high-quality material handling system from HeadPowder can lead to improved operational efficiency, enhanced safety, and greater cost-effectiveness.
Conclusion
In conclusion, the working principle and features of molybdenum oxide material handling systems developed by HeadPowder demonstrate a high level of engineering sophistication and practical application. By combining advanced technology with robust design, these systems effectively address the challenges of handling molybdenum oxide materials. The systems' ability to ensure safe, efficient, and reliable material flow makes them an essential component for any molybdenum oxide processing facility. HeadPowder's commitment to quality and innovation ensures that their material handling systems continue to meet the evolving needs of the industry, providing users with a reliable solution for their material handling requirements.