

[Powdered Drug Particulate Pneumatic Conveying: An Efficient and Environmentally Friendly Material Handling Solution]
Pharmaceutical manufacturing relies on precise and reliable material handling systems to ensure product quality and compliance with stringent industry standards. Among the various methods available, pneumatic conveying stands out as a superior solution for transporting powdered drug materials. This technology offers significant advantages in terms of efficiency, environmental impact, and operational safety, making it an ideal choice for modern pharmaceutical facilities.
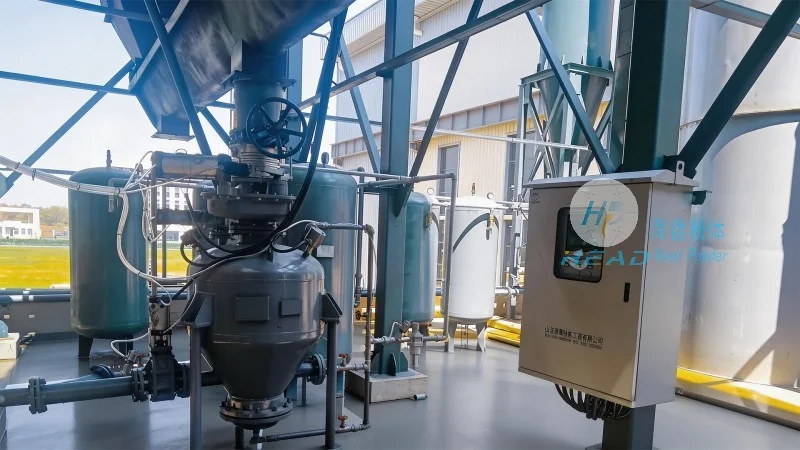
Introduction to Pneumatic Conveying for Pharmaceutical Powders
Pneumatic conveying systems utilize air or gas to transport bulk materials, such as pharmaceutical powders, through a network of pipes. Unlike traditional mechanical systems, this method eliminates the need for moving parts in the conveying line, reducing maintenance requirements and minimizing the risk of contamination. The process involves creating a pressure differential to move the powder, which can be either positive or negative pressure, depending on the specific application and material characteristics. This flexibility allows for tailored solutions that meet the unique needs of each pharmaceutical production line.
HeadPowder: A Leader in Pharmaceutical Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent provider of advanced material handling solutions tailored for the pharmaceutical industry. With a strong presence in China, specifically in Shandong province, the company specializes in designing, manufacturing, and implementing pneumatic conveying systems that enhance operational efficiency while adhering to the highest standards of quality and safety. HeadPowder's expertise lies in understanding the critical requirements of pharmaceutical manufacturing, including GMP compliance, product purity, and environmental sustainability.
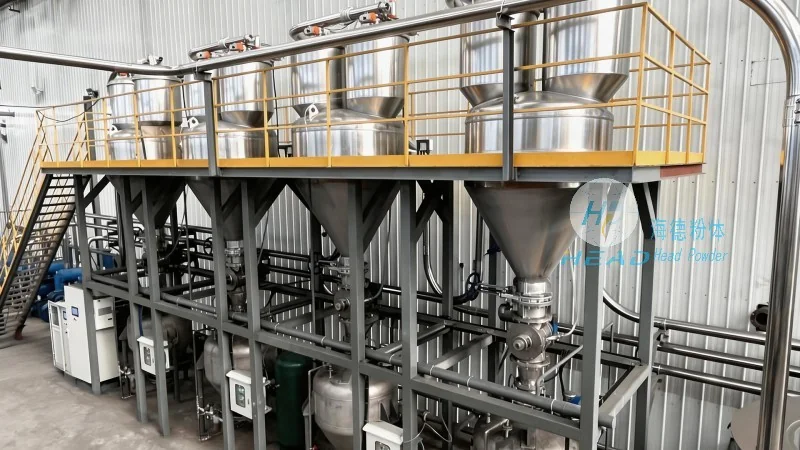
Efficiency and Environmental Benefits of Pneumatic Conveying Systems
One of the primary advantages of pneumatic conveying for pharmaceutical powders is its ability to streamline material transport processes. By eliminating the need for manual handling or complex mechanical equipment, these systems reduce labor costs and minimize the risk of human error. Additionally, the enclosed nature of the conveying system prevents dust dispersion, which is crucial for maintaining a clean and safe working environment. This not only improves workplace safety but also aligns with environmental regulations by reducing air pollution and dust emissions. The energy efficiency of pneumatic conveying systems further contributes to lower operational costs and a smaller carbon footprint, making it a sustainable choice for pharmaceutical manufacturers.
Key Features of Our Pneumatic Conveying Solutions
HeadPowder's pneumatic conveying solutions are engineered with precision to address the specific challenges of pharmaceutical powder handling. These systems are designed to maintain the integrity and purity of the drug particles throughout the conveying process. Key features include: high-precision control systems that ensure consistent flow rates and pressure levels, hygienic and GMP-compliant construction materials such as stainless steel and food-grade plastics, and flexible configuration options that can be adapted to various production scales and layouts. The company also offers advanced monitoring and automation capabilities, allowing for real-time tracking of material movement and system performance. These features collectively contribute to improved product quality, reduced downtime, and enhanced overall operational efficiency.
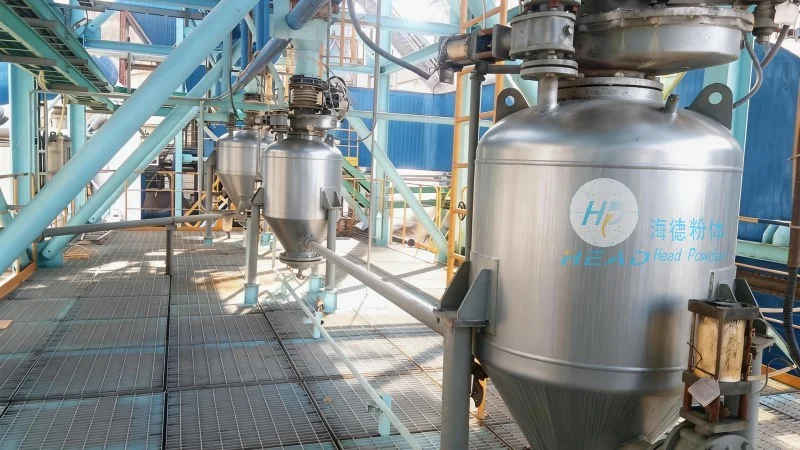
Application in Pharmaceutical Manufacturing
Pneumatic conveying systems are widely used in various stages of pharmaceutical manufacturing, from raw material storage and transfer to processing and packaging. For instance, in the initial stages, powders can be transferred from bulk storage silos to processing units without exposing them to external contaminants. During the manufacturing process, these systems facilitate the movement of active pharmaceutical ingredients (APIs) and excipients between different equipment, ensuring a seamless workflow. The enclosed design of the conveying lines also helps in maintaining the sterile environment required for sterile drug products, such as injectables and inhalers. By integrating pneumatic conveying into the production line, pharmaceutical companies can achieve higher throughput, reduce material waste, and improve overall production efficiency.
Conclusion
In conclusion, pneumatic conveying represents a cutting-edge solution for the efficient and environmentally friendly handling of pharmaceutical powders. With its ability to enhance operational efficiency, maintain product quality, and minimize environmental impact, this technology is increasingly becoming a standard in modern pharmaceutical manufacturing. HeadPowder, as a leading provider in this field, continues to innovate and deliver tailored pneumatic conveying systems that meet the evolving needs of the pharmaceutical industry. By leveraging advanced engineering and a deep understanding of industry requirements, HeadPowder ensures that its solutions not only improve productivity but also contribute to the sustainability and compliance of pharmaceutical operations.