

Airborne Conveying of Rare Earth Ore Powders: An Efficient and Environmentally Friendly Material Handling Solution
Efficient and environmentally friendly material handling is a critical requirement in the processing of rare earth ore powders. Traditional methods often face challenges such as dust pollution, material loss, and operational inefficiencies. To address these issues, advanced air conveying systems have emerged as a leading solution, offering a sustainable approach to transporting these valuable materials.
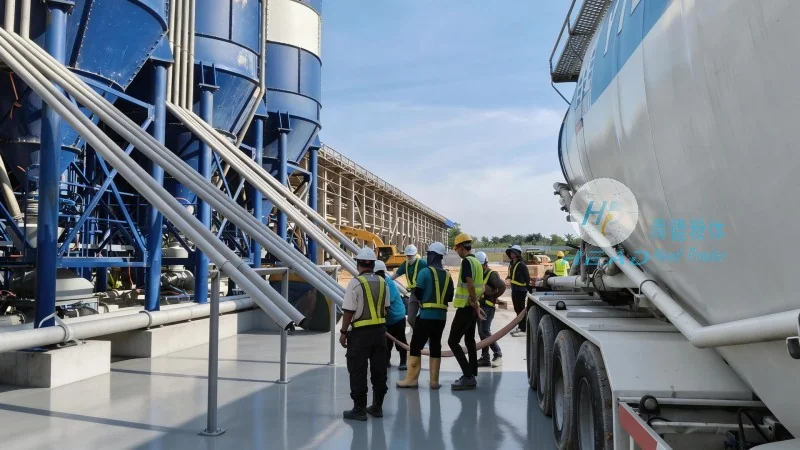
Advanced Air Conveying Technology for Rare Earth Ore Powders
HeadPowder Engineering, a leading provider in the field, specializes in developing and implementing air conveying solutions tailored to the unique characteristics of rare earth ore powders. The company's expertise lies in designing systems that ensure high efficiency, minimal environmental impact, and reliable performance. By leveraging state-of-the-art technology, HeadPowder Engineering has revolutionized the way rare earth ore powders are transported, meeting the stringent demands of modern industrial applications.
Key Features and Benefits of Air Conveying Systems
Our air conveying systems for rare earth ore powders are engineered with precision to deliver optimal performance. Key features include high conveying capacity, low energy consumption, and the ability to handle fine powders without degradation. The systems are designed to minimize dust emissions, ensuring compliance with environmental regulations and creating a safer working environment. Additionally, the technology allows for seamless integration into existing processing lines, reducing downtime and enhancing overall operational efficiency.
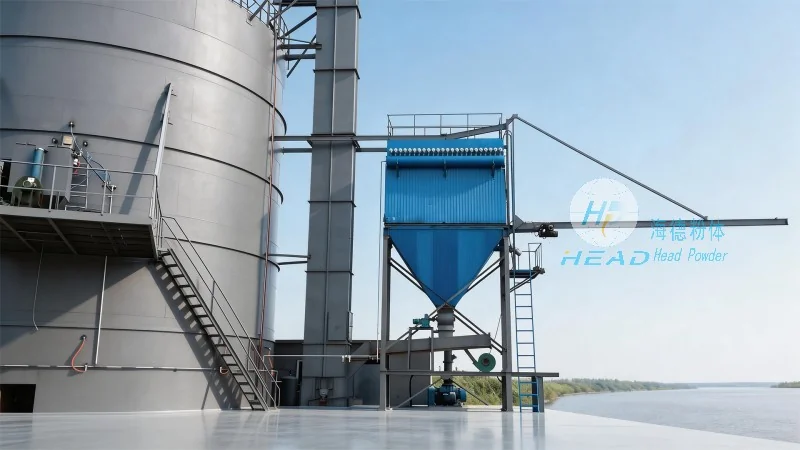
Environmental and Operational Advantages
One of the most significant advantages of air conveying systems is their environmental friendliness. Unlike traditional mechanical conveyors, which generate dust and require additional cleaning measures, air conveying minimizes particulate matter release, contributing to a cleaner industrial site. This not only reduces the risk of health hazards for workers but also lowers the need for extensive dust control infrastructure. From an operational perspective, the systems offer consistent and reliable material flow, reducing the likelihood of bottlenecks and ensuring smooth production processes. The low maintenance requirements further contribute to cost savings and increased productivity.
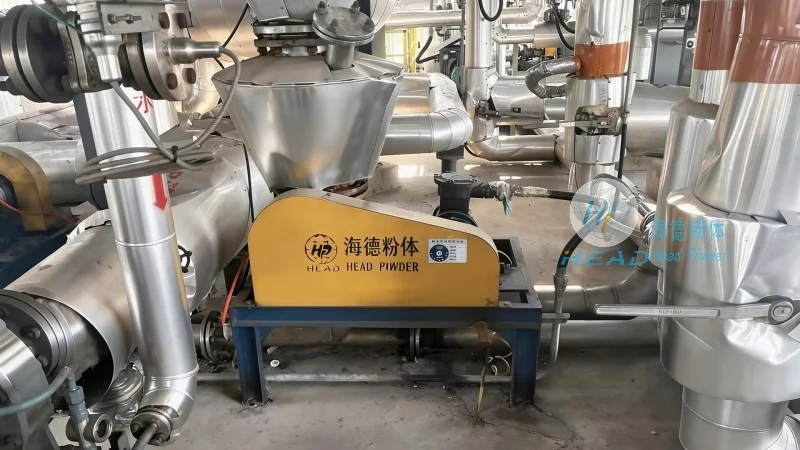
Customized Solutions for Diverse Applications
HeadPowder Engineering understands that each rare earth ore processing facility has unique requirements. Therefore, we offer customized air conveying solutions that are tailored to specific production needs. Whether it's handling high volumes of fine powders or integrating with existing equipment, our team of experts works closely with clients to design systems that meet their exact specifications. The company's commitment to innovation ensures that clients receive cutting-edge technology that adapts to evolving industry standards and operational demands.
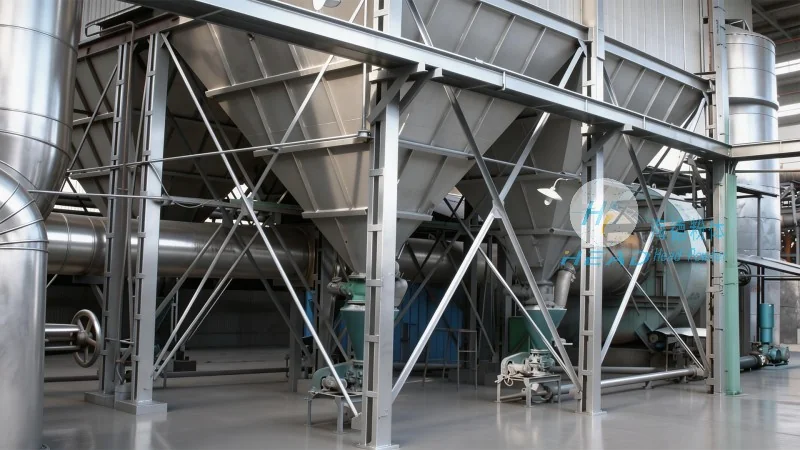
Reliability and Performance in Real-World Applications
With decades of experience in the material handling industry, HeadPowder Engineering has successfully implemented air conveying systems in numerous rare earth ore processing plants across China. These real-world applications have demonstrated the system's reliability and effectiveness. Clients have reported significant improvements in production efficiency, reduced operational costs, and enhanced environmental compliance. The systems have proven to be durable and low-maintenance, providing long-term value to businesses in the rare earth sector.
Conclusion and Company Overview
For businesses seeking an efficient and environmentally friendly solution for transporting rare earth ore powders, HeadPowder Engineering offers a comprehensive range of air conveying systems. With a focus on innovation, quality, and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder Engineering, based in Shandong, China, continues to lead the way in providing advanced material handling solutions that meet the highest standards of performance and sustainability. By choosing our air conveying systems, companies can enhance their operational efficiency, reduce environmental impact, and ensure the long-term success of their rare earth ore processing operations.