

Working Principle and Features of Vacuum Suction Type Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of vacuum suction type material pneumatic conveying equipment. This equipment is widely used in various industries for efficient material handling and transportation. The following article will delve into the working principle and key features of this advanced pneumatic conveying system.
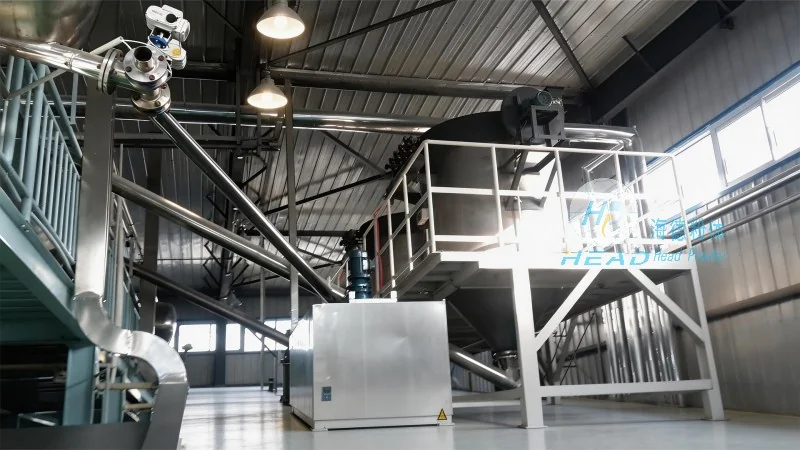
Working Principle of Vacuum Suction Type Material Pneumatic Conveying Equipment
The vacuum suction type material pneumatic conveying system operates by creating a negative pressure environment within the conveying pipeline. This is achieved through a vacuum pump that draws air and the material particles into the system. The material is then carried by the air flow from the material loading point to the discharge point. The process begins with the material being fed into the material hopper, where it is then drawn into the conveying pipeline by the vacuum pump. The air flow, typically at a velocity of 15-30 m/s, ensures that the material particles are suspended and transported efficiently. The conveying pipeline is usually made of stainless steel or other corrosion-resistant materials to handle various types of materials, including chemicals, food products, and pharmaceuticals. The system also includes a filter and cyclone separator at the discharge point to separate the material from the air, allowing for clean material collection and air recycling. The control system monitors the pressure, flow rate, and material level, providing real-time adjustments to maintain optimal conveying performance.
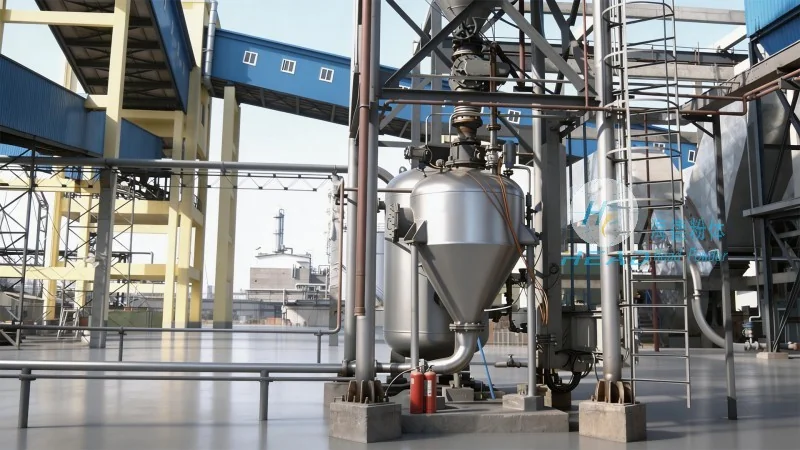
Key Features of Vacuum Suction Type Material Pneumatic Conveying Equipment
HeadPowder's vacuum suction type material pneumatic conveying equipment offers several distinct advantages that make it a preferred choice for industrial applications. Firstly, the system operates under negative pressure, which helps to contain dust and prevent material leakage, ensuring a clean and safe working environment. This is particularly important in industries such as food processing, pharmaceuticals, and chemical manufacturing, where product purity and safety are critical. Secondly, the equipment is highly efficient in terms of energy consumption, with the vacuum pump and air flow system optimized for minimal power usage. This not only reduces operational costs but also contributes to environmental sustainability. Thirdly, the conveying process is gentle on the material, reducing the risk of particle degradation or agglomeration, which is crucial for sensitive materials like pharmaceutical powders or food ingredients. The system's design minimizes mechanical stress on the material, preserving its quality and properties. Additionally, the system is flexible and can be easily integrated into existing production lines, with modular components that allow for customization based on specific material and application requirements. This adaptability makes it suitable for a wide range of industries, including food, pharmaceuticals, chemicals, and mining. The equipment also features advanced control systems that provide real-time monitoring and adjustment of the conveying parameters, ensuring optimal performance and reliability. These controls can be programmed to adjust the vacuum level, air flow rate, and material feed rate, allowing for precise control over the conveying process and minimizing downtime.
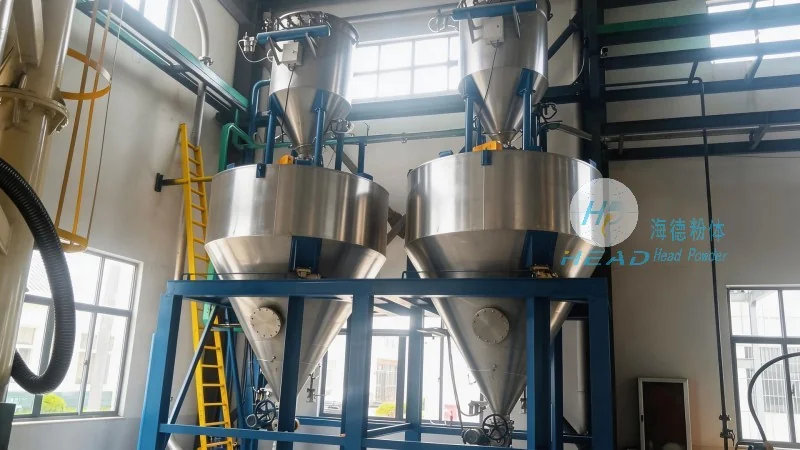
Company Information
HeadPowder, the manufacturer of this advanced vacuum suction type material pneumatic conveying equipment, is a reputable company based in Shandong, China. The company is dedicated to providing high-quality industrial solutions for material handling and transportation. With a strong focus on research and development, HeadPowder continuously improves its products to meet the evolving needs of various industries. The company's products are designed to be durable, efficient, and reliable, ensuring long-term performance and customer satisfaction. The headquarters is located in Shandong, China, where the company's team of experts works tirelessly to deliver innovative solutions to its clients worldwide.