

Working Principle and Features of a Pneumatic Conveyor for Manganese Sulfate Material
HeadPowder, a leading manufacturer based in Shandong, China, specializes in industrial equipment solutions, including advanced pneumatic conveyors designed for handling manganese sulfate material. This article explores the working principle and key features of such conveyors, providing insights into their efficiency and practical applications in material handling processes.
About HeadPowder Engineering Co., Ltd.
HeadPowder is a professional company dedicated to the research, development, and production of industrial machinery. With a strong focus on innovation and quality, the company has established itself as a trusted supplier in the field of material handling equipment. Headquartered in Shandong, China, HeadPowder leverages its expertise to deliver reliable and efficient solutions tailored to the needs of various industries.
Pneumatic Conveyor for Manganese Sulfate Material: An Overview
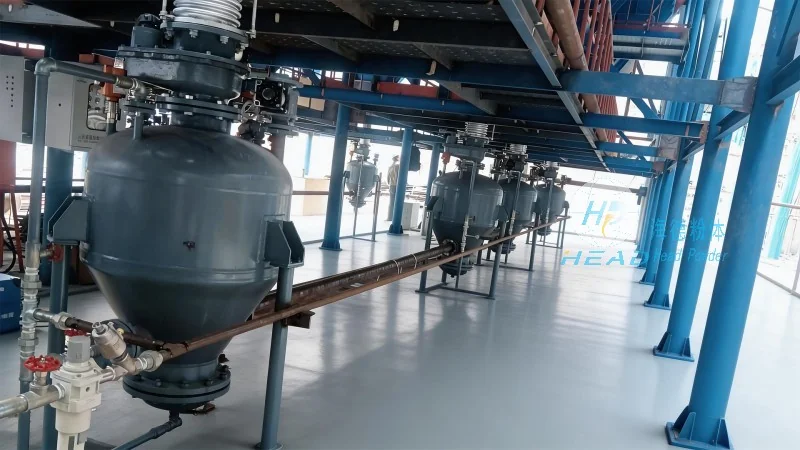
When dealing with manganese sulfate, a common industrial chemical, the need for efficient and safe material handling equipment is crucial. A pneumatic conveyor is an ideal solution, as it offers a dust-free, low-maintenance method to transport bulk materials like manganese sulfate. This equipment is specifically designed to handle the unique properties of manganese sulfate, ensuring optimal performance and minimal operational issues.
Working Principle of the Pneumatic Conveyor
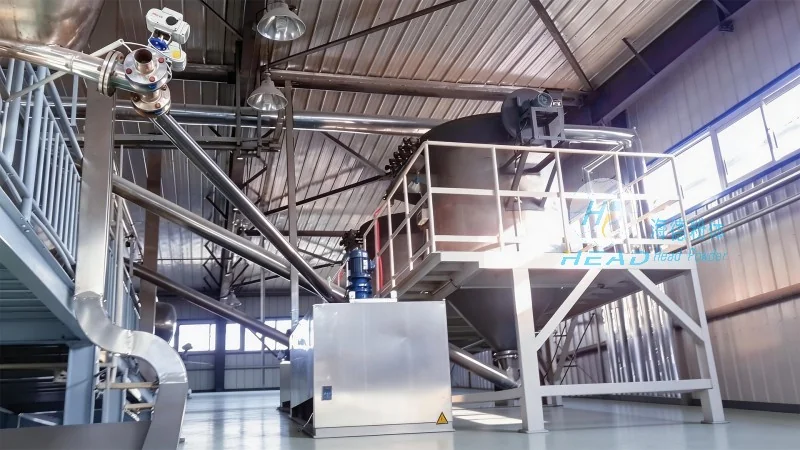
The pneumatic conveyor operates on the principle of air flow to transport solid materials. There are two main types: suction (or negative pressure) and pressure (or positive pressure) systems. For manganese sulfate, a suction system is often preferred due to the material's characteristics. The conveyor draws the material into a pipeline using a vacuum created by a fan or blower. The material is then carried through the pipeline by the moving air, and the air and material are separated at the discharge point. The system includes components such as a hopper, a fan, a pipeline network, and a discharge valve. The hopper holds the manganese sulfate, which is then fed into the pipeline as the air flow pulls it along. The fan generates the necessary airflow, and the pipeline transports the material to the destination. At the end of the pipeline, a separator or cyclone separates the material from the air, allowing the manganese sulfate to be collected in a container or processing unit.
Key Features and Advantages
Several key features make the pneumatic conveyor for manganese sulfate material a superior choice for industrial applications. First, it provides a dust-free environment, which is essential for maintaining workplace safety and compliance with environmental regulations. Unlike traditional belt or bucket elevators, the conveyor eliminates the risk of dust generation, reducing the need for additional dust control measures. Second, the system offers high efficiency in material transport, with the ability to handle large volumes of manganese sulfate quickly and reliably. The air flow ensures consistent material movement, minimizing downtime and increasing overall productivity. Third, the conveyor is designed for low maintenance, with fewer moving parts compared to other equipment. This reduces operational costs and the need for frequent repairs. Additionally, the system is flexible, allowing for easy integration into existing production lines or expansion as needed. The modular design enables customization to fit specific space constraints and material handling requirements. Another advantage is its ability to handle abrasive materials like manganese sulfate without significant wear and tear, as the air flow and separation process minimize direct contact between the material and equipment components.
Applications and Benefits in Industrial Settings
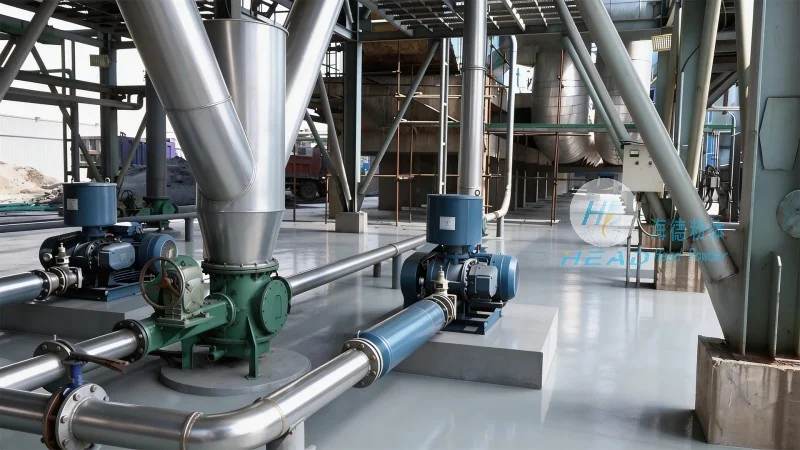
The pneumatic conveyor for manganese sulfate material is widely used in various industrial sectors, including chemical manufacturing, mining, and food processing. In chemical plants, it is used to transport manganese sulfate between processing units, ensuring a continuous flow of raw materials. In mining operations, the conveyor helps move manganese ore or processed manganese sulfate from storage to processing facilities. The benefits in these applications include improved safety, reduced labor costs, and enhanced production efficiency. The dust-free operation also contributes to a healthier work environment, reducing respiratory issues among workers. Furthermore, the system's ability to handle abrasive materials makes it suitable for long-term use in harsh industrial conditions, providing a reliable solution for consistent material transport.
Conclusion
HeadPowder Engineering Co., Ltd. offers a highly effective pneumatic conveyor designed specifically for handling manganese sulfate material. By understanding the working principle and key features of this equipment, industries can enhance their material handling processes, improve safety, and reduce operational costs. The conveyor's efficiency, low maintenance, and dust-free operation make it an ideal choice for various applications. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide high-quality industrial solutions to meet the evolving needs of the market.