

Operation Process and Working Principle of Dust-Free Closed Powder Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced dust-free closed powder pneumatic conveying systems. HeadPowder, as the company is commonly known, is headquartered in Shandong, China, and has established itself as a trusted provider of solutions for efficient and safe powder transportation in various industrial applications.
Understanding the Core Components and Working Principle
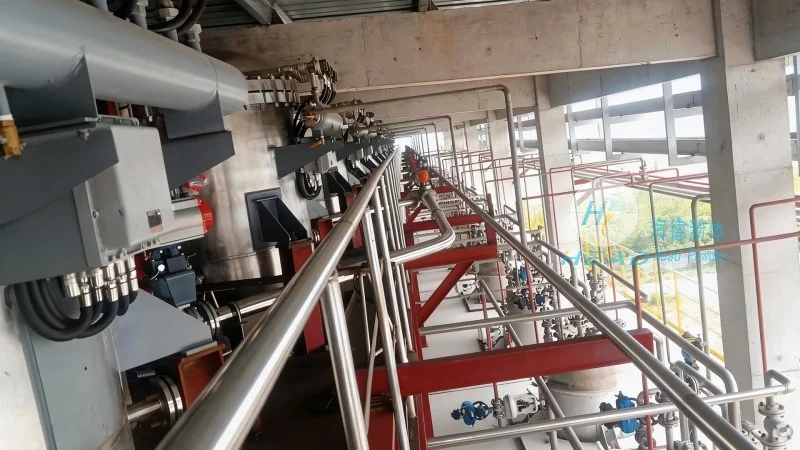
The dust-free closed powder pneumatic conveying system is engineered to transport bulk powders through a sealed pipeline network, eliminating the risk of dust contamination and ensuring compliance with stringent environmental and safety regulations. At the heart of this system lies a sophisticated combination of components that work in harmony to achieve seamless material transfer. The primary elements include a material feeder, a conveying pipeline, a control unit, and a dust collection system. The material feeder is responsible for introducing the powder into the system, while the conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the material under pressure. The control unit monitors and regulates the system's operation, ensuring optimal performance and preventing operational issues. The dust collection system, integrated into the pipeline network, captures any airborne particles, maintaining a clean and safe working environment.
Step-by-Step Operation Process
The operation of the dust-free closed powder pneumatic conveying system follows a systematic sequence that ensures reliable and continuous material transfer. The process begins with the preparation of the powder, where the material is loaded into the feeder hopper. Once the feeder is activated, it releases the powder into the conveying pipeline under controlled pressure. The system uses either positive or negative pressure to move the material through the pipeline, depending on the specific application requirements. As the powder travels through the pipeline, it is continuously monitored by the control unit, which adjusts the pressure and flow rate as needed to maintain consistent performance. The conveying process continues until the material reaches its destination, such as a storage silo, processing unit, or packaging line. The system then automatically shuts down or transitions to a standby mode, ensuring energy efficiency and minimizing downtime.
Key Advantages and Applications
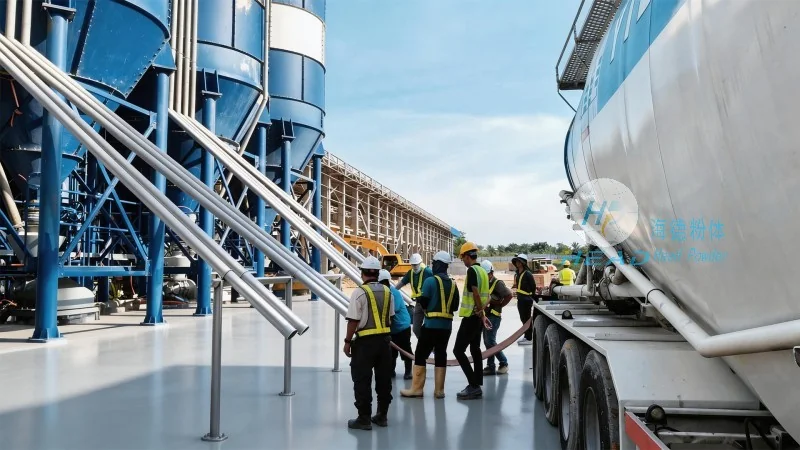
HeadPowder's dust-free closed powder pneumatic conveying systems offer numerous advantages over traditional open systems, making them ideal for industries that handle sensitive or hazardous powders. The primary benefits include complete dust containment, which reduces environmental impact and protects personnel from exposure to airborne particles. Additionally, the sealed system prevents cross-contamination between different materials, ensuring product purity and quality. The system's high efficiency and low maintenance requirements contribute to cost savings and increased productivity. These systems are widely used in pharmaceutical, food, chemical, and agricultural industries, where the handling of powders requires strict adherence to hygiene and safety standards. Whether transporting fine powders, granules, or bulk materials, HeadPowder's solutions provide reliable and efficient powder handling solutions tailored to specific industrial needs.
Customization and Integration Capabilities
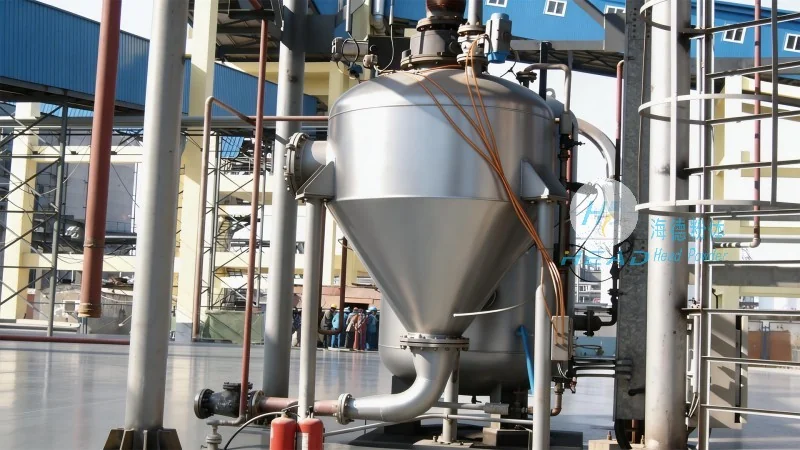
HeadPowder understands that each industrial application has unique requirements, and therefore, offers comprehensive customization options for its dust-free closed powder pneumatic conveying systems. The company works closely with clients to design systems that meet specific material characteristics, flow rates, and operational conditions. Customization may include adjustments to the pipeline diameter, material of construction, control system features, and integration with existing equipment. HeadPowder's engineering team utilizes advanced simulation tools to optimize system performance and ensure compatibility with client facilities. The company also provides comprehensive installation and commissioning services, ensuring that the system is properly integrated and operates at peak efficiency. This approach ensures that clients receive a tailored solution that maximizes performance and minimizes operational challenges.
Maintenance and Longevity
Proper maintenance is crucial for the long-term performance and reliability of dust-free closed powder pneumatic conveying systems. HeadPowder provides detailed maintenance guidelines and support to ensure that clients can keep their systems in optimal condition. Regular maintenance tasks include checking and replacing filters, inspecting pipeline integrity, and calibrating control systems. The company's spare parts inventory is well-stocked, ensuring that any necessary components are readily available for quick replacement. By following the recommended maintenance schedule, clients can extend the lifespan of their equipment and minimize the risk of unexpected downtime. HeadPowder's commitment to quality and customer support ensures that clients receive reliable and durable systems that deliver consistent performance over their operational life.