

Calcium Hydroxide Powder Pneumatic Conveying and Automatic Feeding System
HeadPowder, a leading engineering solutions provider based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying and automatic feeding systems tailored for calcium hydroxide powder handling. This comprehensive system integrates state-of-the-art technology to ensure efficient, safe, and reliable material transport and proportioning in industrial applications.
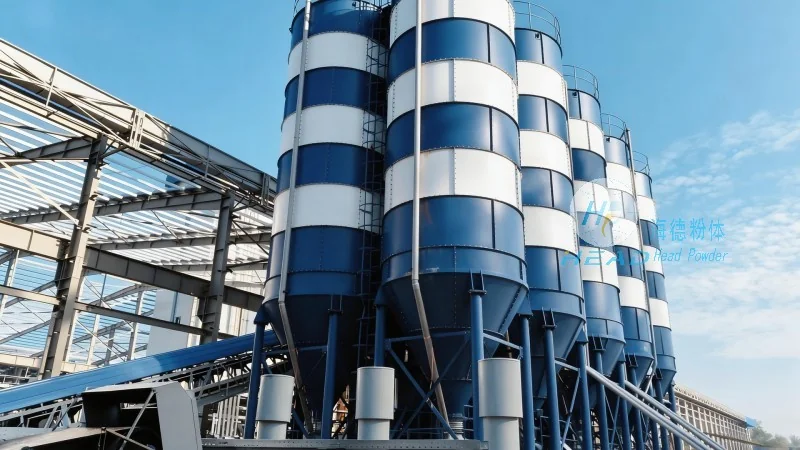
System Overview and Core Components
The Calcium Hydroxide Powder Pneumatic Conveying and Automatic Feeding System is engineered to address the unique challenges of handling fine, dusty, or bulk calcium hydroxide powder. The system typically comprises several key components, including a dust collector, a pneumatic conveying pipeline, a rotary valve or feeder for material discharge, and an automated control unit. Each component is meticulously designed to work in harmony, ensuring seamless material flow from storage to processing units. The pneumatic conveying mechanism utilizes compressed air to transport the powder through the pipeline, minimizing product degradation and contamination risks. The automatic feeding system, often integrated with a weighing or volumetric control module, allows for precise and consistent material proportioning, which is critical for maintaining product quality and process efficiency.
Advantages of Pneumatic Conveying for Calcium Hydroxide Powder
Compared to traditional mechanical conveying methods, pneumatic conveying offers several distinct advantages when handling calcium hydroxide powder. Firstly, it eliminates the need for complex mechanical components like screw conveyors or belt conveyors, which are prone to material buildup and wear. This reduces maintenance costs and extends the system's operational lifespan. Secondly, pneumatic systems provide excellent dust control, as the entire conveying process is enclosed within a sealed pipeline. This not only enhances workplace safety by preventing dust exposure but also ensures compliance with environmental regulations. Thirdly, the flexibility of pneumatic conveying allows for easy integration with existing production lines or expansion of the system to accommodate increased production demands. The system's ability to handle varying powder flow rates and particle sizes further enhances its adaptability across different industrial applications.
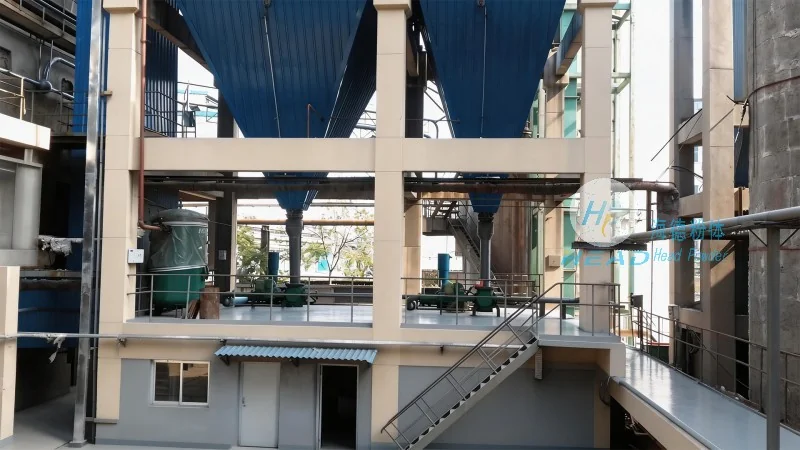
Automatic Feeding and Precision Control
The automatic feeding component of the system is a critical feature that ensures consistent and accurate material delivery. Equipped with advanced sensors and control algorithms, the feeding system can be programmed to deliver specific quantities of calcium hydroxide powder based on real-time process requirements. This precision is essential in applications where the chemical composition of the final product is tightly regulated, such as in water treatment, construction, or chemical manufacturing. The system may incorporate features like load cells for weight-based measurement or volumetric feeders for consistent flow rates, depending on the specific application. The integration of these control mechanisms minimizes human error and ensures that the feeding process remains stable even under varying operational conditions. This reliability is crucial for maintaining product uniformity and meeting strict quality standards.
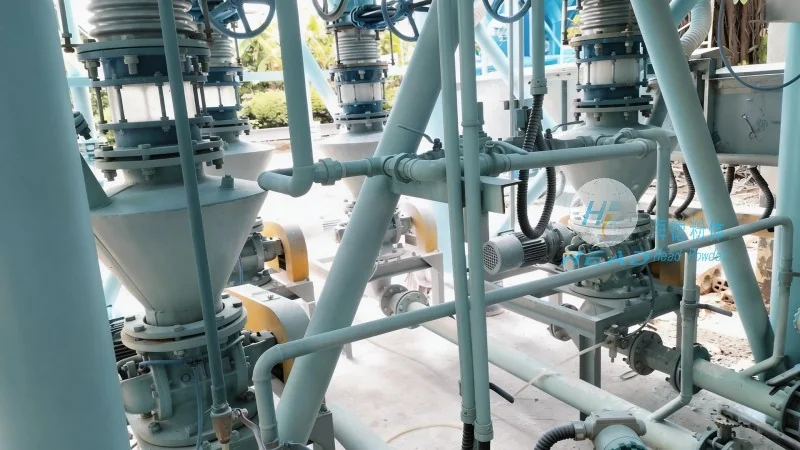
Enhanced Safety and Environmental Compliance
Handling calcium hydroxide powder requires strict adherence to safety and environmental guidelines due to its potential to cause respiratory irritation and environmental contamination. The pneumatic conveying system addresses these concerns by maintaining a sealed environment throughout the material transport process. The dust collector, a key component of the system, captures any airborne particles, preventing them from escaping into the workplace or the environment. This not only protects workers from inhalation hazards but also ensures that the facility remains compliant with local and national environmental regulations. Additionally, the system's design minimizes the risk of material spillage or leakage, further enhancing operational safety. The use of high-quality materials and robust construction ensures that the system can withstand the corrosive nature of calcium hydroxide, extending its service life and reducing long-term maintenance needs.
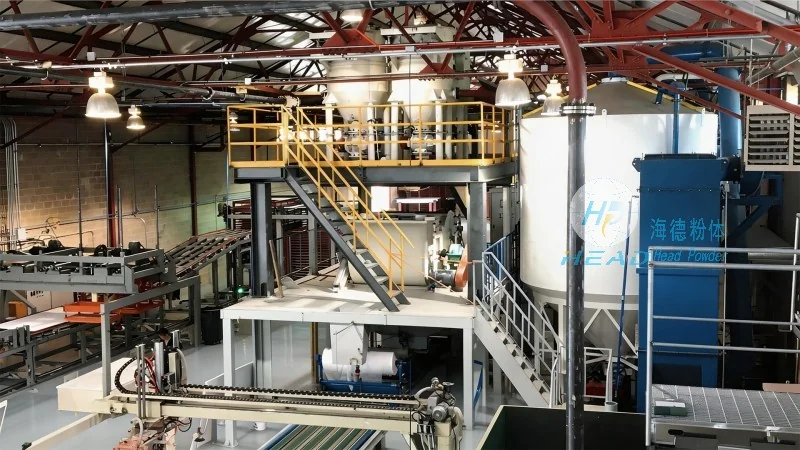
Customization and Scalability for Diverse Applications
HeadPowder recognizes that industrial applications vary widely, and a one-size-fits-all solution is rarely optimal. Therefore, the Calcium Hydroxide Powder Pneumatic Conveying and Automatic Feeding System is designed with flexibility in mind. The system can be customized to meet specific customer requirements, including different pipeline lengths, material flow rates, and control configurations. Whether for small-scale laboratory use or large-scale industrial production, the system can be scaled to accommodate varying production volumes. The modular design allows for easy integration of additional components, such as additional storage silos, secondary conveying lines, or process control interfaces. This adaptability ensures that the system can evolve with the customer's growing needs, providing a long-term solution that delivers consistent performance and value.
Conclusion and Service Commitment
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers a comprehensive solution for calcium hydroxide powder handling through its advanced pneumatic conveying and automatic feeding system. By combining cutting-edge technology with rigorous engineering standards, the system ensures efficient, safe, and reliable material transport and proportioning. The advantages of this system, including reduced maintenance, enhanced safety, and precise control, make it an ideal choice for industries requiring high-quality calcium hydroxide powder processing. HeadPowder's commitment to quality and customer satisfaction is reflected in the robust design and customization options available, ensuring that clients receive a system tailored to their specific operational needs. With a focus on long-term performance and environmental responsibility, this system represents a reliable investment for any industrial facility handling calcium hydroxide powder.