

Principle of Sand Particle Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems for sand particles. The company's core product, the sand particle pneumatic conveying equipment, is engineered to efficiently transport sand and similar granular materials through an air-driven system. This technology offers a reliable and efficient solution for industries requiring consistent and low-maintenance material handling.
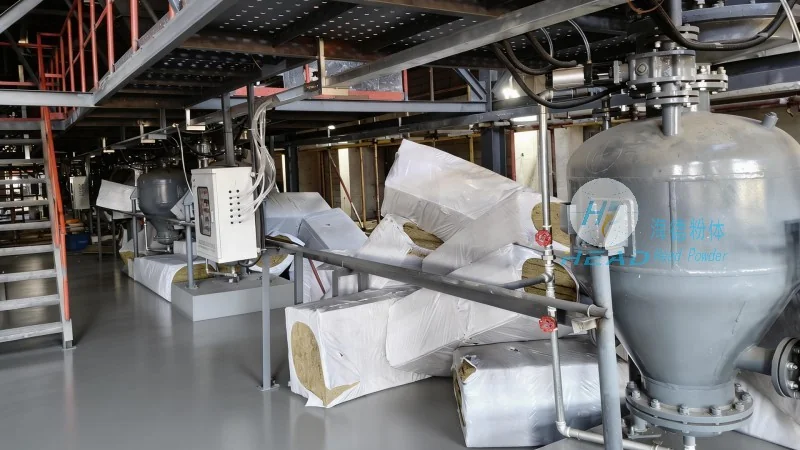
Working Principle of Pneumatic Conveying Systems
The fundamental principle behind the sand particle pneumatic conveying equipment is the use of compressed air to move particles through a pipeline. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a discharge point. When the system is activated, the blower generates a high-pressure air stream that draws the sand particles from the hopper into the pipeline. The air flow carries the particles through the system, ensuring a continuous and controlled flow. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
Key Components and Their Functions
The sand particle pneumatic conveying equipment comprises several critical components, each playing a vital role in the overall operation. The hopper serves as the storage and feeding unit, holding the sand particles and providing a consistent feed to the system. The blower or compressor is the heart of the system, generating the necessary air pressure to move the particles. The pipeline network connects the hopper to the discharge point, with appropriate fittings and valves to control the flow direction and pressure. The discharge point, often equipped with a filter or separator, collects the sand particles and separates them from the air, ensuring clean and efficient material delivery.
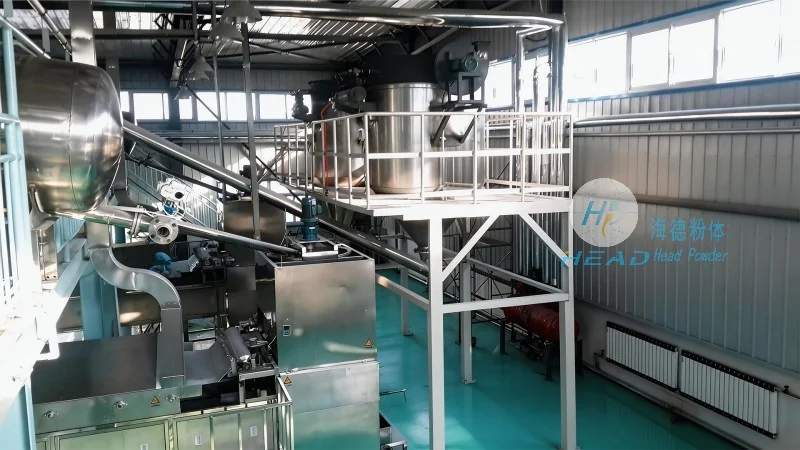
Advantages of Using Pneumatic Conveying for Sand Handling
Compared to traditional mechanical conveying methods, the sand particle pneumatic conveying equipment offers several advantages. First, it provides a dust-free and hygienic environment, which is crucial for industries where contamination must be minimized. Second, the system is highly flexible, allowing for changes in the layout or direction of the pipeline without major modifications. Third, it reduces energy consumption and maintenance costs, as there are fewer moving parts and less wear and tear. Additionally, the system can handle a wide range of particle sizes and densities, making it suitable for various applications in construction, mining, and manufacturing.
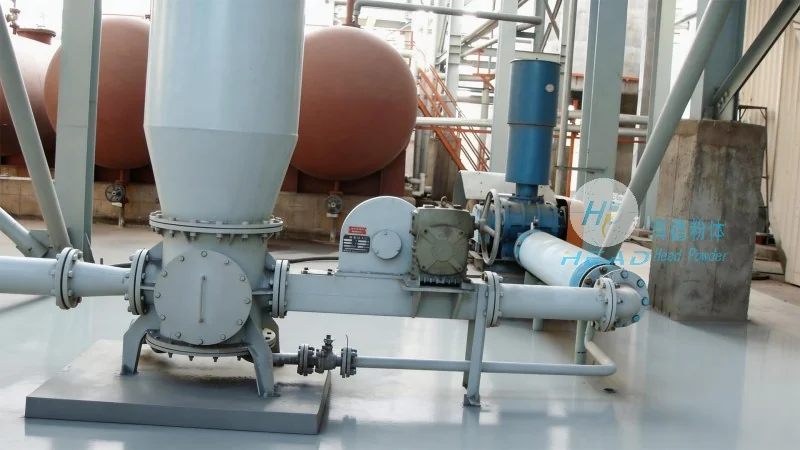
Applications in Different Industries
The sand particle pneumatic conveying equipment is widely used in various industries due to its versatility and efficiency. In the construction industry, it is used to transport sand from storage sites to construction sites, ensuring a steady supply of material. In the mining industry, it helps in the transportation of sand from mining sites to processing facilities, improving operational efficiency. In manufacturing, the equipment is used in sandblasting and foundry processes, where consistent sand delivery is essential for quality control. The system's ability to handle large volumes and maintain consistent flow rates makes it an ideal choice for high-demand applications.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of sand particle pneumatic conveying equipment. The company's commitment to quality and innovation has made its products a preferred choice in the industry. With a focus on customer satisfaction and technical excellence, HeadPowder continues to develop advanced solutions for material handling, ensuring reliable and efficient operation for its clients. The sand particle pneumatic conveying equipment represents a significant advancement in the field, offering a sustainable and effective method for transporting sand and similar granular materials.