

[What is a Tonne Bag Dust-Free Feeding Station Material Handling Equipment? What are its Design Prin
Understanding the Tonne Bag Dust-Free Feeding Station and its material handling equipment is crucial for industries that require efficient, clean, and safe material transfer processes. This equipment is specifically designed to handle bulk materials from tonne bags, ensuring minimal dust generation and maintaining a controlled environment. The design principles behind such systems are centered on integrating advanced engineering solutions to meet stringent industrial standards.
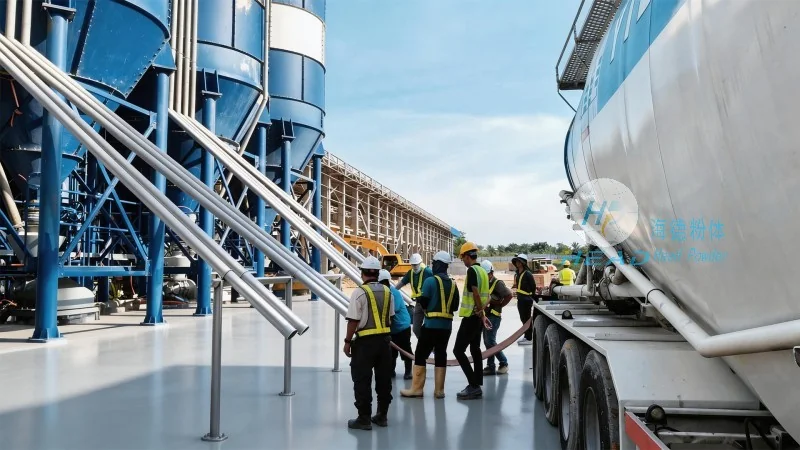
Overview of the Tonne Bag Dust-Free Feeding Station
The Tonne Bag Dust-Free Feeding Station is a specialized system used in various industrial sectors, including chemical, pharmaceutical, food processing, and construction. Its primary function is to transfer bulk materials from large tonne bags into processing equipment or storage facilities while minimizing dust exposure and maintaining a clean working environment. The system typically includes components like bag openers, dust collectors, and material conveyors, all working in tandem to ensure seamless operation.
Key Components and Their Functions
Several critical components make up the Tonne Bag Dust-Free Feeding Station. The first is the bag opener, which safely and efficiently opens the tonne bag without causing spillage or dust release. Next, the dust collection system, often equipped with high-efficiency filters, captures any airborne particles, ensuring compliance with environmental regulations and worker safety standards. The material conveyor, which may include screw conveyors or pneumatic systems, transports the material from the bag to the processing line. Additionally, the system may feature a bag emptying mechanism, such as a bag dump station, to further reduce dust and improve material handling efficiency.
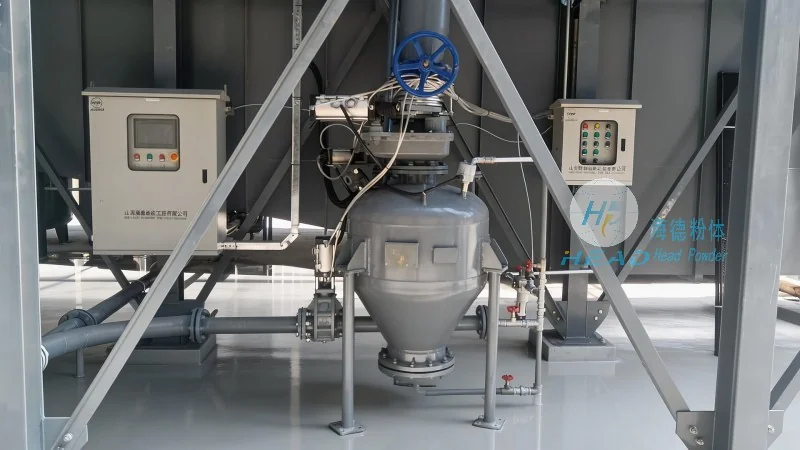
Design Principles and Engineering Considerations
The design of a Tonne Bag Dust-Free Feeding Station follows several key principles to ensure optimal performance and safety. First, the system is engineered to minimize dust generation through enclosed processes and effective sealing. This is achieved by integrating dust collection systems that capture particles at the source, preventing them from entering the workplace. Second, the equipment is designed for durability and ease of maintenance, with components that can withstand heavy usage and are simple to clean or replace. Third, the system is built to be scalable, allowing it to accommodate different bag sizes and material types. Engineers also consider factors like material compatibility, ensuring that the equipment materials do not react with the processed substances. Additionally, the design prioritizes user safety, with features like interlocks and emergency stop buttons to prevent accidents during operation.
Application Scenarios and Benefits
The Tonne Bag Dust-Free Feeding Station is widely used in industries where bulk material handling is essential. In the chemical industry, it is used to transfer raw materials for production, ensuring a clean and controlled environment that prevents contamination. In the pharmaceutical sector, the system is crucial for maintaining sterile conditions, as dust and contaminants can compromise product quality. The food processing industry also benefits from this equipment, as it helps maintain hygiene standards and prevents cross-contamination. The primary benefits of using such a system include improved worker safety, reduced environmental impact, increased operational efficiency, and enhanced product quality. By minimizing dust exposure, the system also reduces the risk of respiratory issues among workers and lowers the cost of cleaning and maintenance.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of material handling equipment, including Tonne Bag Dust-Free Feeding Stations. The company is based in Shandong, China, and has a strong reputation for producing high-quality, reliable equipment tailored to meet the specific needs of various industries. HeadPowder’s commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and safe material handling solutions. The company’s products are designed with advanced technology and engineering expertise, ensuring they meet international standards and provide long-term value to clients.