

What is a Tonne Bag Dust-Free Loading Station and Powder Conveying Machine? Exploring Design Princip
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in dust-free powder handling systems. The company is located in Shandong, China, and focuses on providing high-quality solutions for industrial powder processing. With years of experience in the industry, HeadPowder has developed advanced technologies to meet the growing demands for efficient and safe powder handling in various sectors.
Introduction to the Tonne Bag Dust-Free Loading Station
The Tonne Bag Dust-Free Loading Station is a critical component in modern powder handling operations. It is designed to handle bulk powders from tonne bags efficiently while maintaining a clean, dust-free environment. This system integrates advanced filtration and containment technologies to ensure safe and reliable material transfer. The station is particularly useful in industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining a dust-free workspace is essential for product quality and regulatory compliance.
Key Design Principles of the Loading Station
The design of the Tonne Bag Dust-Free Loading Station is based on several fundamental principles aimed at optimizing performance and safety. First, the system is constructed with a sealed enclosure that creates a negative pressure environment. This negative pressure ensures that any dust particles generated during the loading process are drawn into the filtration system rather than escaping into the surrounding air. The enclosure is typically made of high-quality materials, such as stainless steel or corrosion-resistant plastics, to withstand the demands of industrial use.
Second, the loading station incorporates high-efficiency particulate air (HEPA) filters. These filters are capable of capturing particles as small as 0.3 microns with an efficiency of 99.97%, effectively preventing dust from contaminating the workplace. The filtration system is designed to be easily accessible for maintenance and replacement, ensuring long-term operational reliability.
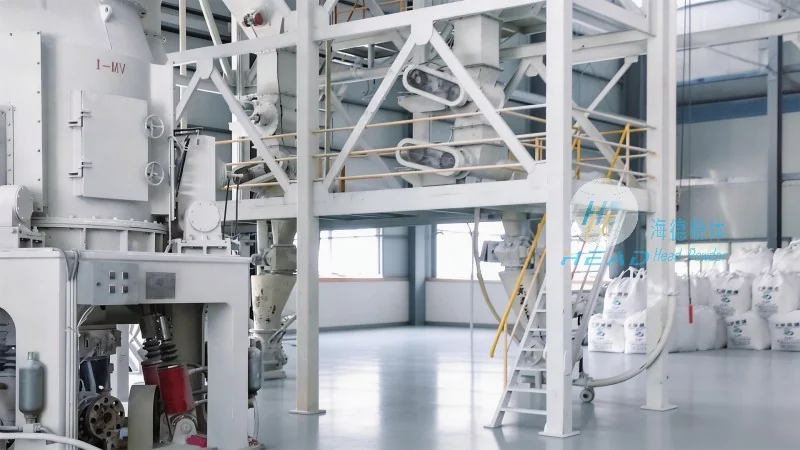
Third, the material flow is controlled by a series of conveyor mechanisms. These may include screw conveyors, pneumatic ducts, or belt conveyors, depending on the specific application. The conveyors are engineered to handle a wide range of powder types, from fine powders to bulkier materials, with minimal risk of clogging or blockage. The system also includes sensors and controls to monitor the flow rate and prevent overloading, ensuring smooth and consistent operation.
Operational Process and Safety Features
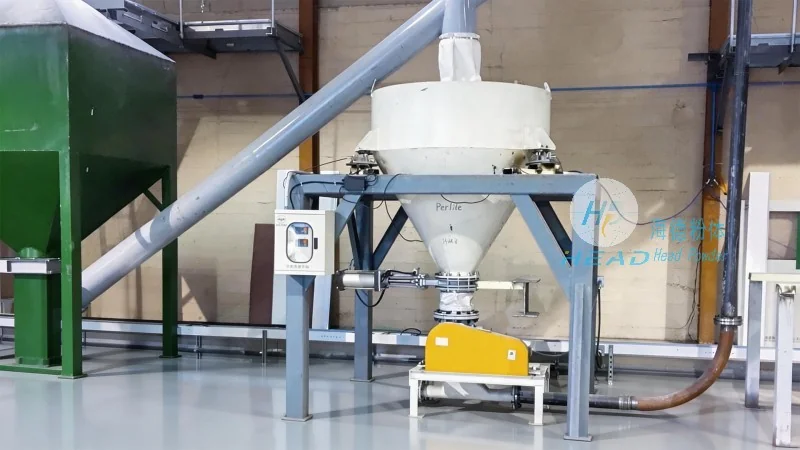
The operational process of the Tonne Bag Dust-Free Loading Station begins with the placement of a tonne bag onto the loading platform. The platform is designed to securely hold the bag in place, preventing it from moving during the loading process. Once the bag is positioned correctly, the system activates the filtration and conveyor components. The powder is then discharged from the bag into the processing line, with all dust and particles captured by the filtration system.
During operation, the station continuously monitors air quality and pressure. If any abnormalities are detected, such as a drop in pressure or an increase in dust levels, the system will automatically shut down to prevent contamination. This safety feature ensures that the workplace remains safe for operators and that the product remains free from dust contamination.
Advantages and Applications
One of the main advantages of the Tonne Bag Dust-Free Loading Station is its ability to handle large quantities of powder without generating excessive dust. This not only improves workplace safety but also reduces the risk of product contamination. Additionally, the modular design allows for easy integration with existing production lines, making it a versatile solution for various industrial applications.
These systems are widely used in industries such as pharmaceuticals, where product purity is paramount. In food processing, the dust-free environment helps maintain hygiene standards and prevent cross-contamination. In chemical manufacturing, the system ensures that powders are handled safely, reducing the risk of fire or explosion hazards associated with dust accumulation.
Conclusion
In summary, the Tonne Bag Dust-Free Loading Station and Powder Conveying Machine is a sophisticated piece of equipment that combines advanced engineering with practical functionality. By understanding its design principles and operational capabilities, businesses can enhance their powder handling processes, improve safety, and maintain high standards of product quality. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide solutions that meet the evolving needs of the industrial sector.