

What is a Dust-Free Powder Handling System? Understanding Its Design Principles
HeadPowder, a leading provider of industrial powder handling solutions, specializes in dust-free powder transport systems. This article explores the fundamental aspects of such systems, including their design principles and operational benefits, with a focus on how these systems enhance safety, efficiency, and compliance in various industrial applications.
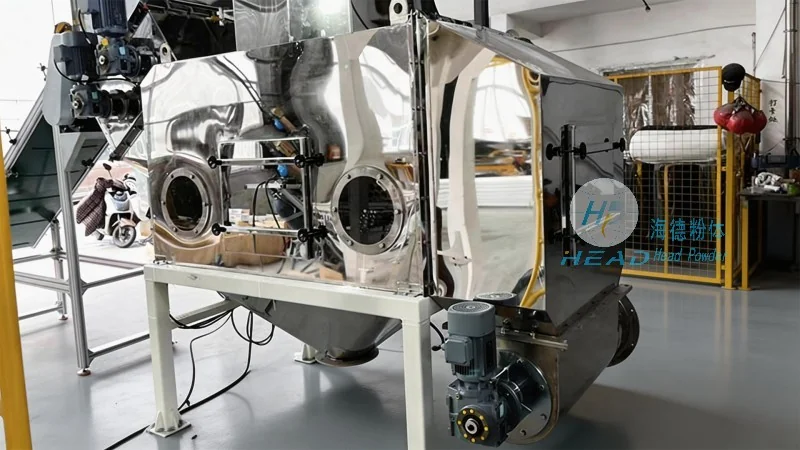
The Importance of Dust-Free Powder Handling Systems
In industries such as pharmaceuticals, food processing, and chemical manufacturing, the control of airborne dust is critical for maintaining product quality, ensuring worker safety, and adhering to regulatory standards. Dust-free powder handling systems are engineered to minimize or eliminate the release of powders into the environment, preventing contamination, respiratory hazards, and equipment damage. These systems are essential for industries where product purity and worker health are paramount, making them a cornerstone of modern industrial operations.
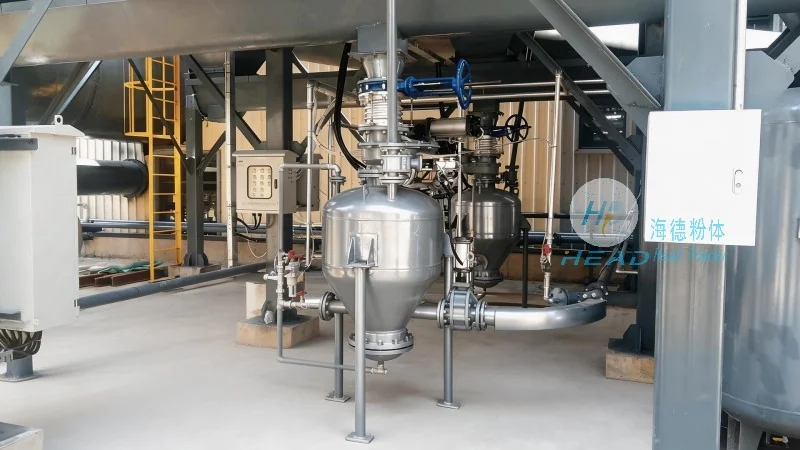
Key Design Principles of Dust-Free Powder Handling Systems
The effectiveness of a dust-free powder handling system relies on several core design principles. First, seal integrity is paramount. Systems incorporate multiple sealing mechanisms, such as double mechanical seals or hermetic enclosures, to prevent powder leakage at joints, valves, and transfer points. Second, controlled airflow is crucial. Negative pressure or closed-loop systems are often used to draw powders into the system while containing dust within the enclosure, reducing the risk of external contamination. Third, material selection plays a vital role. Components are typically made from stainless steel, food-grade plastics, or other corrosion-resistant materials to withstand harsh powder environments and maintain hygiene standards. Fourth, system integration ensures seamless operation with other equipment, such as hoppers, mixers, and packaging machines, minimizing points of failure and enhancing overall efficiency.
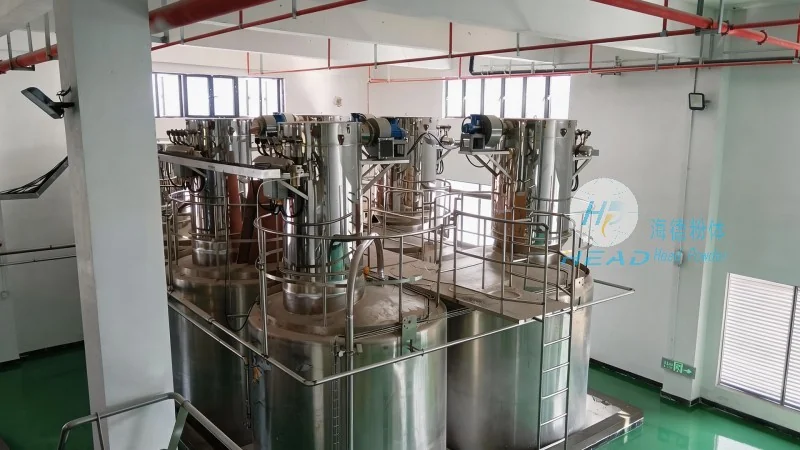
How HeadPowder's Systems Implement These Principles
Shandong HeadPowder Engineering Co., Ltd. leverages these design principles to develop customized dust-free powder handling solutions tailored to specific industry needs. For example, their systems may feature advanced double-seal technology to prevent powder leakage, integrated negative pressure controls to maintain a safe working environment, and durable materials like 316L stainless steel to resist corrosion and maintain hygiene. The company’s engineers work closely with clients to assess operational requirements, such as powder type, flow rates, and environmental regulations, to design systems that meet both functional and compliance needs. By prioritizing seal integrity, controlled airflow, and material quality, HeadPowder’s systems ensure reliable, dust-free operation while reducing maintenance costs and downtime.
Operational Benefits and Applications
Implementing a dust-free powder handling system offers numerous benefits. Firstly, it significantly reduces the risk of dust-related accidents, such as explosions or respiratory illnesses, by containing powders within the system. Secondly, it improves product quality by preventing cross-contamination and maintaining consistent powder characteristics. Thirdly, it enhances operational efficiency by minimizing material loss and reducing the need for cleaning and maintenance. HeadPowder’s systems are widely used in pharmaceutical manufacturing for drug powders, food processing for ingredients like flour or sugar, and chemical production for raw materials. In each case, the systems are designed to meet stringent industry standards, such as FDA or GMP requirements, ensuring compliance and customer trust.
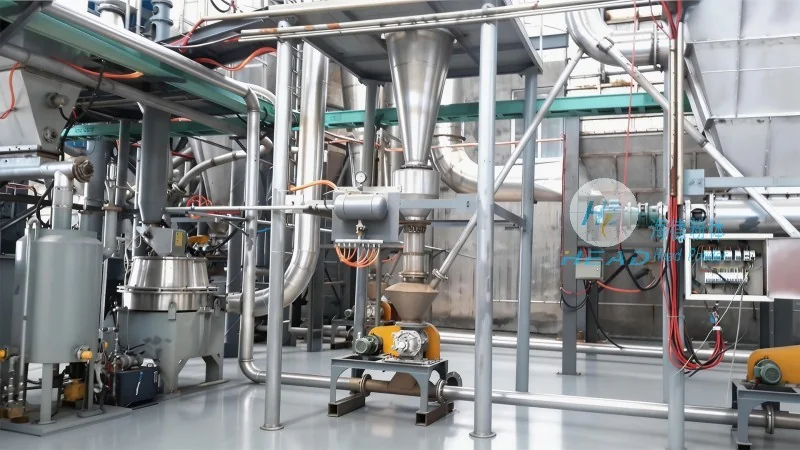
Conclusion: The Role of HeadPowder in Modern Powder Handling
As a trusted provider of dust-free powder handling systems, Shandong HeadPowder Engineering Co., Ltd. combines advanced design principles with industry expertise to deliver solutions that meet the evolving needs of modern industries. By focusing on seal integrity, controlled airflow, and high-quality materials, their systems provide reliable, efficient, and safe powder transport. With a commitment to innovation and customer satisfaction, HeadPowder continues to be a leader in the field, helping businesses maintain productivity while upholding the highest standards of safety and quality. Based in Shandong, China, the company serves clients globally, offering customized solutions that adapt to diverse operational environments and regulatory requirements.