

What is a Guar Gum Powder Material Handling System? And What Are Its Design Principles?
Guar gum powder, a key industrial ingredient widely used in various sectors such as food, pharmaceuticals, and chemicals, requires efficient and reliable material handling systems to ensure smooth production processes. The design of a guar gum powder material handling system is crucial for maintaining product quality, minimizing downtime, and optimizing operational efficiency. This article explores the fundamental aspects of such systems, focusing on their design principles and practical applications.
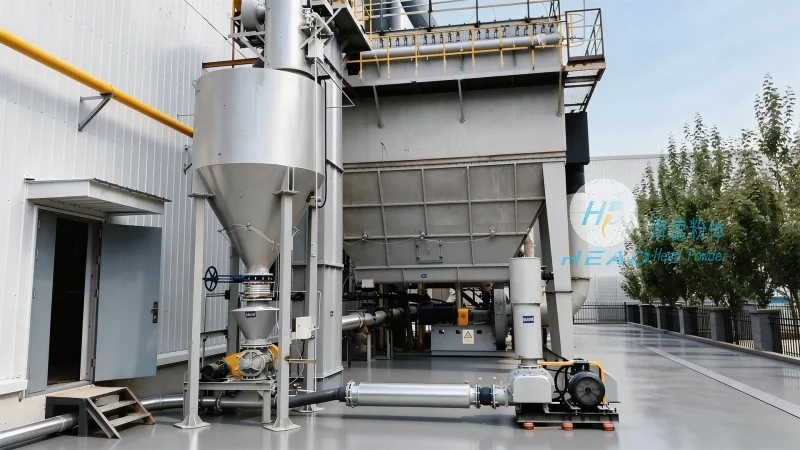
Understanding Guar Gum Powder Properties and Handling Challenges
Before delving into the design of a material handling system for guar gum powder, it is essential to understand the unique properties of this material. Guar gum is a natural polysaccharide derived from the guar bean, known for its high viscosity and water-binding capabilities. These properties make it highly hygroscopic, meaning it readily absorbs moisture from the air, which can lead to clumping, caking, and reduced flowability. Additionally, guar gum powder is often fine and powdery, posing challenges in terms of dust control, dust explosion prevention, and material transport without degradation.
Key Components of a Guar Gum Powder Material Handling System
A comprehensive guar gum powder material handling system typically includes several critical components designed to address the material's characteristics and operational requirements. These components work in synergy to ensure safe, efficient, and consistent material flow. The primary components include:
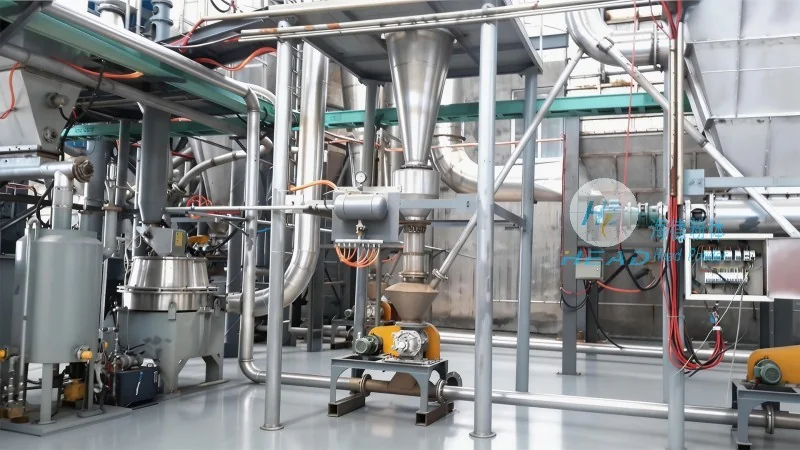
- Storage Silos: Large-capacity storage silos are used to store bulk guar gum powder. These silos are often equipped with aeration systems to control moisture levels and prevent caking. The design of the silo, including its shape and material, is crucial to minimize material degradation and ensure easy discharge.
- Conveying Equipment: Conveyors are essential for transporting guar gum powder from storage to processing areas. Screw conveyors, pneumatic conveyors, and bucket elevators are commonly used. Screw conveyors are ideal for horizontal or slight incline transport, while pneumatic conveyors are suitable for long-distance or vertical transport, especially when dust control is a priority.
- Dosing and Feeding Systems: Accurate dosing and feeding mechanisms are vital to maintain consistent product quality and process control. These systems ensure that the correct amount of guar gum powder is delivered to the next stage of production. Equipment such as rotary valves, gravimetric feeders, and loss-in-weight feeders are commonly employed to achieve precise and reliable feeding.
- Dust Control and Explosion Prevention: Given the fine nature of guar gum powder and its potential to create dust, dust control systems are integral to the material handling system. This includes dust collection hoods, filters, and explosion-proof designs. Proper ventilation and the use of explosion-proof electrical components are essential to comply with safety regulations and prevent dust explosions.
- Control and Monitoring Systems: Modern material handling systems are equipped with advanced control and monitoring systems. These systems allow operators to track material levels, monitor equipment performance, and adjust parameters in real-time. This enhances operational efficiency and helps in early detection of potential issues, reducing downtime.
Design Principles for Guar Gum Powder Material Handling Systems
The design of a guar gum powder material handling system follows several key principles aimed at optimizing performance, safety, and cost-effectiveness. These principles are tailored to address the specific challenges posed by guar gum powder and ensure that the system meets the requirements of the end-user.
- Minimizing Moisture Exposure: Guar gum's hygroscopic nature makes moisture control a top priority. The design incorporates features such as aeration systems in storage silos, sealed conveyor systems, and moisture-proof packaging to prevent moisture absorption. This helps maintain the powder's flowability and prevents caking, which can lead to blockages and equipment damage.
- Preventing Material Degradation: Guar gum powder is sensitive to physical and chemical changes. The system design ensures that the material is handled gently to avoid attrition and degradation. This includes using smooth, non-abrasive surfaces for equipment, minimizing impact during transport, and controlling temperature and humidity levels.
- Ensuring Dust Control and Safety: Dust control is critical to prevent dust accumulation and potential explosions. The system incorporates explosion-proof designs, dust collection systems, and proper ventilation. Regular maintenance and cleaning of equipment are also part of the design to ensure consistent dust control performance.
- Optimizing Flow and Efficiency: The design focuses on maximizing material flow efficiency while minimizing energy consumption. This involves selecting the appropriate conveying equipment, optimizing the layout of the system, and ensuring smooth transitions between different components. Proper alignment and maintenance of equipment are essential to maintain optimal performance.
- Compliance with Regulations: The system design adheres to relevant safety and environmental regulations. This includes standards for dust explosion prevention, material handling safety, and environmental protection. Compliance ensures that the system operates safely and meets legal requirements, reducing the risk of accidents and legal issues.
Case Study: A Practical Application by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, has successfully implemented a guar gum powder material handling system for a client in the food processing industry. The system was designed to handle 500 tons of guar gum powder per month, with a focus on maintaining product quality and operational efficiency.
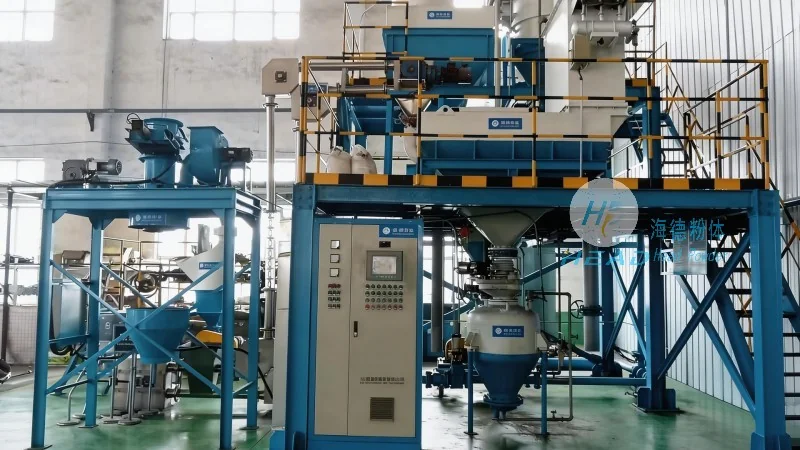
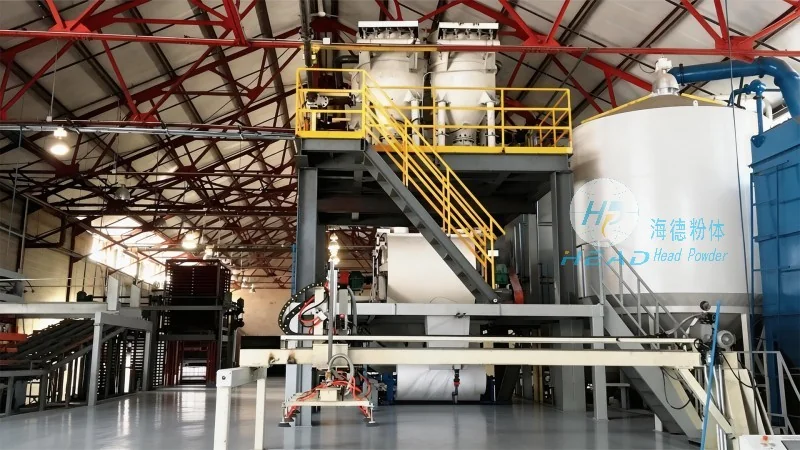
The system included a large storage silo with an aeration system to control moisture, a pneumatic conveyor for vertical transport, and a gravimetric feeder for precise dosing. The dust control system was designed to meet the client's safety requirements, with explosion-proof components and regular maintenance schedules. The client reported significant improvements in production efficiency, reduced downtime due to caking, and improved product quality after the system was installed.
Conclusion: The Importance of a Well-Designed Guar Gum Powder Material Handling System
In conclusion, a well-designed guar gum powder material handling system is essential for any industrial application involving this versatile ingredient. The system's design must address the unique properties of guar gum powder, including its hygroscopic nature, fine particle size, and sensitivity to moisture and handling. By incorporating key components such as storage silos, conveying equipment, dosing systems, and dust control measures, and adhering to design principles focused on moisture control, material protection, and safety, the system ensures efficient, safe, and reliable operation.
Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing tailored material handling solutions that meet the specific needs of their clients. By understanding the challenges and requirements of guar gum powder handling, they help industries optimize their production processes, reduce costs, and maintain high product quality. Investing in a properly designed material handling system is a strategic decision that can significantly impact the overall performance and success of industrial operations.