

Working Principle and Features of Limestone Powder Conveying Equipment
In industrial production, limestone powder conveying equipment plays a crucial role. These devices efficiently and safely transport limestone powder from one location to another, widely used in chemical, building materials, and environmental protection sectors. This article delves into the working principle of limestone powder conveying equipment and details its core features, helping readers fully understand the technical advantages and application value of such devices.
Working Principle of Limestone Powder Conveying Equipment
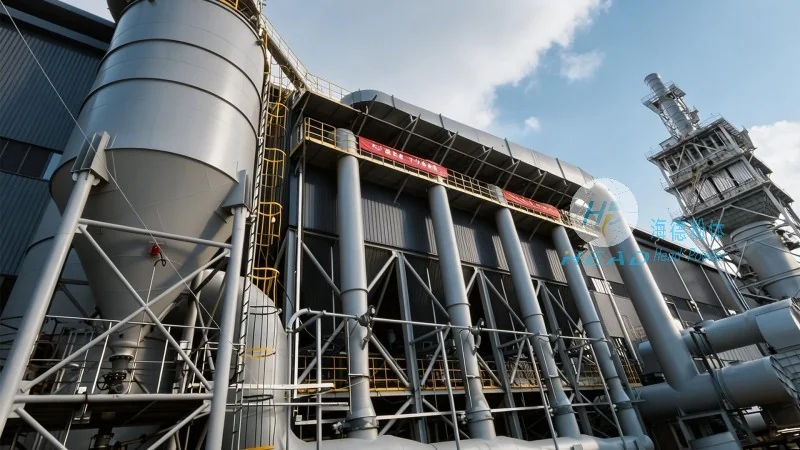
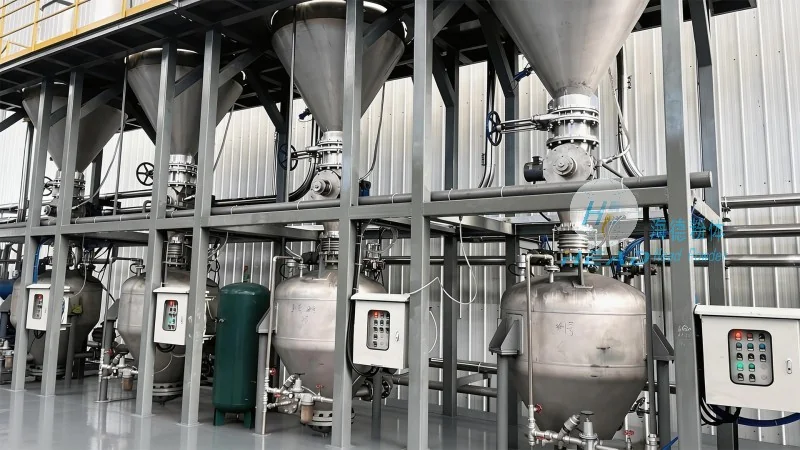
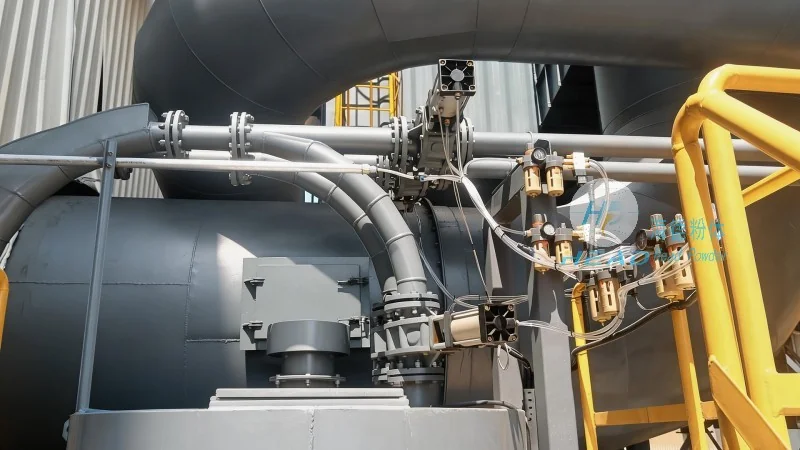
Limestone powder conveying equipment typically operates through a combination of mechanical and pneumatic systems designed to handle fine powders. The core mechanism involves the use of air or pressure to move the powder through a pipeline. For example, in a pneumatic conveying system, a blower or compressor generates airflow that carries the limestone powder particles. The equipment may include components such as a hopper, which stores the powder, a feeder that controls the flow rate, and a pipeline network that transports the material. The system ensures that the powder is moved without clogging or loss, maintaining consistent pressure and flow rates. Additionally, some systems incorporate cyclone separators or filters to separate the powder from the air, ensuring that the material is delivered to the destination in a dry and controlled manner. This integrated approach allows for efficient and reliable powder transport, minimizing downtime and operational costs. The design of the conveying system is tailored to the specific characteristics of limestone powder, such as its particle size distribution and moisture content, ensuring optimal performance under various operating conditions. By controlling the airflow velocity and pressure, the equipment can effectively transport even fine powders that are prone to agglomeration or dust generation, making it suitable for a wide range of industrial applications.
Key Features of Limestone Powder Conveying Equipment
HeadPowder's limestone powder conveying equipment is engineered with several distinctive features that enhance performance and usability. One of the primary features is its high efficiency in material handling, which is achieved through optimized airflow and particle size management. The equipment is designed to handle various types of limestone powders, including different fineness levels and moisture contents, without compromising on transport quality. Another notable feature is the robust construction, which ensures durability and long-term reliability in demanding industrial environments. The system also includes advanced control mechanisms that allow for precise regulation of flow rates and pressure, enabling operators to adjust the conveying process according to specific production needs. Furthermore, the equipment is equipped with safety features such as pressure relief valves and particle filters, which protect both the machinery and the environment from potential hazards. These features collectively contribute to a cost-effective and sustainable solution for limestone powder transport, making it an ideal choice for industries seeking reliable and efficient material handling solutions. The equipment also incorporates energy-efficient components, reducing operational costs and environmental impact. Its modular design allows for easy maintenance and upgrades, ensuring that the system can adapt to evolving production requirements over time.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the brand behind these advanced limestone powder conveying systems, is a leading manufacturer based in Shandong, China. The company specializes in the design, development, and production of high-quality powder handling equipment, with a strong focus on innovation and customer satisfaction. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner in the industry, providing tailored solutions that meet the unique requirements of clients across various sectors. The company's commitment to quality and technology has enabled it to deliver equipment that not only meets but exceeds industry standards, ensuring long-term performance and customer trust. With a dedicated team of engineers and technicians, HeadPowder continues to advance the field of powder conveying technology, offering reliable and efficient solutions for industrial applications. The company adheres to international quality management standards, ensuring that each product is rigorously tested and certified before delivery. This commitment to excellence has helped HeadPowder build a strong reputation in the global market, with clients from both domestic and international industries relying on their equipment for critical powder handling tasks.