

Working Principle and Features of Sucrose Powder Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and manufacturing of advanced powder handling systems tailored for the food and chemical industries. Among their product portfolio, sucrose powder conveying equipment stands out as a critical solution for efficient and reliable transport of granular sugar in processing facilities. This article delves into the working principle and key features of such equipment, providing insights into how they enhance operational efficiency and product quality in sugar processing applications.
Working Principle of Sucrose Powder Conveying Equipment
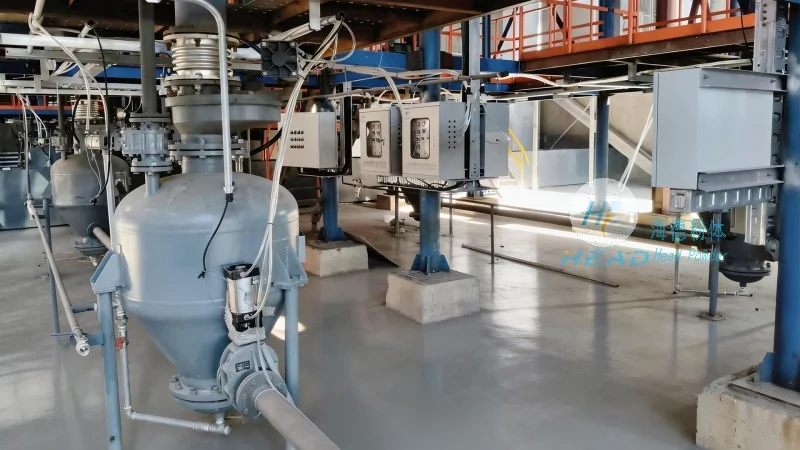
The core function of sucrose powder conveying equipment is to transport granular sucrose from a source point to a destination point within a processing plant. The system typically operates on a closed-loop or open-loop basis, depending on the specific requirements of the application. A common configuration involves a hopper or storage silo where the sucrose is stored, from which it is discharged into a conveyor system. The equipment may utilize various mechanisms such as pneumatic (air-assisted) conveying, mechanical screw conveyors, or bucket elevators to move the powder. In pneumatic conveying systems, for instance, the sucrose is drawn into a pipeline by a vacuum or pressure source, where it is mixed with air and transported to the target location. The control system, often integrated with sensors and valves, regulates the flow rate and pressure to ensure consistent and controlled delivery. This automated process minimizes human intervention, reduces labor costs, and maintains product integrity by preventing exposure to contaminants or moisture.
Key Features of Sucrose Powder Conveying Equipment
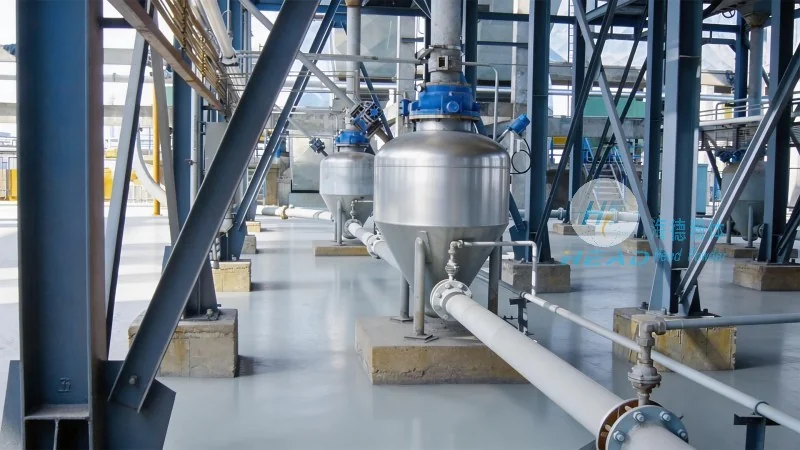
HeadPowder's sucrose powder conveying equipment is engineered with several distinct features that address the unique challenges of handling sucrose. Firstly, the equipment is designed to maintain a hygienic environment, which is paramount in food processing. Stainless steel construction, smooth surfaces, and easy-to-clean components are standard, ensuring compliance with regulatory standards like FDA and GMP. Secondly, the systems are highly efficient in terms of energy consumption and material handling. Advanced control algorithms optimize the air flow and pressure, reducing energy waste while maximizing throughput. This efficiency is particularly beneficial for large-scale sugar processing operations where operational costs are a significant factor. Thirdly, the equipment offers flexibility in terms of system integration. It can be customized to fit existing plant layouts, accommodating various distances and elevations between the source and destination. Additionally, the systems are equipped with safety features such as overload protection and emergency shut-off valves, ensuring operational safety and minimizing downtime. The ability to handle different particle sizes and flow rates without compromising performance is another notable feature, making the equipment versatile for diverse production needs.
Customization and Application-Specific Solutions
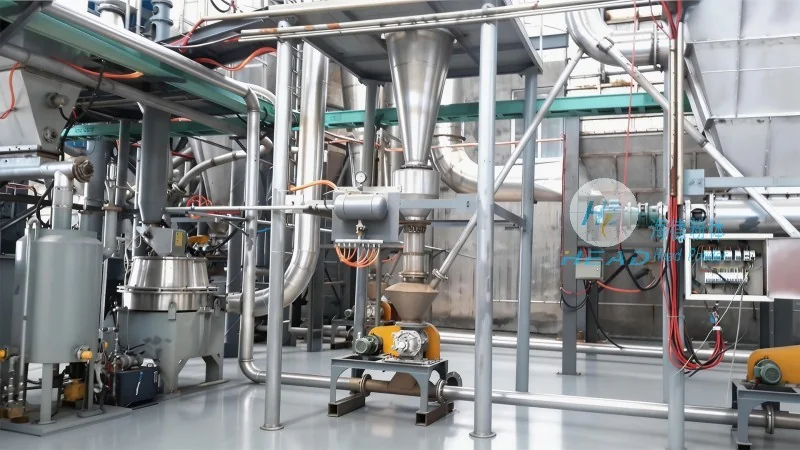
Shandong HeadPowder Engineering Co., Ltd. emphasizes customization to meet the specific needs of each client. The company's engineers work closely with customers to understand their production processes, material characteristics, and operational constraints. Based on this analysis, they design tailored conveying solutions that optimize performance and cost-effectiveness. For example, in applications where sucrose is used in high-speed blending or packaging lines, the equipment may be integrated with automated feeding systems to ensure a steady and precise flow of material. The company also considers factors such as the moisture content of the sucrose and the potential for dust generation, incorporating features like moisture control and dust suppression mechanisms into the design. This approach ensures that the conveying equipment not only meets the technical requirements but also enhances overall plant productivity and safety.
Conclusion
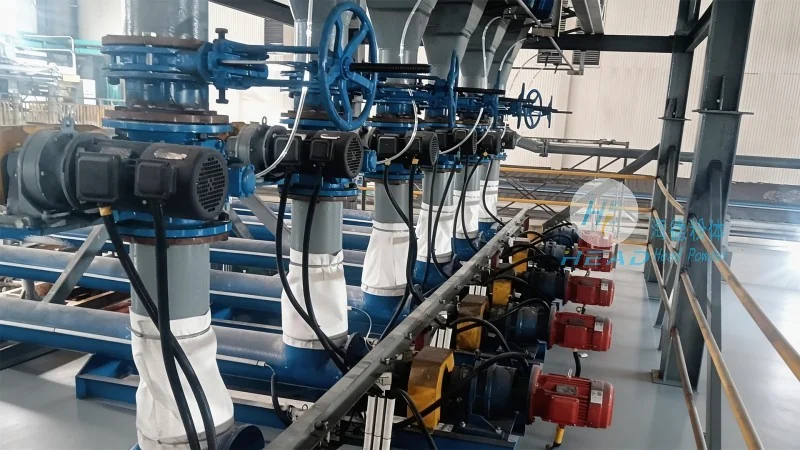
In summary, sucrose powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced technology with robust engineering to provide efficient, hygienic, and reliable transport of granular sucrose. The working principle, which typically involves pneumatic or mechanical systems controlled by intelligent software, ensures consistent and controlled delivery of the product. Key features such as hygienic design, energy efficiency, and flexibility make these systems ideal for modern sugar processing facilities. By prioritizing customization and customer collaboration, headpowder delivers solutions that address the unique challenges of each application, contributing to improved operational performance and product quality in the food and chemical industries.