

Working Principle and Features of Sodium Hexafluorophosphate Powder Handling Equipment
Understanding the working principle and key features of sodium hexafluorophosphate powder handling equipment is crucial for industries that rely on this chemical compound. This article provides an in-depth look at the technology behind such equipment, highlighting its operational mechanisms and distinctive attributes.
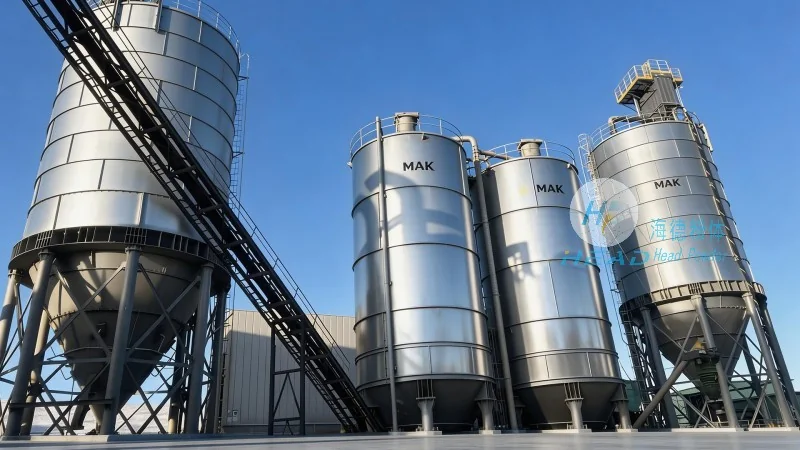
Introduction to Sodium Hexafluorophosphate Powder Handling Equipment
Sodium hexafluorophosphate (NaPF₆) is a white crystalline powder commonly used in various industrial applications, including pharmaceuticals, electronics, and chemical synthesis. The efficient and safe handling of this powder requires specialized equipment designed to manage its flow, storage, and transfer. The equipment developed by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) is engineered to meet these demands, ensuring optimal performance and reliability.
Working Principle of the Powder Handling Equipment
The core working principle of the sodium hexafluorophosphate powder handling equipment involves a combination of mechanical and pneumatic systems. The system typically includes a hopper, conveyor, and control unit, all working in tandem to transport the powder from its source to the desired destination. The hopper serves as the primary storage container, allowing for a steady supply of the powder. Within the hopper, a rotary valve or feeder controls the flow rate, ensuring a consistent and controlled discharge of the material. This controlled discharge is then transferred to a conveyor system, which may be a belt conveyor or a pneumatic conveyor, depending on the specific application and the required distance of transport.
The pneumatic conveyor, in particular, is often used for longer distances or when the powder needs to be transported in a closed system to prevent contamination or dust exposure. This system uses compressed air to create a flow of air and powder particles, moving the material through a pipeline. The control unit plays a critical role in regulating the entire process, monitoring parameters such as pressure, flow rate, and temperature to maintain optimal operation. Sensors and feedback mechanisms are integrated into the system to adjust the feed rate and ensure that the powder is handled safely and efficiently.
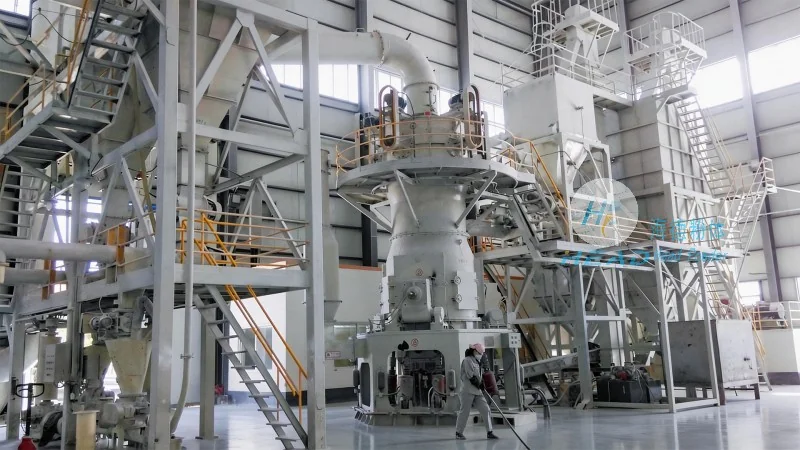
Key Features of the Equipment
The sodium hexafluorophosphate powder handling equipment from HeadPowder is characterized by several key features that enhance its performance and usability. One of the primary features is its high efficiency in handling fine powders, which is essential for maintaining the purity and quality of the sodium hexafluorophosphate. The equipment is designed to minimize particle agglomeration and segregation, ensuring that the powder remains well-mixed and free-flowing. This is achieved through the use of specialized hopper designs and internal baffles that promote uniform flow.
Another notable feature is the equipment's safety and environmental considerations. The system is equipped with dust collection and filtration systems to prevent the release of harmful particles into the air, adhering to environmental regulations. Additionally, the equipment incorporates explosion-proof and fire-resistant components, making it suitable for use in hazardous environments where sodium hexafluorophosphate may be handled. The control unit includes safety interlocks and emergency stop functions to prevent accidents and ensure operator safety.
The equipment also offers flexibility in terms of customization. HeadPowder can tailor the design and specifications of the powder handling system to meet the specific needs of each client, including different hopper sizes, conveyor lengths, and material handling capacities. This adaptability allows the equipment to be integrated seamlessly into existing production lines or used as a standalone unit for batch processing.
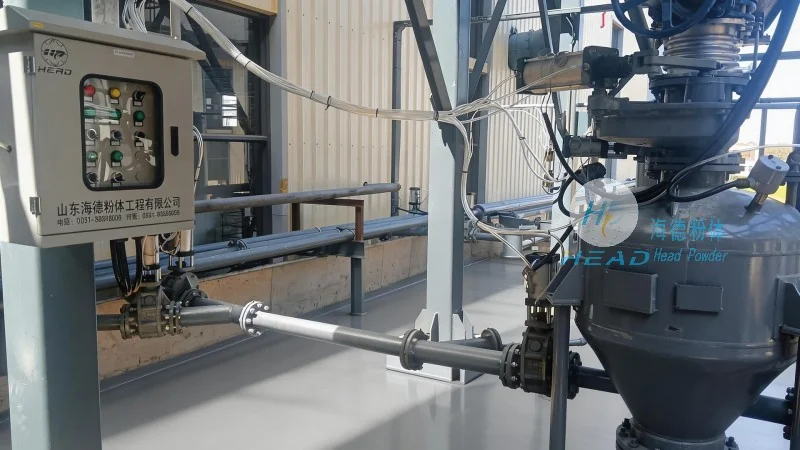
Operational Advantages and Applications
The efficient operation of sodium hexafluorophosphate powder handling equipment provides several advantages for industrial processes. By ensuring a consistent and controlled flow of the powder, the equipment reduces downtime and improves production throughput. The minimized risk of contamination and dust exposure enhances product quality and reduces the need for rework or waste disposal. Additionally, the energy-efficient design of the system contributes to lower operational costs and a smaller environmental footprint.
These advantages make the equipment suitable for a wide range of applications, including the production of pharmaceuticals, where the purity of sodium hexafluorophosphate is critical for drug formulation. In the electronics industry, the equipment is used in the manufacturing of semiconductors and other components, where precise powder handling is essential for achieving high-quality products. The versatility of the system also makes it applicable in chemical synthesis and research laboratories, where accurate and controlled powder transfer is required for experimental procedures.
Conclusion
In conclusion, the sodium hexafluorophosphate powder handling equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced technology with robust design to provide an efficient and reliable solution for handling this important chemical compound. The working principle, which integrates mechanical and pneumatic systems with intelligent control, ensures optimal performance, while the key features, such as high efficiency, safety, and customization, address the specific needs of various industries. By understanding these aspects, industries can make informed decisions about implementing this equipment to enhance their production processes and maintain product quality.