

Working Principle and Features of Inorganic Salt Crystal Powder Conveyors
Shandong HeadPowder Engineering Co., Ltd., situated in Shandong, China, specializes in the design, production, and supply of advanced powder handling equipment. Our company is committed to delivering efficient and reliable solutions for the transportation of inorganic salt crystals and other fine powders. The inorganic salt crystal powder conveyor is a core product in our portfolio, engineered to meet the rigorous demands of various industrial processes.
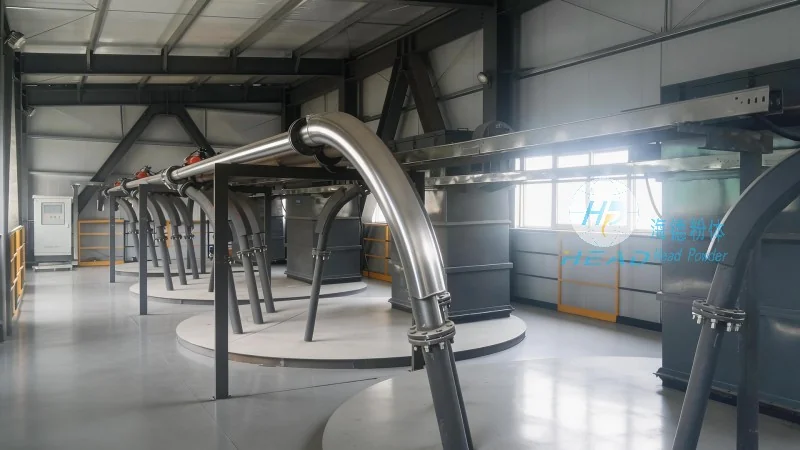
Working Principle of the Inorganic Salt Crystal Powder Conveyor
The inorganic salt crystal powder conveyor functions on a principle of continuous material movement within a closed system. It typically comprises a hopper for material storage, a conveyor mechanism (such as a belt or screw) for transporting the powder, and a discharge outlet. The hopper is designed to hold the inorganic salt crystals, ensuring a steady feed into the conveyor system. The conveyor mechanism moves the material from the inlet to the outlet, preventing accumulation and maintaining a consistent flow rate. Control valves and sensors regulate the speed and quantity of material transport, optimizing operation based on real-time conditions. This continuous motion ensures efficient and unidirectional material handling.
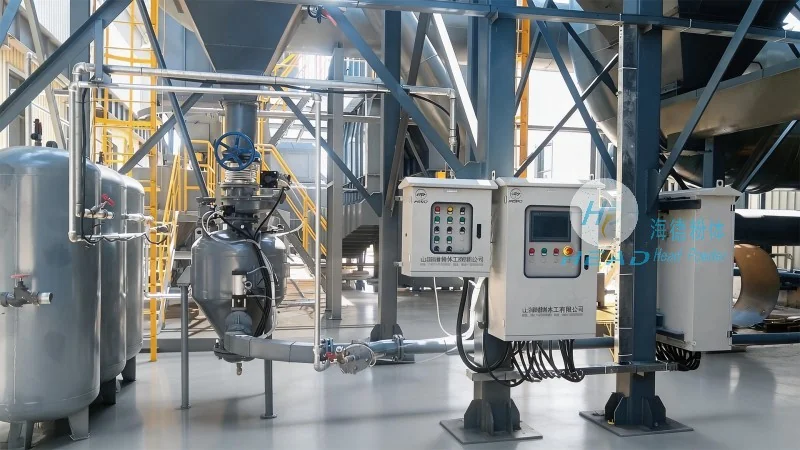
Key Features of the Inorganic Salt Crystal Powder Conveyor
One primary feature of our inorganic salt crystal powder conveyor is its high efficiency in handling fine powders. The design minimizes material degradation and dust generation, critical for preserving product quality and ensuring workplace safety. Constructed from durable materials like stainless steel, the conveyor resists corrosion from inorganic salts and prevents contamination, ensuring long-term performance and low maintenance costs. Another significant feature is adjustable speed control, allowing operators to customize the conveyor speed according to specific process requirements. This flexibility adapts to varying production volumes and material characteristics. The system also includes safety features like overload protection and emergency stop buttons, enhancing operational safety and compliance with industrial standards.
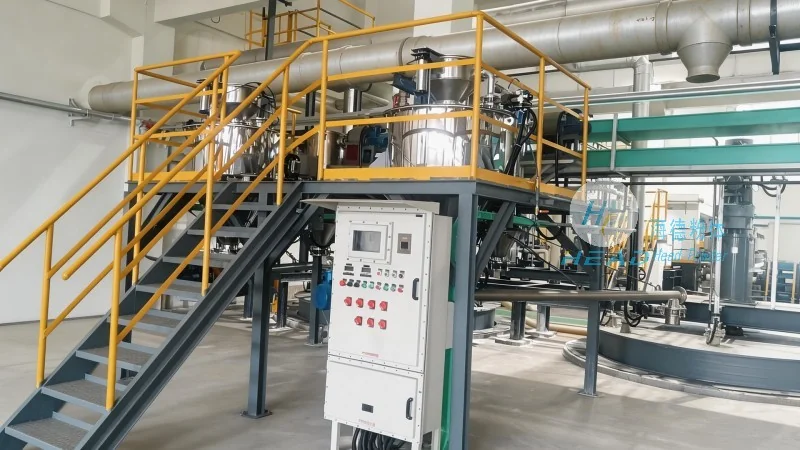
Advantages in Industrial Applications
The inorganic salt crystal powder conveyor offers several advantages in industrial settings. Its ability to handle abrasive materials reduces wear on components, extending equipment lifespan. The closed system design prevents dust dispersion, contributing to a cleaner environment and compliance with environmental regulations. The compact structure is suitable for installations with limited space, beneficial for facilities with spatial constraints. Additionally, low energy consumption and easy maintenance contribute to cost savings and operational efficiency. These features make the conveyor ideal for industries such as chemical processing, food processing, and pharmaceutical manufacturing, where fine powder handling is critical.
Customization and Technical Specifications
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial application has unique requirements. Our inorganic salt crystal powder conveyor can be customized to meet specific needs. We offer various configurations, including different conveyor lengths, widths, and material handling capacities. The system can be equipped with additional features like dust collection systems, temperature control units, and integration with automation systems. Technical specifications include adjustable speed ranges, material capacity from 0.5 to 50 tons per hour, and dimensions tailored to client space. Our engineering team collaborates closely with clients to ensure the final product meets all operational and safety standards.
Quality Assurance and After-Sales Service
We prioritize quality in every aspect of our product development and manufacturing. Our inorganic salt crystal powder conveyor undergoes rigorous testing to comply with international quality standards. High-quality materials and precision manufacturing guarantee reliability and durability. After delivery, we provide comprehensive after-sales service, including installation support, operator training, and regular maintenance. Our technical support team addresses any issues, ensuring the equipment operates at peak performance. By choosing our conveyor system, clients benefit from a reliable partner committed to delivering high-quality solutions and long-term support.