

Working Principle and Features of Tonne Bag Unloading Powder Handling and Conveying System Equipment
The tonne bag unloading powder handling and conveying system is a specialized industrial equipment designed to efficiently transfer bulk powders from large, heavy-duty bags (typically 1 tonne or more) into processing or storage facilities. This system is vital in industries such as food processing, pharmaceuticals, chemicals, and mining, where handling large quantities of powders safely and effectively is essential. The system integrates key components, including a bag unloader, conveyor, and control mechanisms, to ensure smooth and reliable operation.
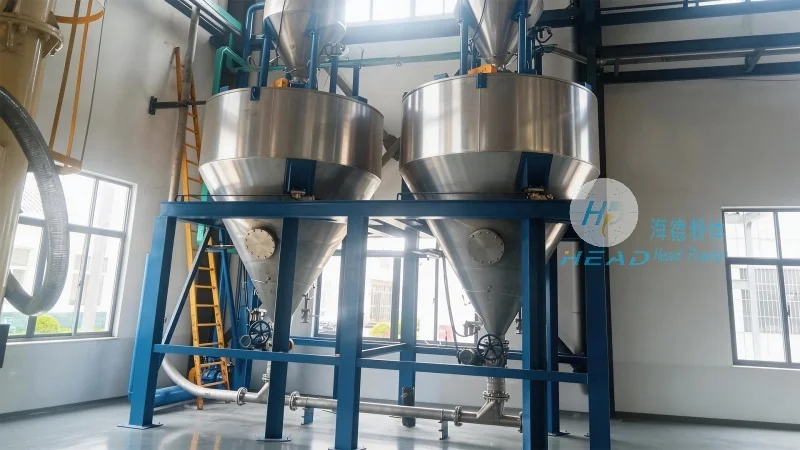
Working Principle of the Tonne Bag Unloading System
The operation of a tonne bag unloading powder handling system typically follows a sequential process. First, the heavy tonne bag is positioned on a loading platform or a specialized bag stand. The bag is then secured to prevent movement during unloading. Next, the bag is opened, either by cutting the top or using a specialized opening mechanism. The unloader, equipped with a rotating auger or pneumatic suction system, then extracts the powder from the bag. The auger, a screw-shaped conveyor, rotates to push the powder forward, while the suction system may use air to draw the powder out. The extracted powder is directed into a conveyor system, transporting it to the desired destination, such as a silo, storage tank, or processing unit. The control system monitors the entire process, ensuring consistent flow rates and safe operation. This integrated approach ensures powder transfer without spillage or contamination, maintaining product quality and safety.
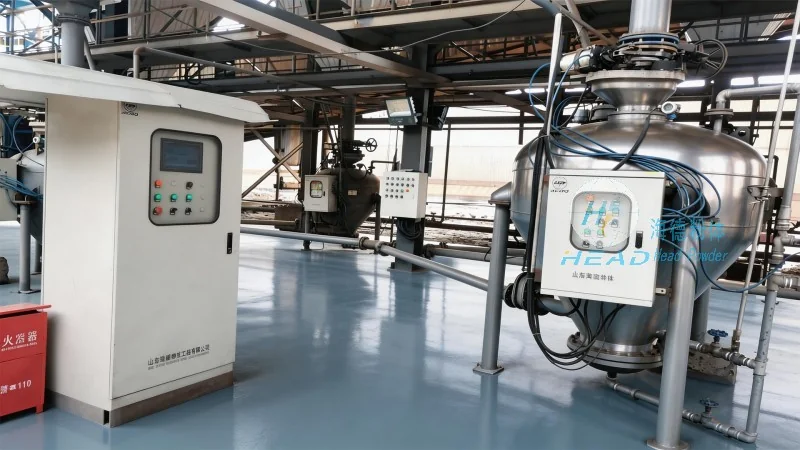
Key Features and Advantages of the System
One primary feature of the tonne bag unloading powder handling and conveying system is its ability to handle large volumes of bulk powders efficiently. The system processes multiple tonne bags per hour, reducing manual unloading time and labor, and minimizing human error or product contamination risks. Another important feature is adaptability to various powder types. The auger and suction system components can be adjusted or replaced to accommodate different powder characteristics, including moisture content, particle size, and flowability, making the system suitable for diverse applications. Additionally, the system includes safety features like overload protection and emergency stop buttons, ensuring safe operation and protecting personnel and equipment. The control system allows remote monitoring and operation, enabling operators to manage the process from a central location, enhancing flexibility and reducing on-site personnel needs, further improving efficiency.
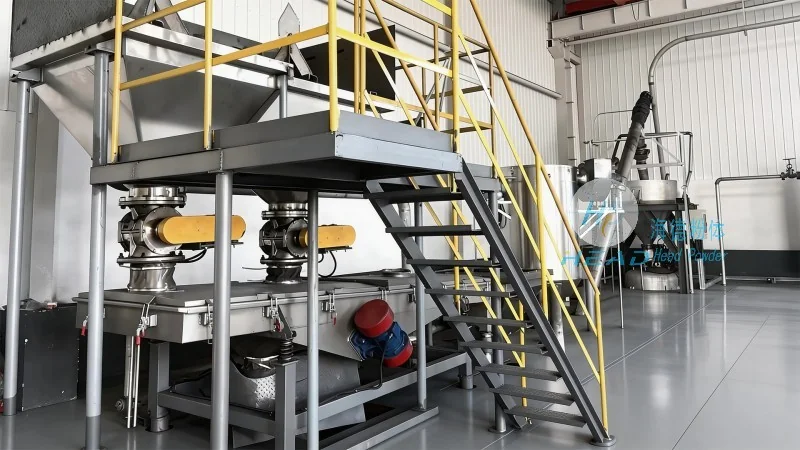
Reliability and Durability in Industrial Applications
The tonne bag unloading powder handling and conveying system is built to withstand continuous industrial use. High-quality materials, such as stainless steel and durable plastics, are used in component construction, providing corrosion and wear resistance. The auger and conveyor mechanisms feature heavy-duty bearings and robust motors, delivering consistent performance under high loads. Regular maintenance, including lubrication and component inspection, is recommended for long-term reliability. The system’s design minimizes maintenance needs, with easy access for cleaning and replacement, reducing downtime and costs. Its compact design allows installation in various industrial settings, including factories, warehouses, and processing plants, saving space and simplifying processing area layouts. The integration of the bag unloader and conveyor into a single unit optimizes workflow and operational efficiency.