

Working Principle and Features of Barley Material Pneumatic Conveying Equipment
Efficient material handling is a critical aspect of modern grain processing operations, particularly when dealing with bulk materials like barley. The pneumatic conveying system has emerged as a highly effective solution for transporting barley from storage to processing units. This article explores the working principle and key features of a barley material pneumatic conveying machine, highlighting its advantages in agricultural and food processing industries.
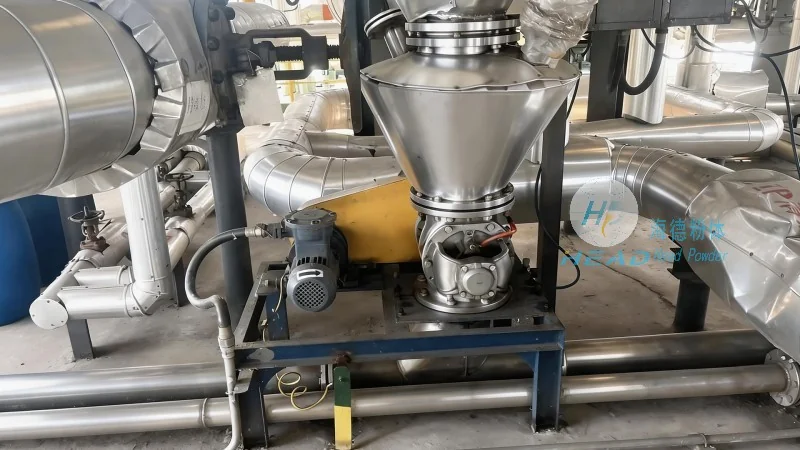
Introduction to Barley Pneumatic Conveying Systems
Barley, a staple grain used in brewing, animal feed, and food products, requires reliable and efficient transportation methods to maintain quality and minimize handling losses. Traditional methods such as bucket elevators or belt conveyors may pose challenges in terms of dust control, material degradation, and operational complexity. Pneumatic conveying offers a solution by using air to transport barley particles through a sealed system, ensuring a clean, hygienic, and continuous flow of material.
Working Principle of Barley Material Pneumatic Conveying Equipment
The core of a pneumatic conveying system for barley involves the use of a blower or fan to generate airflow within a network of pipes. The system typically operates under either negative pressure (suction) or positive pressure (pressure) to move the material. In a suction system, the fan creates a vacuum that draws barley from a storage bin or hopper into the conveying line. The material is then mixed with air and transported through the pipes to the destination point, such as a mill or silo. In a pressure system, the fan forces air and barley into the pipes, pushing the material forward. The system includes components like a hopper, a rotary valve for material discharge, a filter to remove dust, and a separator to separate the barley from the air at the end of the line.
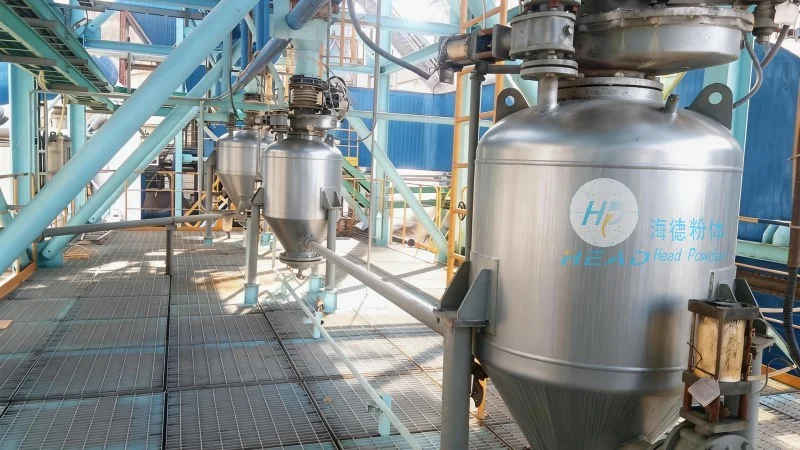
Key Features and Advantages of Barley Pneumatic Conveying Machines
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing high-quality pneumatic conveying equipment tailored for barley processing. The company's barley material pneumatic conveying machines are engineered with several key features that enhance performance and efficiency:
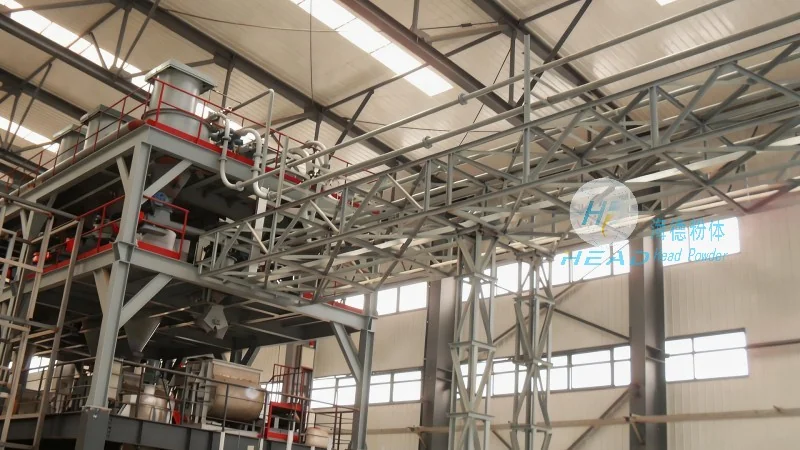
- High Efficiency and Capacity: The system can handle large volumes of barley with minimal downtime, ensuring consistent production flow. The design optimizes airflow and material velocity to maximize throughput without compromising material quality.
- Low Maintenance and Durability: Constructed with robust materials, the equipment is built to withstand the abrasive nature of barley particles and the demands of continuous operation. This reduces maintenance costs and extends the service life of the machinery.
- Hygienic and Clean Operation: The sealed system prevents dust and contamination, which is crucial for food-grade barley products. The design includes features like self-cleaning filters and easy-to-clean components, ensuring compliance with industry standards.
- Energy Efficiency: Advanced blower technology and optimized system design minimize energy consumption while maintaining high conveying efficiency. This contributes to lower operational costs and reduced environmental impact.
- Customizable and Scalable: The equipment can be tailored to specific production requirements, from small-scale operations to large industrial facilities. It can be easily integrated with existing processing lines, providing flexibility in system expansion.
Application in Barley Processing
Barley pneumatic conveying systems are widely used in various stages of barley processing, including:
- Storage and Transfer: Moving barley from storage silos or bins to processing units, such as malting or milling facilities.
- Processing Line Integration: Conveying barley to grinding or milling equipment, ensuring a steady supply of raw material for product manufacturing.
- Quality Control: The system can be integrated with sampling and testing equipment to monitor barley quality during transport.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides reliable and efficient barley material pneumatic conveying equipment that combines advanced technology with robust design. By understanding the working principle and key features of these systems, grain processing facilities can enhance operational efficiency, maintain product quality, and reduce costs. The company's commitment to quality and innovation ensures that their pneumatic conveying solutions meet the evolving needs of the agricultural and food processing industries.