

Principles and Working Scene Characteristics of Dust Powder Conveying System Equipment
HeadPowder, a leading provider of dust and powder conveying solutions, specializes in equipment designed to efficiently handle and transport various types of powders and dust materials. The company, based in Shandong, China, offers a range of systems tailored to meet the diverse needs of industrial applications. This article explores the fundamental principles behind these conveying systems and highlights the key working scene characteristics that define their effectiveness and versatility.
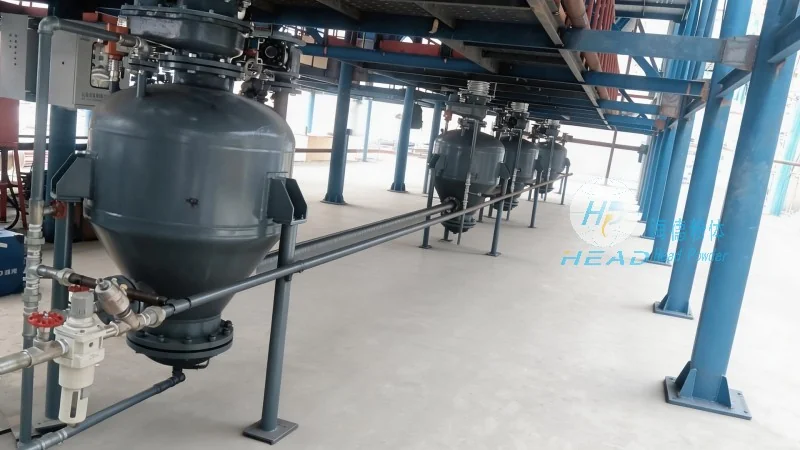
Company Overview and Background
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of dust powder conveying equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's products are engineered to ensure reliable performance, safety, and efficiency in handling powders and dusts across various industrial sectors. The company's headquarters is located in Shandong, China, where it conducts research, development, and production activities to deliver cutting-edge solutions for its clients.
The Core Principles of Dust Powder Conveying Systems
The fundamental principle of dust powder conveying systems is to transport bulk materials in a controlled manner, minimizing material loss, contamination, and operational hazards. These systems typically utilize a combination of mechanical components and control mechanisms to achieve efficient material movement. The primary goal is to ensure that powders and dusts are conveyed safely and effectively from one location to another, while maintaining the integrity of the material and preventing environmental contamination. Key principles include maintaining consistent flow rates, controlling pressure differentials, and ensuring proper sealing to prevent dust leakage. Advanced systems may also incorporate features such as variable speed drives, material flow monitoring, and automated control to optimize performance and reduce downtime.
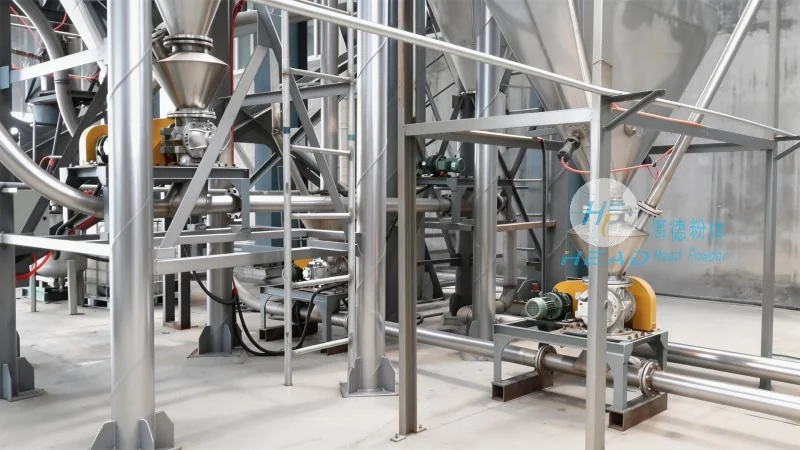
Working Scene Characteristics of Dust Powder Conveying Equipment
The working scene characteristics of dust powder conveying systems are tailored to the specific requirements of different industrial applications. These characteristics include adaptability to various material types, such as fine powders, granules, and bulk solids, and the ability to handle different flow rates and capacities. The systems are designed to operate in diverse environments, from cleanroom facilities to heavy-duty industrial plants, ensuring compatibility with a wide range of operational conditions. Another important characteristic is the system's ability to integrate with existing infrastructure, allowing for seamless integration into existing production lines or new installations. Additionally, the equipment is engineered to minimize maintenance requirements and maximize operational uptime, contributing to overall cost-effectiveness and productivity. The working scene also emphasizes safety features, such as dust suppression mechanisms, explosion-proof designs, and user-friendly controls, to protect personnel and equipment from potential hazards associated with powder handling.
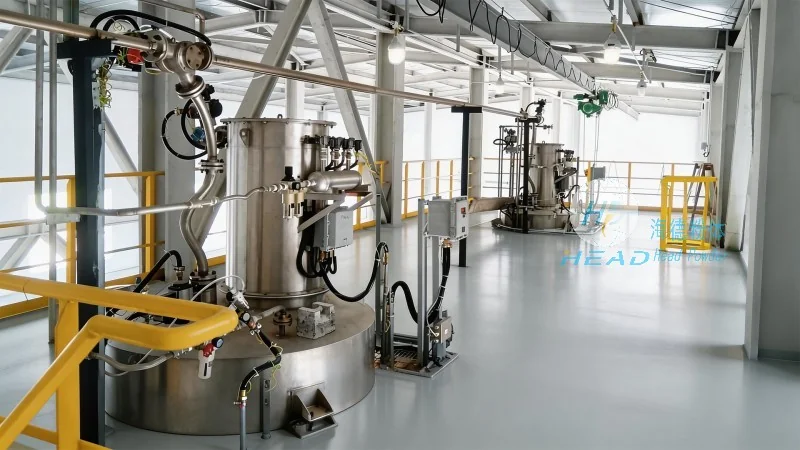
Key Applications and Industry Use Cases
Dust powder conveying systems are widely used across multiple industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, these systems are crucial for transporting active ingredients and excipients while maintaining stringent cleanliness and contamination control standards. The food processing sector relies on these systems to handle powders like flour, sugar, and spices, ensuring hygienic and efficient material movement. Chemical manufacturers use dust powder conveyors to transport raw materials and finished products, often requiring specialized designs to handle hazardous or reactive substances. In the mining industry, bulk material handling systems are essential for transporting ore and other minerals from processing plants to storage or shipping facilities. Each industry has unique requirements, and HeadPowder's conveying systems are customized to meet these specific needs, ensuring optimal performance and compliance with industry regulations.
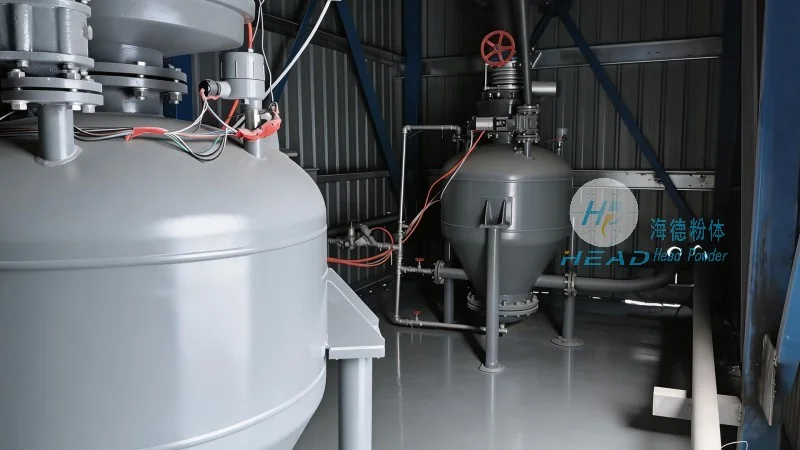
Advantages and Benefits of HeadPowder's Conveying Solutions
HeadPowder's dust powder conveying systems offer several advantages that make them a preferred choice for industrial applications. These include high efficiency in material transport, reduced labor costs due to automated operation, and improved safety through advanced control and monitoring features. The systems are designed to minimize material degradation and loss, which is critical for maintaining product quality and reducing waste. Additionally, the equipment is built with durability and longevity in mind, using high-quality materials and robust construction to withstand the rigors of continuous operation. The company's focus on customization allows clients to select systems that are tailored to their specific operational needs, ensuring optimal performance and cost-effectiveness. The working scene characteristics of these systems, such as low maintenance requirements and easy integration, further enhance their appeal to industrial users seeking reliable and efficient solutions.
Conclusion and Future Outlook
In conclusion, dust powder conveying systems are essential equipment for industries that handle bulk powders and dusts. The principles behind these systems focus on efficient, safe, and controlled material transport, while the working scene characteristics adapt to the diverse needs of various industrial applications. HeadPowder, with its expertise and commitment to quality, provides advanced conveying solutions that meet the demands of modern industrial operations. As technology continues to evolve, these systems will likely incorporate more sophisticated features, such as AI-driven control and predictive maintenance, to further enhance performance and reliability. The future of dust powder conveying equipment remains promising, with continued innovation aimed at improving efficiency, safety, and sustainability in material handling processes.