

Principle and Working Scene Characteristics of Tonne Bag Material Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and production of advanced material handling solutions. Among their product lineup, the tonne bag material conveying equipment stands out as a critical component for efficient bulk material transport in various industrial applications. This equipment is engineered to handle large volumes of materials, typically stored in tonne bags, and ensures seamless transfer from storage to processing or packaging stages.
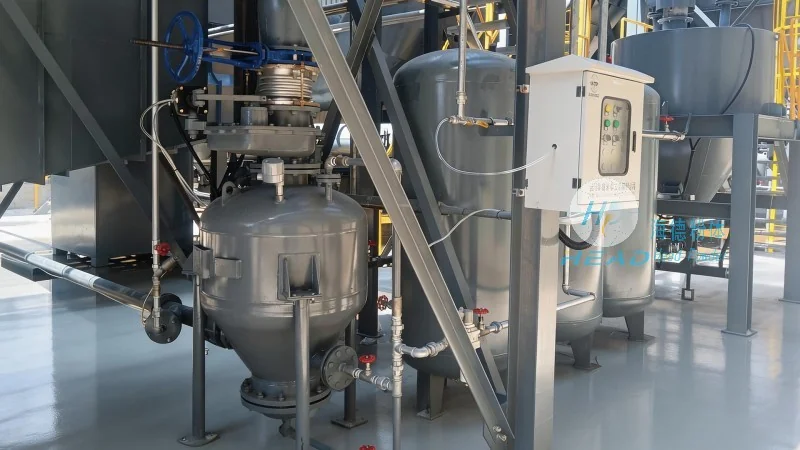
Principle of Tonne Bag Material Conveying Equipment
The core principle of tonne bag material conveying equipment revolves around the mechanical handling of bulk materials contained within flexible containers. These systems typically incorporate a combination of components such as feeders, conveyors, and lifting mechanisms. The process begins with the placement of a tonne bag on a loading platform or hopper. The equipment then uses a series of rollers, belts, or chains to lift and transport the bag horizontally or vertically. Key mechanisms include the use of hydraulic or electric actuators to control the movement of the conveyor system, ensuring precise positioning and stability. The design prioritizes durability and efficiency, with features like reinforced frames and wear-resistant materials to withstand heavy loads and continuous operation. The system is often integrated with sensors and control panels to monitor the conveying process, allowing for real-time adjustments and maintenance alerts. This mechanical approach minimizes manual labor, reduces handling time, and enhances overall operational productivity.
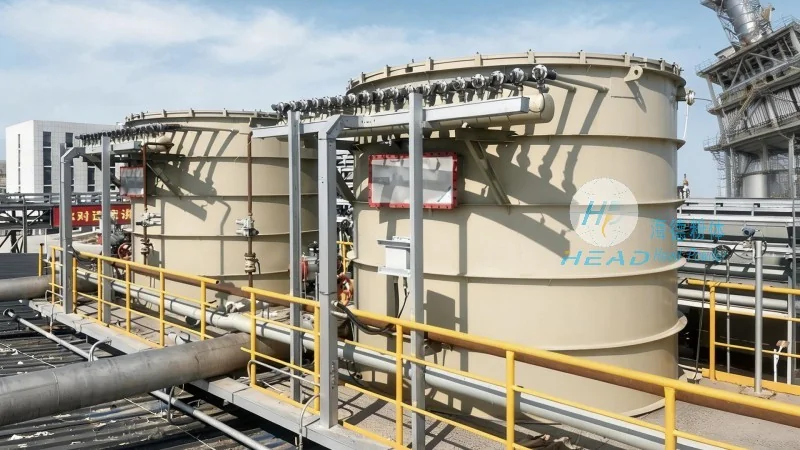
Working Scene Characteristics of Tonne Bag Material Conveying Equipment
The working scene characteristics of tonne bag material conveying equipment are tailored to meet the demands of diverse industrial environments. These systems are commonly deployed in settings such as mining, construction, agriculture, and manufacturing where bulk materials need to be transported over short to medium distances. The equipment is designed to operate in both indoor and outdoor conditions, with weather-resistant components to ensure reliability in various climates. In mining operations, for instance, the equipment efficiently transfers ore from storage bins to processing plants, handling large volumes of materials while maintaining safety standards. In construction sites, it aids in the movement of aggregates, sand, and other construction materials, streamlining the supply chain and reducing material handling costs. The equipment's modular design allows for easy integration into existing production lines, adapting to different workflow requirements. Additionally, the system's ability to handle multiple tonne bags simultaneously enhances throughput, making it suitable for high-volume production environments. The working scene also emphasizes safety, with features like emergency stop buttons, overload protection, and protective guards to prevent accidents and ensure compliance with industrial safety regulations. The equipment's low maintenance requirements and long operational lifespan further contribute to its effectiveness in various working scenarios.
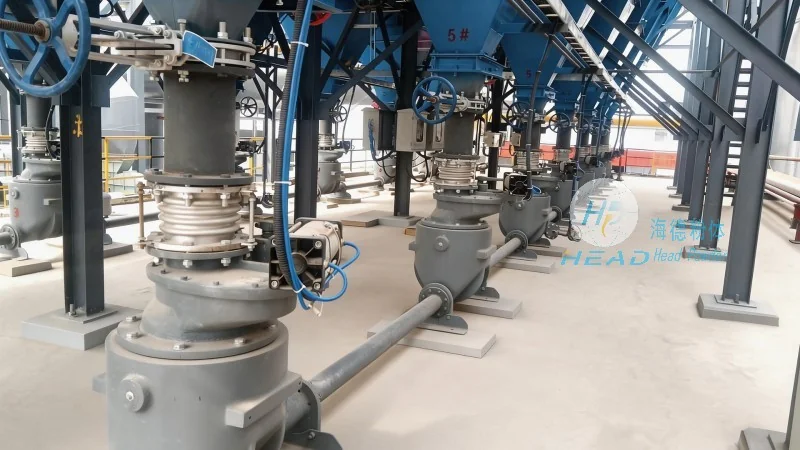
Key Features and Advantages in Practical Applications
When deployed in practical applications, tonne bag material conveying equipment offers several advantages that enhance operational efficiency and cost-effectiveness. One of the primary benefits is the reduction in manual handling, which minimizes the risk of workplace injuries and improves worker safety. The equipment's ability to handle large quantities of material in a single operation significantly increases throughput, leading to higher productivity. Additionally, the system's modular and customizable design allows for adaptation to specific material types and workflow needs, ensuring optimal performance. The use of durable materials and robust construction ensures long-term reliability, reducing downtime and maintenance costs. In terms of energy efficiency, modern designs incorporate variable speed drives and energy-saving mechanisms, lowering operational expenses. The integration of advanced control systems enables precise monitoring and automation, further optimizing the conveying process. These features collectively make tonne bag material conveying equipment a valuable asset in industries where bulk material handling is a critical aspect of operations.
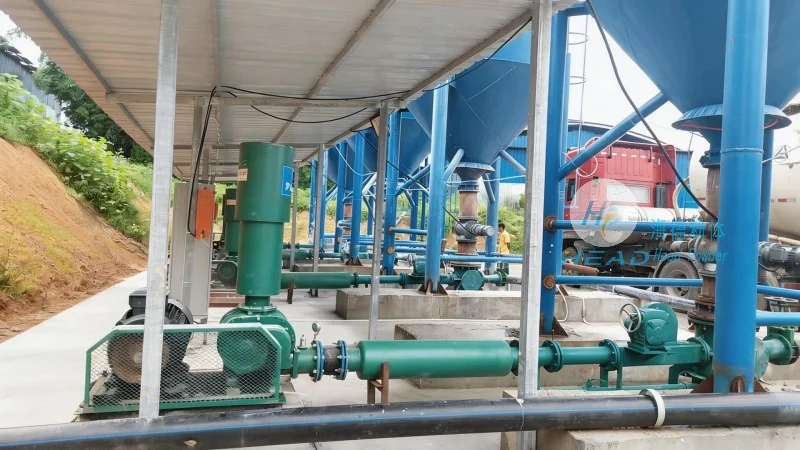
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in the field of material handling technology, providing reliable and efficient tonne bag material conveying equipment tailored to the needs of various industries. The company's commitment to quality, durability, and customer satisfaction is reflected in the design and performance of their products. By understanding the principles and working scene characteristics of this equipment, industries can leverage its benefits to enhance operational efficiency, reduce costs, and improve overall productivity. As a leading manufacturer in China, HeadPowder remains dedicated to delivering advanced solutions that meet the evolving demands of modern industrial applications.