

Introduction to Mobile Powder Handling Systems: Structure and Working Principles
Mobile powder handling systems represent a critical technology in modern industrial processes, particularly for the efficient and safe transportation of bulk powders. These systems are designed to meet the demands of various industries, including pharmaceuticals, chemicals, food processing, and construction materials, where precise and reliable powder movement is essential for operational efficiency and product quality. The development of mobile powder transport solutions has significantly enhanced workflow flexibility and reduced the need for fixed infrastructure, making them a preferred choice for many businesses seeking to optimize their material handling operations.
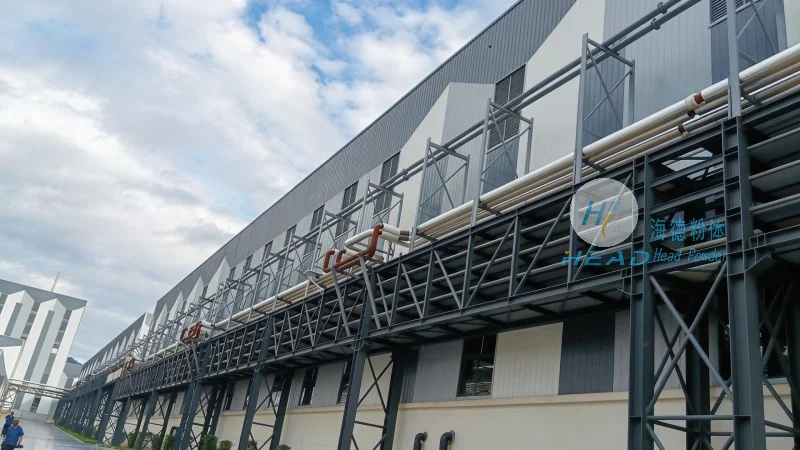
Key Components and Structural Design of Mobile Powder Handling Systems
The structure of a mobile powder handling system typically consists of several integrated components that work in concert to ensure smooth and efficient operation. At the core of these systems is a robust frame or chassis, often built from high-strength materials such as steel or aluminum, to provide durability and stability during transport. This chassis supports the main mechanisms responsible for powder movement, including conveyor belts, screw conveyors, or pneumatic pipelines, depending on the specific application requirements. The design of the system is tailored to accommodate different powder types, particle sizes, and flow characteristics, ensuring optimal performance under various conditions.
A critical component is the feeding mechanism, which may include hoppers or feeders that regulate the flow of powder into the system. These devices are engineered to prevent clogging and ensure consistent material input, which is vital for maintaining system efficiency. The conveying section, whether mechanical or pneumatic, is designed to handle the bulk material with minimal degradation, preserving the integrity of the powder. For example, in pneumatic systems, high-pressure air or gas is used to transport the powder through pipelines, while mechanical systems rely on rotating screws or belts to move the material. The system also incorporates control panels and sensors that monitor operational parameters, such as pressure, flow rate, and temperature, allowing for real-time adjustments and ensuring safety.
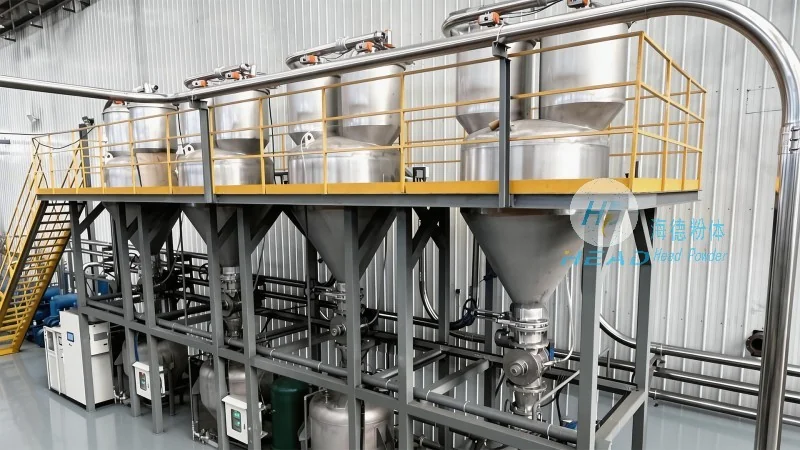
Working Principles of Mobile Powder Handling Systems
The working principles of mobile powder handling systems are based on the physics of powder flow and the mechanics of material transport. The primary goal is to move bulk powders from a source to a destination without compromising the quality or integrity of the material. The process begins with the powder being loaded into a hopper or storage container. From there, the material is transferred to the conveying mechanism, which may involve gravity, mechanical force, or pneumatic pressure to propel the powder forward. In mechanical systems, the screw or belt rotates, creating a continuous motion that pushes the powder along the path. In pneumatic systems, compressed air creates a flow that carries the powder through the pipeline, often with the assistance of cyclones or separators to maintain particle separation and prevent blockages.
The system's control system plays a crucial role in regulating the flow rate and pressure, ensuring that the powder moves at an optimal speed without causing excessive wear or degradation. Sensors are integrated to detect any abnormalities, such as blockages or pressure drops, triggering alerts or automatic shutdowns to prevent system damage or material loss. The mobility aspect of these systems is achieved through a wheeled chassis or a specialized base that allows for easy movement between different locations, making them adaptable to various operational needs. This flexibility is particularly valuable in industries where production sites may change or where multiple processing points are required.
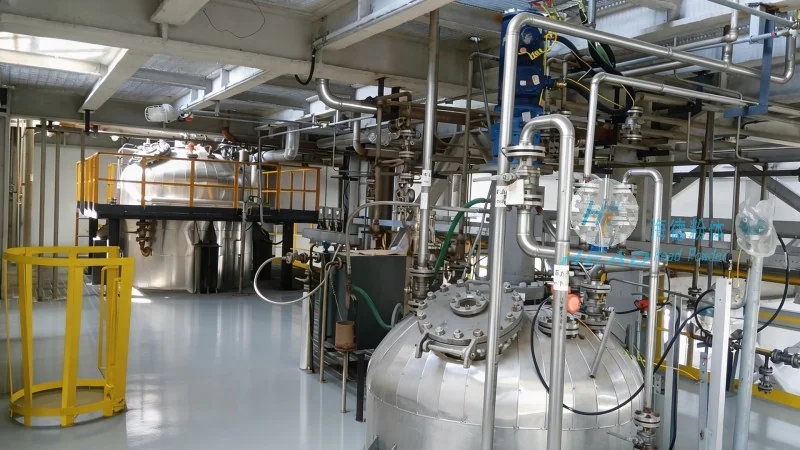
Applications and Benefits of Mobile Powder Handling Systems
Mobile powder handling systems find applications in a wide range of industries, each benefiting from the system's ability to handle bulk materials efficiently and safely. In the pharmaceutical industry, these systems are used to transport raw materials and finished products, ensuring compliance with stringent quality and safety standards. The systems are designed to minimize contamination and maintain the purity of the powders, which is critical for pharmaceutical applications. In the chemical industry, mobile powder transport is essential for handling reactive or hazardous materials, where precise control over flow and pressure is necessary to prevent accidents. The construction materials sector utilizes these systems for transporting cement, sand, and other aggregates, improving on-site material management and reducing labor costs.
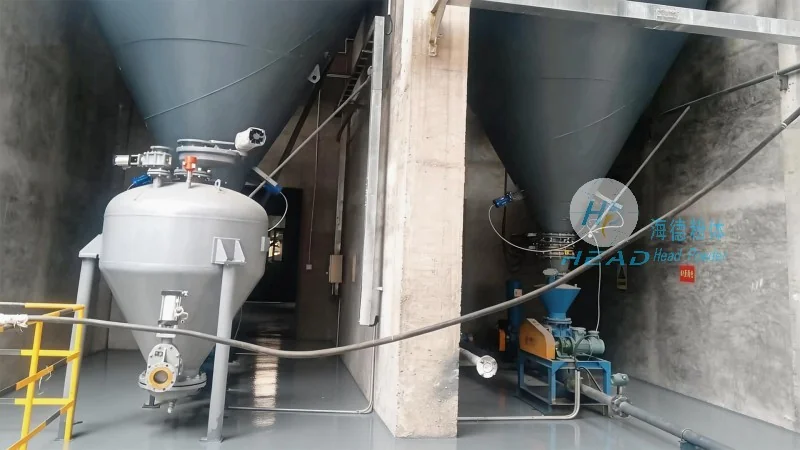
The benefits of mobile powder handling systems extend beyond operational efficiency. These systems enhance safety by reducing the need for manual handling of heavy or hazardous powders, minimizing the risk of workplace injuries. They also improve environmental sustainability by reducing dust emissions and improving material containment, which is increasingly important in today's industrial practices. Additionally, the mobility feature allows businesses to scale their operations without the need for extensive fixed infrastructure, providing a cost-effective solution for growing or changing production needs.
Conclusion and Company Information
Mobile powder handling systems represent a sophisticated and essential technology for modern industrial operations. By integrating robust structural design with advanced control systems, these systems provide reliable and efficient transport of bulk powders. The adaptability and mobility of these solutions make them a valuable asset for businesses across various industries. As the demand for efficient material handling continues to grow, mobile powder handling systems are poised to play an increasingly important role in optimizing industrial processes. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing high-quality mobile powder handling systems tailored to meet the specific needs of their clients. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, offering solutions that enhance operational efficiency and safety. Located in Shandong, China, HeadPowder Engineering Co., Ltd. continues to advance the technology of mobile powder handling, contributing to the growth and development of industries worldwide.