

Long-Distance Pneumatic Conveying System for Yeast
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems, particularly tailored for the efficient and reliable transport of yeast over long distances. With a focus on industrial applications, the company's systems are engineered to meet the unique demands of the yeast processing industry, ensuring optimal performance and minimal product degradation.
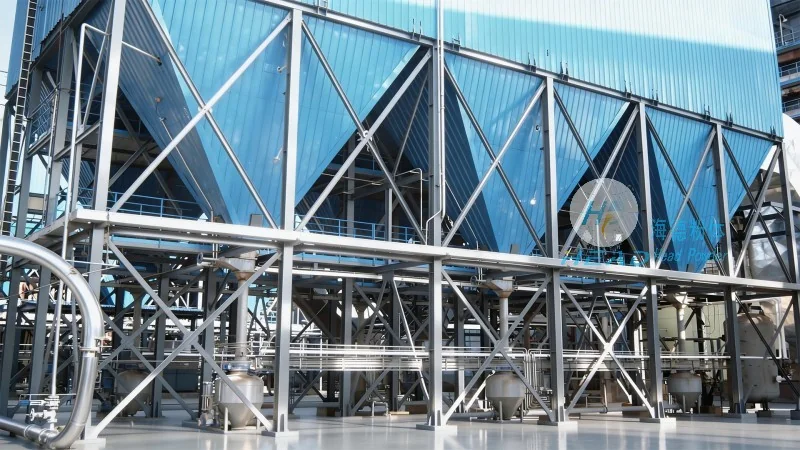
Introduction to Long-Distance Pneumatic Conveying for Yeast
Efficient material handling is crucial in the yeast production and processing sector, where maintaining product quality and operational efficiency are paramount. Traditional conveying methods, such as belt conveyors or bucket elevators, often face challenges when dealing with fine, fragile, or hygroscopic materials like yeast. These challenges include product degradation, dust generation, and operational inefficiencies. To address these issues, HeadPowder has developed a specialized long-distance pneumatic conveying system designed specifically for yeast transport. This system leverages compressed air to move yeast particles through a sealed pipeline network, providing a gentle, dust-free, and highly efficient method of material transport.
Key Features and Advantages of the System
The long-distance pneumatic conveying system for yeast offered by HeadPowder incorporates several key features that enhance its performance and reliability. One of the primary advantages is the ability to handle fragile yeast cells with minimal damage, preserving their viability and quality. The system uses a combination of positive and negative pressure zones to control the flow of yeast, ensuring consistent and controlled movement through the pipeline. This design minimizes the risk of product breakage and reduces the need for additional processing steps to restore product integrity.
Another significant benefit is the system's ability to operate in a dust-free environment. Unlike traditional bulk handling methods, pneumatic conveying systems are enclosed, preventing dust emissions and maintaining a clean working environment. This is particularly important in food processing facilities, where compliance with hygiene and safety regulations is essential. The sealed pipeline design also helps to maintain the moisture content of the yeast, preventing drying or clumping that could affect downstream processing.
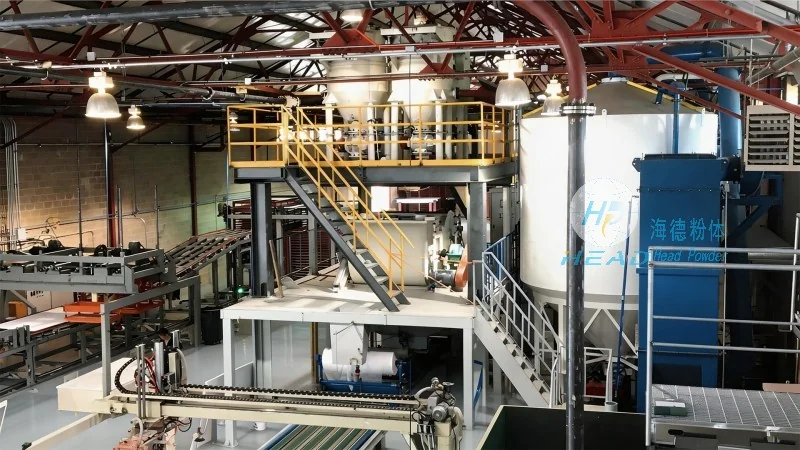
System Components and Design
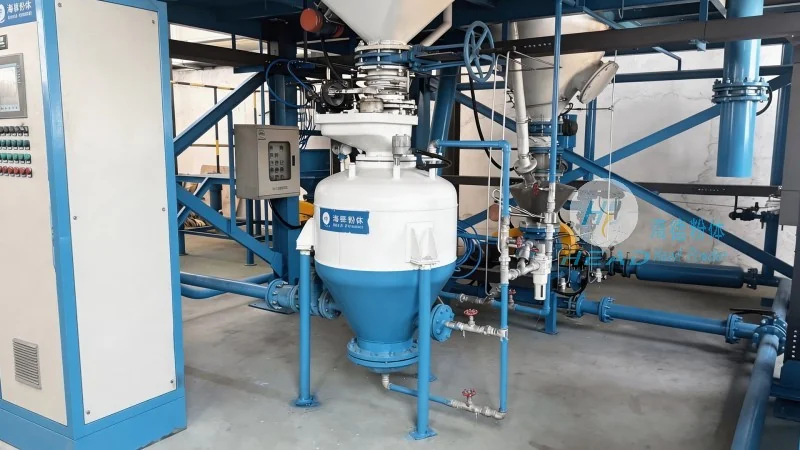
The long-distance pneumatic conveying system consists of several critical components, each designed to work in harmony to ensure optimal performance. The system begins with a hopper or storage silo where the yeast is stored. From there, a rotary valve or feeder controls the flow of yeast into the conveying line. The conveying line itself is typically made of stainless steel or other corrosion-resistant materials, suitable for handling food-grade materials like yeast. The line includes various components such as elbows, bends, and expansion joints to accommodate changes in direction and elevation, ensuring smooth and continuous flow.
At the heart of the system is the air compressor or blower, which generates the necessary pressure to move the yeast through the pipeline. The compressor is equipped with controls to regulate air pressure and flow, allowing for precise adjustment based on the volume and characteristics of the yeast being transported. The system also includes a filter and separator to remove any entrained air or dust from the conveying line, ensuring that the yeast is delivered in a clean and dry state. In addition, the system may include a receiver or discharge hopper at the end of the line, where the yeast is collected and transferred to the next processing stage.
Operational Efficiency and Maintenance
HeadPowder's long-distance pneumatic conveying system is designed for high operational efficiency, with minimal downtime and low maintenance requirements. The use of stainless steel components and advanced materials ensures durability and resistance to corrosion, reducing the need for frequent replacements or repairs. The system's enclosed design also simplifies cleaning and maintenance, as there are no exposed moving parts or areas where product can accumulate. Regular maintenance, such as filter changes and air compressor checks, is typically performed on a scheduled basis, ensuring that the system operates at peak performance.
The system's ability to handle large volumes of yeast over long distances makes it ideal for industrial-scale yeast production facilities. By eliminating the need for multiple transfer points or manual handling, the system reduces labor costs and increases overall productivity. The gentle handling of the yeast also extends the shelf life of the product, reducing waste and improving profitability for the end-user. Additionally, the system's energy efficiency, due to optimized air flow and pressure control, helps to lower operational costs and minimize the environmental impact of the conveying process.
Applications and Industry Impact
The long-distance pneumatic conveying system for yeast is widely used in various industrial applications within the food and beverage industry. It is commonly employed in yeast production plants to transport yeast from storage silos to fermentation tanks or packaging lines. The system is also used in bakeries and breweries to move yeast to production lines, ensuring a consistent and high-quality supply of yeast for baking and brewing processes. In addition, the system is suitable for use in research and development facilities, where precise control over yeast transport is required for experimental purposes.
By providing a reliable and efficient method of yeast transport, HeadPowder's system has a significant impact on the yeast processing industry. It enables manufacturers to improve their operational efficiency, reduce costs, and maintain product quality. The system's ability to handle fragile materials with minimal damage also contributes to the overall sustainability of the industry, as it reduces waste and extends the usable life of the yeast product. Furthermore, the system's compliance with food safety and hygiene standards ensures that it meets the stringent requirements of the food industry, providing peace of mind to manufacturers and consumers alike.