

Long - distance Pneumatic Conveying System for Wheat Starch
Long - distance pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of bulk materials, such as wheat starch, over extended distances. This technology offers significant advantages over traditional mechanical conveying methods, including reduced equipment wear, lower energy consumption, and enhanced safety in handling fine powders. The system's design is tailored to meet the specific requirements of wheat starch, ensuring minimal product degradation and consistent quality throughout the conveying process. Pneumatic conveying systems operate by using air or other gases to transport materials through a pipeline. There are two main types of pneumatic conveying: positive pressure and negative pressure. Positive pressure systems use a blower to force air and material through the pipeline, while negative pressure systems use a vacuum to draw material into the pipeline. For wheat starch, positive pressure systems are often preferred due to their ability to handle high volumes of material and maintain consistent flow rates. The system's components are carefully selected to ensure compatibility with wheat starch, which is a fine, abrasive powder that can be challenging to transport without proper equipment.
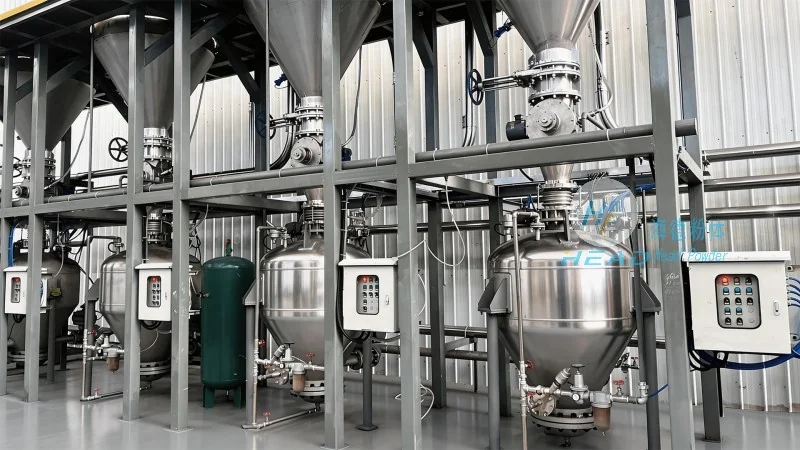
System Overview and Core Components
The long - distance pneumatic conveying system for wheat starch, developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), is engineered to deliver high - performance material transport. The system typically comprises several key components: a material feeding unit, a conveying pipeline network, a pressure - regulating system, and a dust separation and recovery unit. The feeding unit ensures a steady and controlled flow of wheat starch into the pipeline, while the conveying pipeline, often made of high - quality stainless steel or specialized plastic, is designed to withstand the abrasive nature of the starch and maintain hygiene standards. The pressure - regulating system manages the air flow and pressure within the pipeline, optimizing the conveying efficiency and preventing system overloads. The dust separation and recovery unit is crucial for maintaining air quality and recovering valuable starch particles that may have escaped the primary conveying process. Each component is engineered to work in harmony, ensuring a smooth and continuous material flow from the source to the destination.
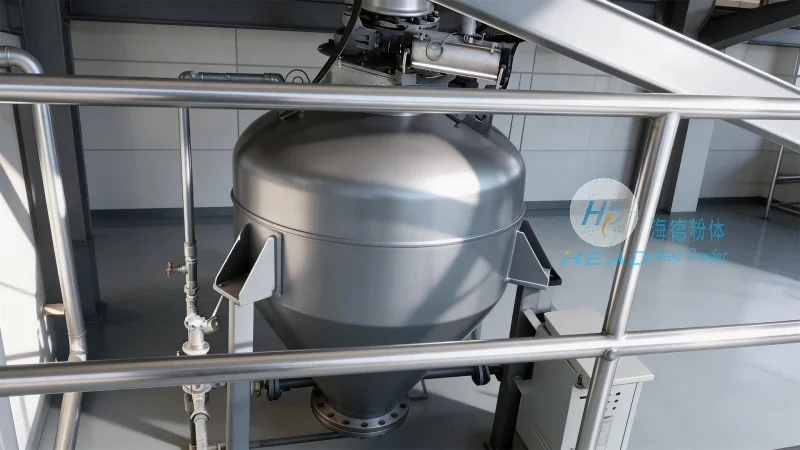
Advantages of Pneumatic Conveying for Wheat Starch
When compared to other conveying methods like belt conveyors or screw conveyors, pneumatic conveying offers several distinct benefits for wheat starch transport. Firstly, it eliminates the need for physical contact between the material and the conveying equipment, which is particularly important for maintaining the purity and quality of wheat starch, especially when it is used in food or pharmaceutical applications. Secondly, the system can handle high volumes of material with minimal operational interruptions, as it is less prone to blockages and can be easily adjusted to accommodate varying production rates. Thirdly, the energy efficiency of pneumatic conveying systems is superior, as they can transport materials over long distances using less power than mechanical systems. Additionally, the system's compact design and flexible pipeline layout allow for easy integration into existing production facilities, reducing installation time and costs. These advantages make pneumatic conveying an ideal choice for industries that require reliable, high - capacity material transport with minimal maintenance.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced material handling solutions, including pneumatic conveying systems. With a strong focus on research and development, the company has built a reputation for delivering high - quality, customized systems that meet the unique needs of its clients. Headpowder's team of experienced engineers and technicians work closely with customers to understand their specific requirements, from material characteristics to operational constraints, and develop tailored solutions that maximize efficiency and minimize downtime. The company adheres to international quality standards and uses advanced manufacturing processes to ensure the reliability and durability of its products. Headpowder's commitment to innovation and customer satisfaction has made it a trusted partner in the material handling industry, serving a wide range of industries including food processing, pharmaceuticals, and chemical manufacturing. The company's headquarters are located in Shandong, China, where it has established a comprehensive production and R&D base.
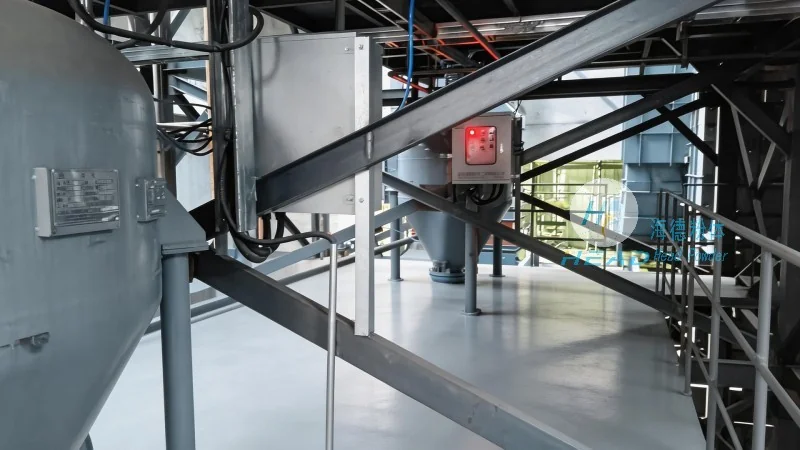
Application Scenarios and Industry Impact
The long - distance pneumatic conveying system for wheat starch is widely used in various industrial applications, particularly in the food and starch processing sectors. In these industries, the system is essential for transporting wheat starch from storage silos to processing plants, or between different stages of the production line, such as from grinding to drying or packaging. The system's ability to handle large volumes of material over long distances makes it ideal for large - scale production facilities, where efficient material flow is critical to maintaining production schedules and meeting market demands. By implementing this system, companies can improve their overall operational efficiency, reduce labor costs, and enhance product quality. The system's flexibility also allows for easy expansion or modification as production needs change, providing a long - term solution for material handling challenges. Many leading wheat starch producers have adopted this system to enhance their production capabilities and ensure consistent product output, demonstrating the system's effectiveness and reliability in real - world applications.