

Long - Distance Pneumatic Conveying System for Sintering Dust
Long - distance pneumatic conveying systems are critical for efficient material handling in industrial applications, particularly in the sintering industry where dust management and material transport over extended distances are essential. The system designed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges by providing a reliable, high - performance solution for transporting sintering dust from source points to processing or disposal facilities. This technology ensures minimal environmental impact while maximizing operational efficiency.
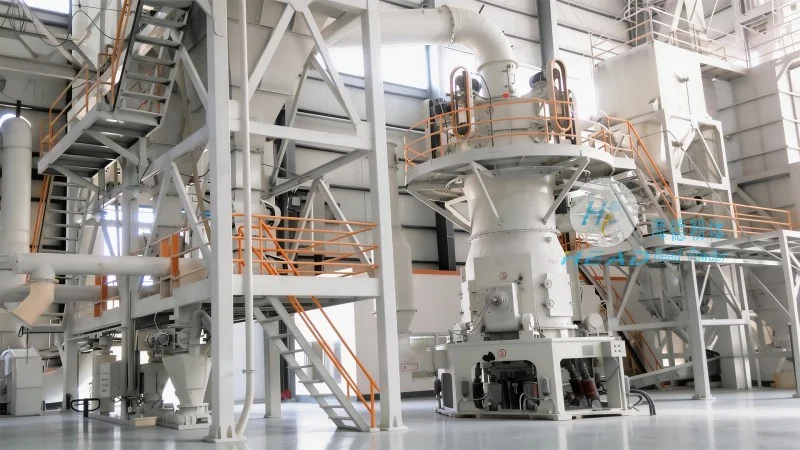
System Overview and Core Components
The long - distance pneumatic conveying system for sintering dust is engineered to handle fine particulate materials with high efficiency. Key components include dust collection hoppers, high - pressure blowers, flexible hoses or pipelines, and material discharge units. The system operates on the principle of air - assisted transport, where compressed air propels the dust particles through the conveying line. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and increasing system reliability. The design incorporates advanced control systems that monitor pressure, flow, and material level in real - time, ensuring optimal performance and preventing system failures.
Advantages of the System
Compared to traditional conveying methods such as belt conveyors or bucket elevators, the pneumatic conveying system offers several distinct advantages. First, it provides a dust - free and enclosed transport process, which significantly reduces environmental pollution and improves workplace safety. The system is also highly flexible, allowing for changes in conveying routes or distances without major structural modifications. Additionally, the low maintenance requirements and long service life of the components contribute to lower operational costs over time. The system's ability to handle fine and abrasive materials without causing wear and tear on components further enhances its durability and efficiency.
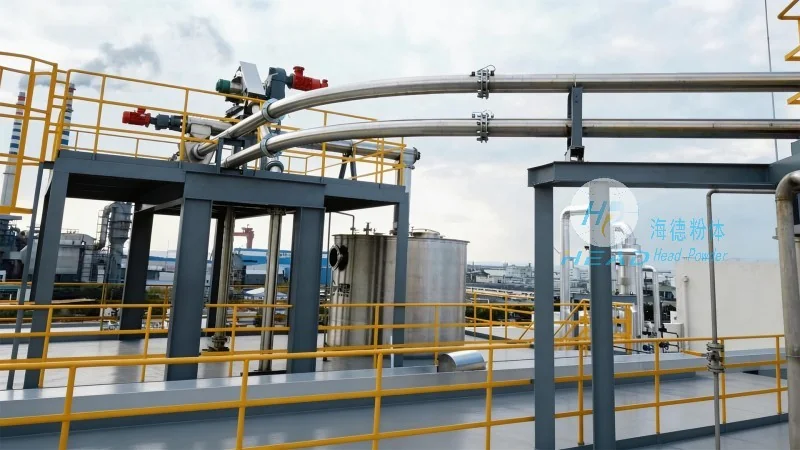
Application in Sintering Industry
In the sintering process, dust is generated during the preparation of raw materials and the operation of sintering furnaces. This dust, if not properly managed, can lead to environmental issues and operational inefficiencies. The long - distance pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is specifically tailored to address these issues by efficiently collecting and transporting the dust from various points in the sintering plant to a central processing or storage facility. The system can handle large volumes of dust over long distances, ensuring that the material is transported without loss or contamination. This not only improves the overall efficiency of the sintering process but also contributes to better environmental compliance and reduced operational costs.
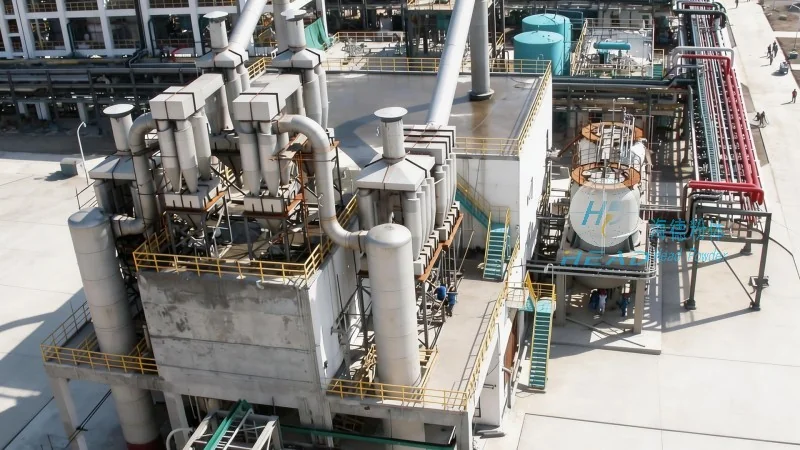
Technical Specifications and Performance
The system is designed to meet the specific requirements of sintering dust handling, with technical specifications tailored to the material properties and conveying distances. The high - pressure blowers used in the system can generate pressures up to 0.8 MPa and flow rates up to 200 m³/h, depending on the application. The conveying lines are typically made of corrosion - resistant materials such as stainless steel or polyurethane, which are suitable for handling abrasive dust particles. The system's efficiency is measured by the conveying distance, material throughput, and pressure drop across the system. Typical performance indicators include the ability to transport dust over distances of up to 1000 meters with a throughput of 10 tons per hour while maintaining a stable pressure and flow rate.
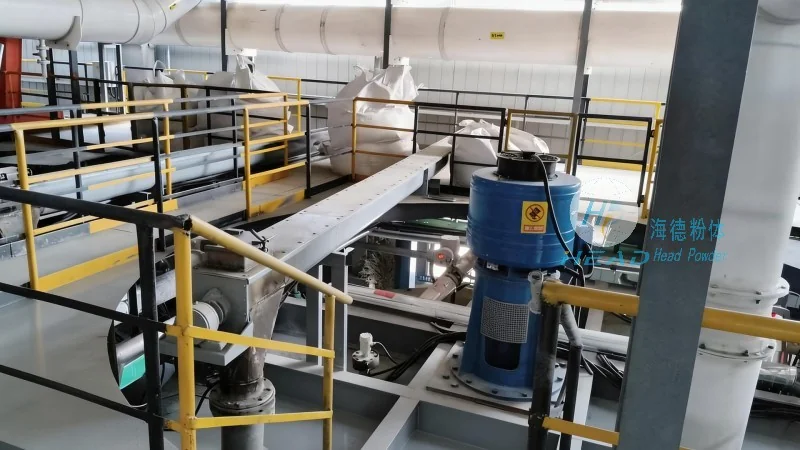
Installation and Maintenance
The installation of the long - distance pneumatic conveying system is straightforward and can be customized to fit the existing infrastructure of the sintering plant. The system components are modular, allowing for easy assembly and disassembly during maintenance or upgrades. Regular maintenance involves checking the blower performance, cleaning the dust collection hoppers, and inspecting the conveying lines for any signs of wear or blockages. The company provides comprehensive maintenance services and spare parts to ensure that the system operates at peak efficiency throughout its service life. The modular design and easy access to components reduce downtime and maintenance costs, making the system a cost - effective solution for long - term use.
Environmental and Safety Benefits
One of the most significant benefits of the pneumatic conveying system is its positive impact on the environment and workplace safety. By enclosing the dust transport process, the system prevents dust emissions into the atmosphere, reducing air pollution and meeting environmental regulations. The enclosed system also protects workers from exposure to fine dust particles, which can cause respiratory issues. Additionally, the system's low noise levels and reduced vibration contribute to a safer and more comfortable working environment. The environmental benefits extend to the reduction of dust - related equipment wear and the need for additional dust control measures, such as baghouses or scrubbers, which can be costly to operate and maintain.