

Wheat Pneumatic Conveying Systems: The Intelligent and Efficient New Era of Wheat Transport
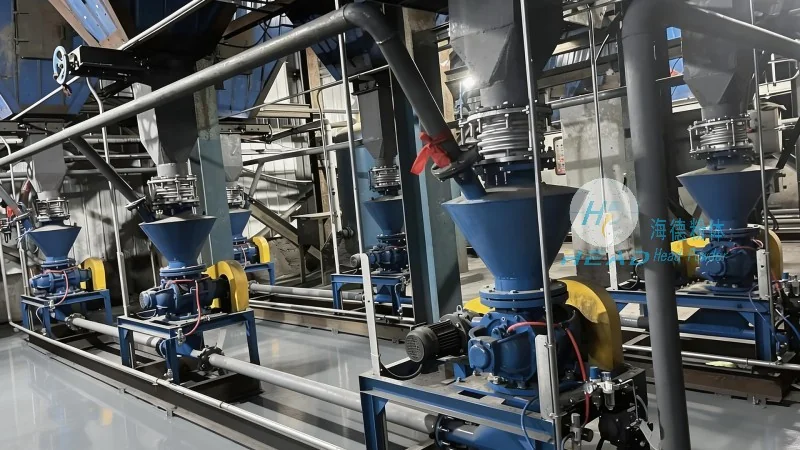
Wheat pneumatic conveying systems represent a sophisticated solution for the efficient and intelligent handling of wheat and other bulk materials. These systems utilize air pressure to transport grains, offering a clean, dust-free, and highly effective method compared to traditional mechanical conveyors. The technology has evolved significantly, making it an essential component in modern grain processing and storage facilities.
Company Overview
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and installation of advanced pneumatic conveying systems. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, reliable equipment tailored to the specific needs of the agricultural and food processing industries. The company's headquarters and primary operations are located in Shandong, China, where it leverages local expertise and resources to serve a global clientele.
Key Features of Wheat Pneumatic Conveying Systems
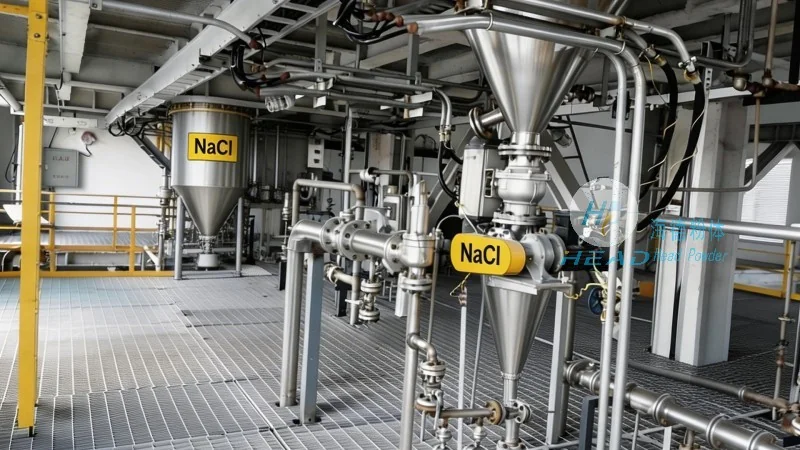
HeadPowder's wheat pneumatic conveying systems are engineered with several key features that enhance performance and operational efficiency. One of the primary advantages is the ability to transport wheat in a closed system, which minimizes contamination and preserves grain quality. The systems are designed to handle various grain types, including wheat, corn, and other cereals, with adjustable air pressure and flow rates to accommodate different material characteristics and processing requirements. Additionally, the equipment is constructed from durable materials, such as stainless steel, to withstand the abrasive nature of grain handling and ensure long-term durability.
Advantages of Using Pneumatic Conveying for Wheat Transport
Implementing a pneumatic conveying system for wheat transport offers numerous benefits for businesses in the agricultural sector. The most significant advantage is the reduction in labor costs and operational time, as the automated system can handle large volumes of grain with minimal human intervention. The closed system design also eliminates the need for manual handling, reducing the risk of product damage and improving workplace safety. Furthermore, the technology is highly versatile, allowing for integration with other processing equipment, such as cleaning, drying, and packaging systems, creating a seamless workflow from reception to final product. Another key benefit is the energy efficiency of pneumatic conveying, as it uses less power compared to traditional belt or bucket elevators, leading to lower operational costs over time.
Customization and Application in Wheat Processing
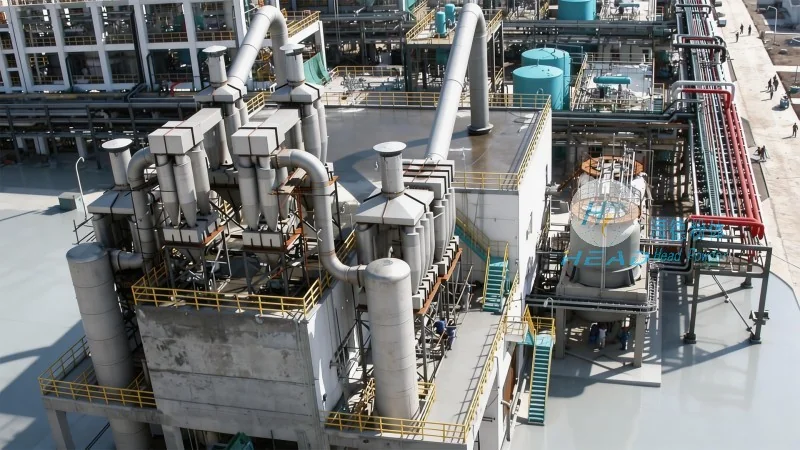
HeadPowder understands that each wheat processing facility has unique requirements, which is why their pneumatic conveying systems are highly customizable. The company works closely with clients to assess their specific needs, including the volume of grain to be transported, the distance of the conveying line, and the desired speed of operation. Based on this assessment, they design and install systems that are optimized for maximum efficiency and minimal downtime. These systems are commonly used in applications such as grain reception, storage, and transfer to milling or packaging lines. The flexibility of the systems allows them to be adapted for both new facility installations and retrofits in existing plants, ensuring that clients can upgrade their operations without major disruptions.
Quality Assurance and After-Sales Support
At HeadPowder, quality is a top priority. The company adheres to strict manufacturing standards and uses advanced technology to ensure that each pneumatic conveying system meets the highest performance criteria. All equipment is rigorously tested before delivery to verify its functionality and durability. Additionally, the company provides comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance. This commitment to customer service ensures that clients can rely on their wheat conveying systems for long-term performance and minimal operational issues. The team of experts at HeadPowder is available to provide guidance and support throughout the entire lifecycle of the equipment, from installation to maintenance and troubleshooting.