

Sodium Dithionite Pneumatic Conveying System: Pioneering the Intelligent and Efficient New Era of So
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for the transportation of sodium dithionite, a critical chemical widely used in various industrial applications. The company, known by the abbreviation "headpowder," is headquartered in Shandong, China, and has established itself as a leading provider of innovative pneumatic conveying systems tailored to the unique requirements of sodium dithionite handling.
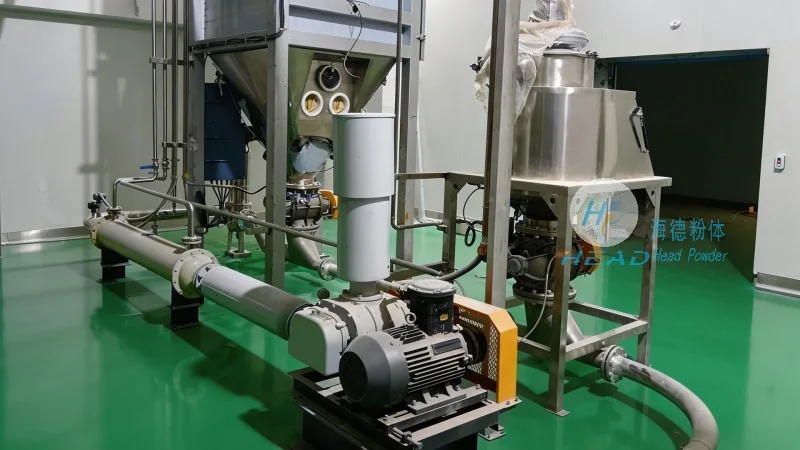
Introducing the Advanced Pneumatic Conveying System for Sodium Dithionite
The company's flagship product, the sodium dithionite pneumatic conveying system, represents a significant advancement in material handling technology. This system is designed to efficiently transport sodium dithionite, a hygroscopic and potentially reactive chemical, with precision and reliability. By leveraging pneumatic conveying principles, the system ensures minimal product degradation, consistent flow rates, and enhanced safety during transportation.
Key Features and Benefits of the Pneumatic Conveying System
One of the primary advantages of this system is its ability to handle the hygroscopic nature of sodium dithionite. The design incorporates moisture-resistant components and sealed conveying lines to prevent moisture absorption, which could otherwise affect the chemical's performance and stability. Additionally, the system features intelligent control mechanisms that optimize air pressure, flow rates, and material feed, ensuring efficient and energy-saving operation. The result is a reliable solution that minimizes downtime and reduces operational costs for industrial clients.
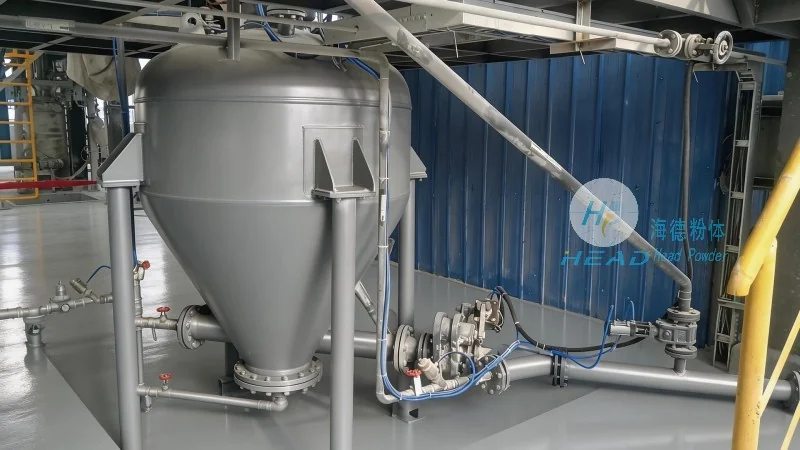
Customization and Adaptability for Diverse Industrial Needs
Recognizing that industrial applications vary widely, Shandong HeadPowder Engineering Co., Ltd. offers customizable solutions for the sodium dithionite pneumatic conveying system. The company works closely with clients to understand their specific processing requirements, such as the scale of operation, the distance of material transport, and the desired level of automation. This approach allows for the development of tailored systems that meet exact specifications, ensuring optimal performance and compatibility with existing industrial setups. Whether for small-scale laboratory use or large-scale industrial production, the system can be adapted to meet diverse needs.
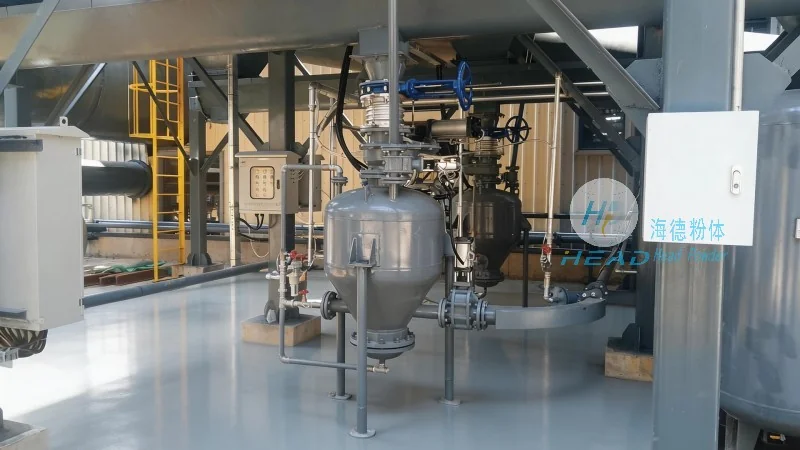
Ensuring Safety and Compliance in Material Handling
Given the potential hazards associated with sodium dithionite, safety is a top priority in the design and operation of the pneumatic conveying system. The system incorporates multiple safety features, including pressure relief valves, emergency shut-off mechanisms, and monitoring systems that track air pressure and material flow. These measures help prevent accidents and ensure compliance with industrial safety regulations. Furthermore, the system is designed to minimize dust generation and exposure, protecting both personnel and the environment. By prioritizing safety, the company ensures that its clients can operate the system with confidence, knowing that their operations are secure and compliant.
Efficiency and Cost-Effectiveness in Industrial Operations
The sodium dithionite pneumatic conveying system is engineered for high efficiency and cost-effectiveness. By eliminating the need for traditional bulk handling methods, such as trucks or conveyor belts, the system reduces transportation time and labor costs. The automated control system minimizes human intervention, leading to consistent performance and reduced operational errors. Additionally, the system's energy-efficient design helps lower long-term operational expenses. For industrial facilities, this translates into improved productivity and a competitive edge in the market. The system's reliability and low maintenance requirements further contribute to its cost-effectiveness, making it a valuable investment for businesses handling sodium dithionite.