

Calcium Carbonate Pneumatic Conveying System: The Intelligent and Efficient New Era of Calcium Carbo
Calcium carbonate, a widely used industrial material, requires efficient and reliable transportation methods to meet the demands of various industries. The traditional methods of handling and transporting calcium carbonate often involve high labor costs, potential material loss, and environmental concerns. To address these challenges, modern pneumatic conveying systems have emerged as a superior solution, offering intelligent and efficient solutions for calcium carbonate transportation.
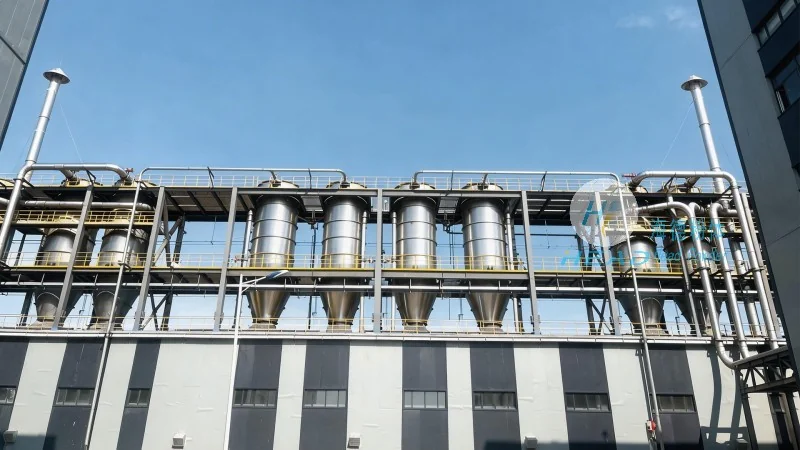
HeadPowder Engineering: Leading the Way in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a prominent player in the field of material handling and processing, specializes in designing and manufacturing advanced pneumatic conveying systems tailored for calcium carbonate applications. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries relying on calcium carbonate as a key raw material.

The Core Components and Advantages of the Pneumatic Conveying System
The calcium carbonate pneumatic conveying system typically consists of several key components, including a material hopper, a rotary airlock valve, a conveying pipeline, a dust collector, and a control system. This integrated system ensures the safe and efficient transfer of calcium carbonate from the storage area to the processing or packaging units. The advantages of this system include reduced labor requirements, minimized material degradation, improved safety standards, and enhanced operational flexibility.
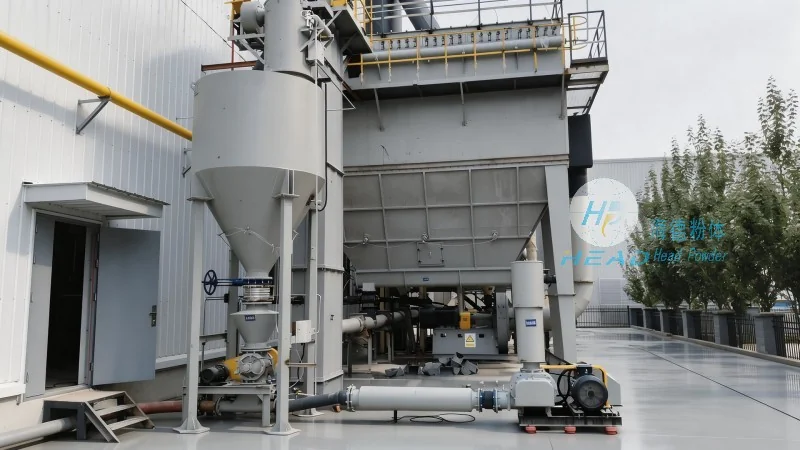
Customization and Application Flexibility
HeadPowder understands that each calcium carbonate application has unique requirements. Therefore, their pneumatic conveying systems are designed with high customization capabilities. Whether the application involves bulk handling, fine powder transport, or long-distance conveying, the system can be tailored to meet specific flow rates, pressure requirements, and environmental conditions. This flexibility ensures optimal performance and cost-effectiveness for different industrial settings.
Efficiency and Reliability in Material Handling
One of the primary benefits of the calcium carbonate pneumatic conveying system is its ability to maintain consistent material flow and minimize downtime. The system’s intelligent control features allow for real-time monitoring and adjustment of conveying parameters, ensuring smooth operation even under varying load conditions. Additionally, the use of high-quality materials and robust construction ensures long-term reliability, reducing maintenance costs and increasing overall productivity.
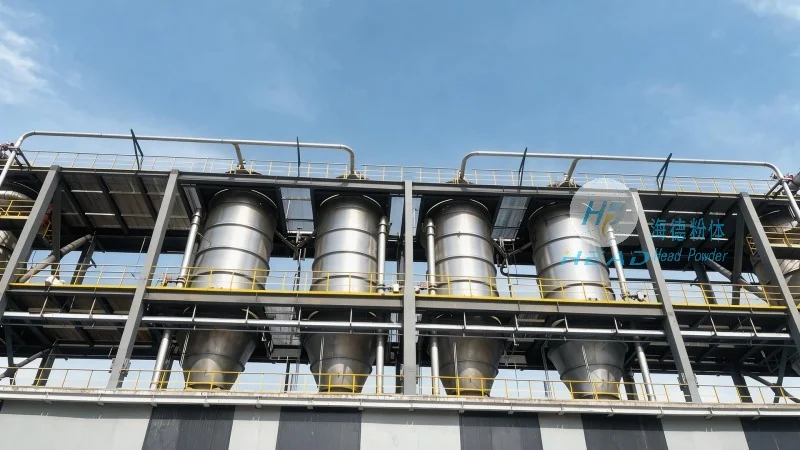
Environmental Considerations and Safety Features
In today’s industrial landscape, environmental sustainability and worker safety are paramount. The calcium carbonate pneumatic conveying system from HeadPowder incorporates advanced dust control measures, such as efficient dust collectors and sealed conveying lines, to minimize airborne particulate emissions and protect the environment. The system also includes safety features like pressure relief valves and emergency shut-off mechanisms, ensuring safe operation and compliance with industry safety standards.