

PFA Pneumatic Conveying System: Pioneering Intelligent and Efficient PFA Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of advanced pneumatic conveying systems tailored for handling polytetrafluoroethylene-co-hexafluoropropylene (PFA) materials. The company's PFA pneumatic conveying system represents a cutting-edge solution that integrates intelligent control technologies with robust engineering to ensure optimal performance in material transport applications.
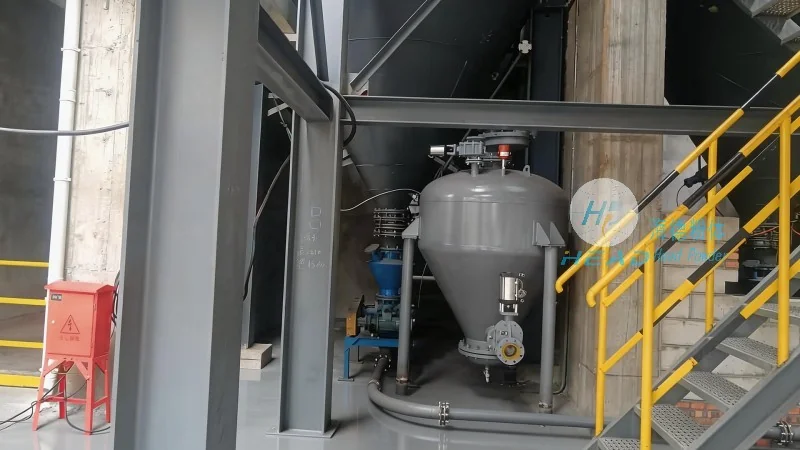
Key Features and Technical Advantages of the PFA Pneumatic Conveying System
The PFA pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is engineered with several key features that enhance its reliability and efficiency. One of the primary advantages is its ability to handle PFA powders and granules with minimal degradation, thanks to the system's low-pressure, low-velocity conveying design. This design reduces material attrition and maintains the integrity of the PFA particles, which is crucial for applications where material quality is paramount. Additionally, the system incorporates advanced filtration and separation components to prevent PFA particles from escaping into the environment, ensuring compliance with environmental regulations and maintaining a clean operational space.
Another significant feature is the intelligent control system integrated into the PFA pneumatic conveying system. This system utilizes real-time monitoring and automation to optimize conveying parameters such as air pressure, flow rate, and material feed speed. The automation capabilities allow for precise control over the material handling process, reducing human error and improving overall operational efficiency. The control system can also be programmed to adapt to varying PFA material characteristics, ensuring consistent performance even with different batch compositions or particle sizes.
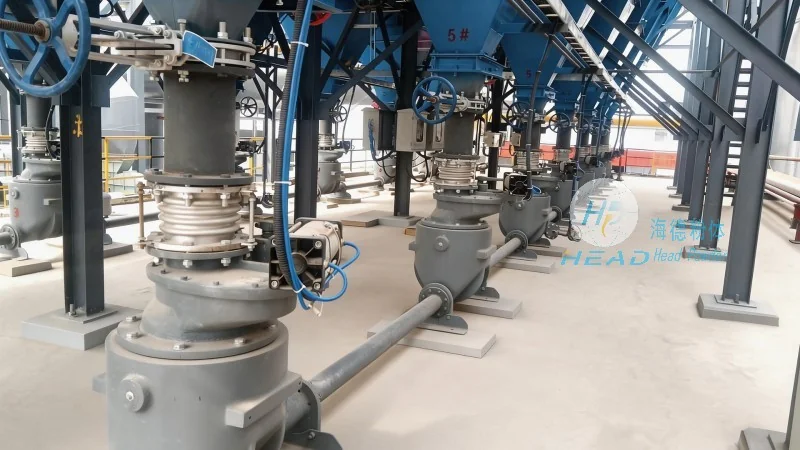
Enhanced Safety and Maintenance Considerations
Safety is a top priority in the design of the PFA pneumatic conveying system. The system incorporates multiple safety features, including pressure relief valves, emergency shut-off mechanisms, and regular maintenance alerts. These features help prevent accidents and ensure that the system operates within safe parameters at all times. Furthermore, the system is constructed with corrosion-resistant materials, such as stainless steel and fluoropolymer components, to withstand the chemical properties of PFA and the associated conveying environment. This durability reduces the need for frequent maintenance and extends the system's service life.
Maintenance of the PFA pneumatic conveying system is designed to be straightforward and efficient. The modular design of the system allows for easy access to components for cleaning, inspection, and replacement. Regular maintenance procedures, including filter changes and system checks, are straightforward and can be performed by trained personnel, minimizing downtime and ensuring continuous operation. The company also provides comprehensive maintenance and support services to its clients, offering technical assistance and spare parts to address any issues that may arise.
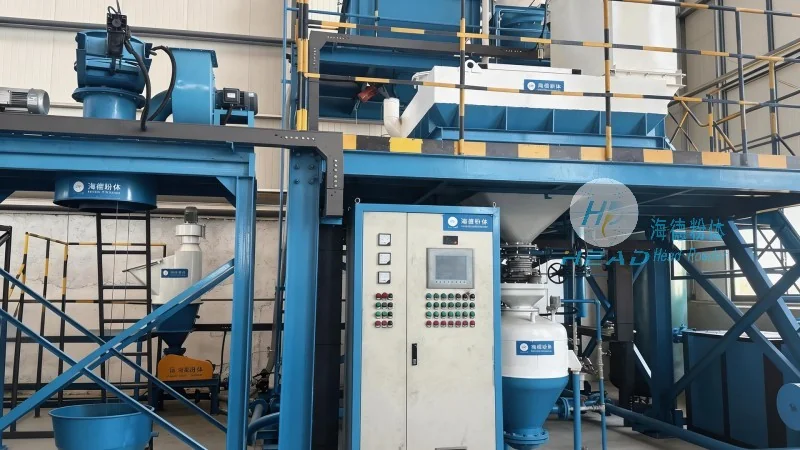
Applications and Industry Benefits
The PFA pneumatic conveying system is suitable for a wide range of applications in industries that rely on PFA materials, including chemical processing, electronics manufacturing, and aerospace. In these industries, the system's ability to handle PFA efficiently and safely is critical. For example, in the electronics industry, PFA is used as a dielectric material in capacitors and other components, and the system ensures that the material is transported without contamination or damage, maintaining product quality. In the aerospace industry, PFA is used in high-performance applications, and the system's reliability ensures that PFA materials are delivered to production lines on time and in optimal condition.
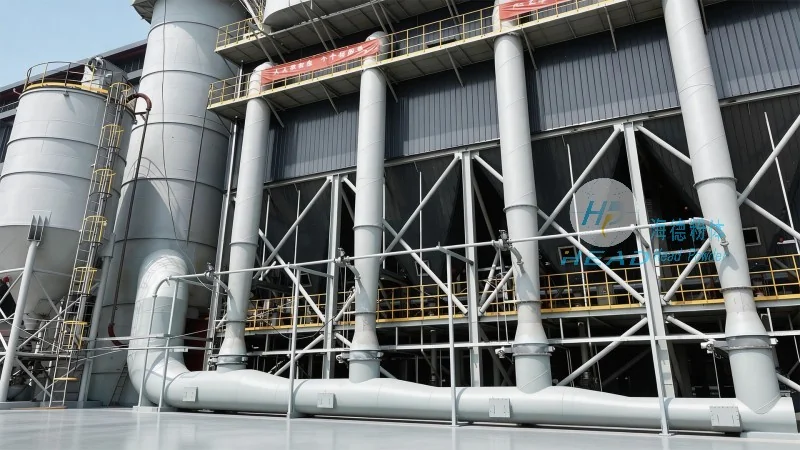
The adoption of the PFA pneumatic conveying system offers several benefits to industries. Firstly, it improves operational efficiency by reducing material handling time and increasing throughput. Secondly, it enhances product quality by minimizing material degradation and contamination. Thirdly, it improves safety by reducing the risk of dust explosions and other hazards associated with PFA handling. Finally, it reduces maintenance costs by extending the system's service life and simplifying maintenance procedures.
Conclusion and Company Commitment
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality PFA pneumatic conveying systems that meet the needs of its clients. The company's expertise in material handling and engineering ensures that the PFA pneumatic conveying system is a reliable and efficient solution for industries that require the transport of PFA materials. By combining advanced technology with robust engineering, the company has developed a system that sets a new standard for PFA material handling, offering intelligent and efficient solutions that enhance operational performance and product quality.