

Design of a Negative Pressure Pneumatic Conveying System for Solid Powders
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design and production of negative pressure pneumatic conveying systems for solid powders. With a focus on precision engineering and customer-specific solutions, the company has established itself as a trusted partner in the field of powder handling technology. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and advanced manufacturing capabilities to deliver high-quality equipment tailored to diverse industrial needs.
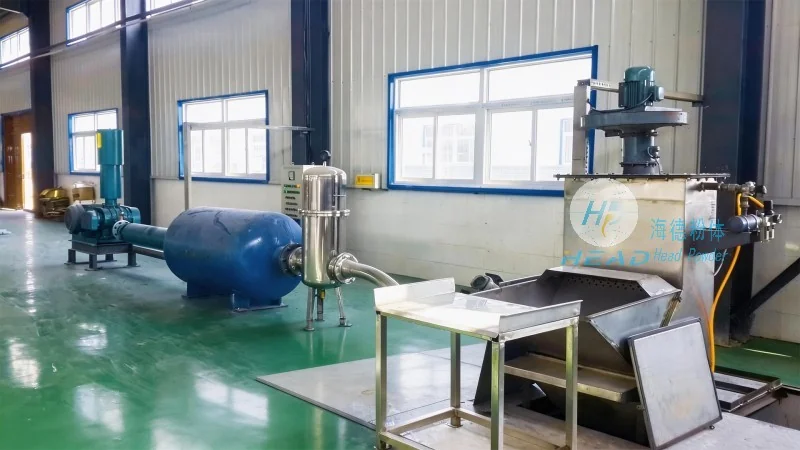
Pneumatic Conveying System for Solid Powders: Core Functionality and Design Principles
The negative pressure pneumatic conveying system for solid powders is engineered to efficiently transport dry, free-flowing powders from one location to another using a combination of air flow and pressure differentials. This technology offers a dust-free, low-maintenance alternative to traditional bulk material handling methods, making it ideal for industries such as food processing, pharmaceuticals, chemicals, and minerals. The system operates by creating a vacuum in the conveying line, which draws the powder from the source container and transports it to the destination point. Key components include a dust collector, a conveying pipeline, a control system, and a discharge unit, all integrated to ensure smooth and reliable operation.
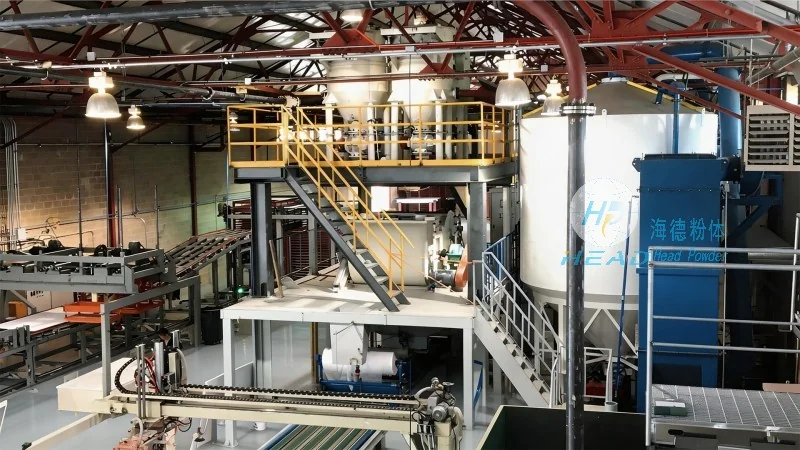
Key Design Considerations for Optimal Performance
When designing a negative pressure pneumatic conveying system for solid powders, several critical factors must be considered to ensure efficiency, safety, and longevity. First, the material properties of the powder—such as particle size, density, and moisture content—play a significant role in determining the appropriate air velocity and pressure drop. HeadPowder engineers conduct thorough material analysis to select the most suitable conveying line diameter and air flow rate. Second, the system's layout and distance between the source and destination points are crucial. Longer conveying distances may require additional booster units or larger pipeline diameters to maintain sufficient air pressure. Third, the inclusion of a dust collection system is essential to prevent environmental contamination and protect equipment from wear. The dust collector is typically equipped with filters that can be cleaned or replaced to maintain optimal performance. Additionally, the control system must be user-friendly, allowing operators to monitor and adjust parameters such as air pressure, flow rate, and conveyor speed in real-time. These design considerations ensure that the system operates at peak efficiency while minimizing downtime and maintenance costs.
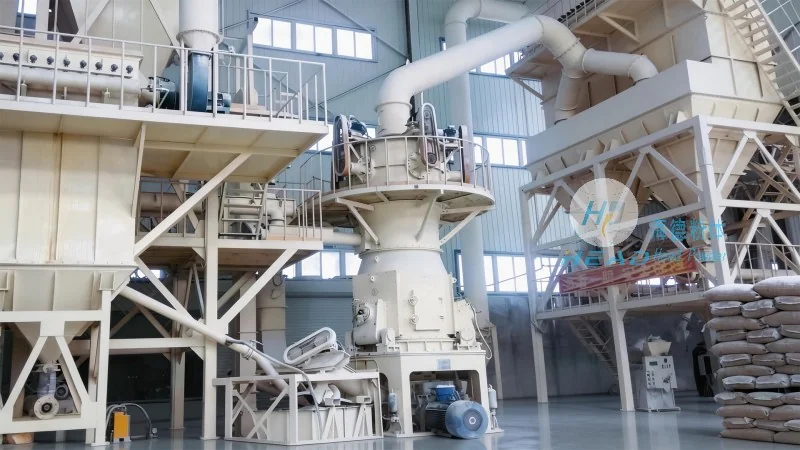
Advantages of Negative Pressure Pneumatic Conveying
Compared to positive pressure systems, negative pressure pneumatic conveying offers several advantages that make it a preferred choice for many industries. One of the primary benefits is its ability to handle powders with high moisture content or those that are prone to caking, as the vacuum environment prevents material buildup in the pipeline. This reduces the risk of blockages and ensures consistent flow. Another advantage is the reduced risk of dust explosions, as the system operates under negative pressure, limiting the release of combustible particles into the atmosphere. Furthermore, negative pressure systems are generally more energy-efficient, as they require less air pressure to transport materials over shorter distances. The compact design of the equipment also allows for easier integration into existing production lines, minimizing installation time and costs. These advantages make the negative pressure pneumatic conveying system a versatile and reliable solution for a wide range of powder handling applications.
Applications in Various Industries
The negative pressure pneumatic conveying system for solid powders is widely used across multiple industries due to its adaptability and efficiency. In the food and beverage industry, it is commonly employed to transport ingredients such as flour, sugar, and spices from storage silos to processing equipment, ensuring a hygienic and dust-free transfer process. The pharmaceutical industry utilizes this technology to handle active pharmaceutical ingredients (APIs) and excipients, where contamination control is paramount. The chemical industry benefits from the system's ability to handle corrosive or hazardous powders, as the enclosed pipeline prevents exposure to personnel and the environment. In the minerals and mining sector, the system is used to transport raw materials such as limestone, coal, and ore from processing plants to storage facilities. Each application requires a customized design, taking into account the specific material characteristics and operational requirements. HeadPowder's team of engineers works closely with clients to develop tailored solutions that meet their unique needs, ensuring optimal performance and compliance with industry standards.
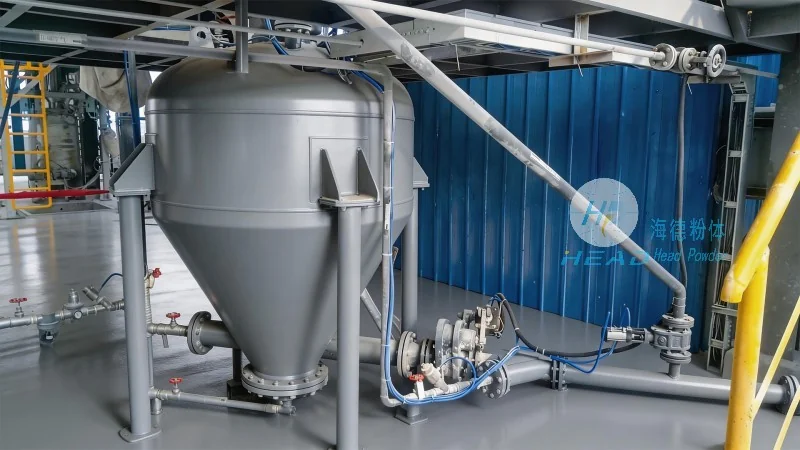
Commitment to Quality and Customer Satisfaction
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality negative pressure pneumatic conveying systems that meet the highest standards of performance and reliability. The company adheres to strict quality control measures throughout the manufacturing process, from material selection to final assembly and testing. Each system undergoes rigorous testing to ensure it meets or exceeds industry specifications before delivery. HeadPowder also provides comprehensive after-sales support, including installation, training, and maintenance services, to ensure the system operates at peak efficiency throughout its lifespan. The company's dedication to customer satisfaction is reflected in its long-term partnerships with clients across various industries. By combining advanced engineering expertise with a customer-centric approach, HeadPowder continues to be a leader in the field of powder handling technology, providing innovative solutions that enhance operational efficiency and safety.