

What is a Feather Powder Conveying System? And What Are Its Design Principles?
Feather powder conveying systems are specialized equipment designed to handle and transport fine powders, such as those derived from feather processing. These systems are crucial in industries where feather-based products are processed, ensuring efficient and reliable material movement. The design principles behind these systems focus on minimizing dust generation, controlling air flow, and maintaining product integrity throughout the conveying process.
Understanding the Core Components of a Feather Powder Conveying System
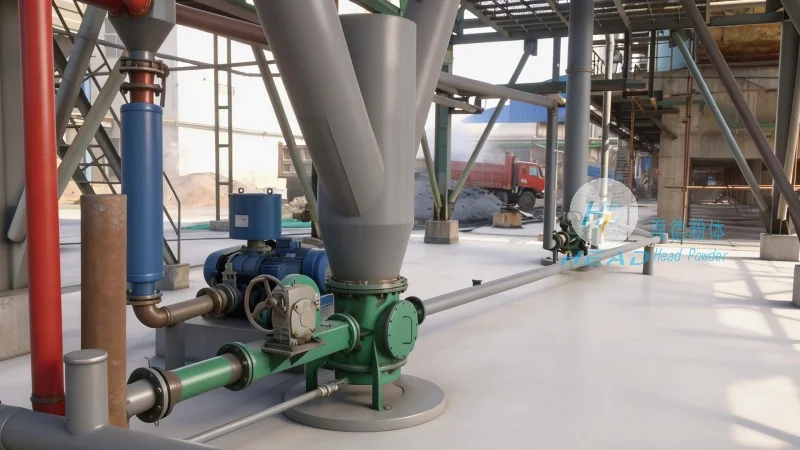
A typical feather powder conveying system comprises several key components that work in tandem to achieve effective material transport. The primary elements include a feeding mechanism, a conveying pipeline, a control unit, and a dust collection system. The feeding mechanism is responsible for introducing the feather powder into the system, often using a hopper or a rotary valve to regulate the flow rate. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, ensures the powder moves from the source to the destination without clogging or degradation. The control unit monitors and adjusts the system's operation, such as air pressure and flow rate, to maintain optimal performance. Finally, the dust collection system captures any airborne particles, protecting the environment and ensuring compliance with industrial regulations.
Design Principles for Efficient Feather Powder Conveying
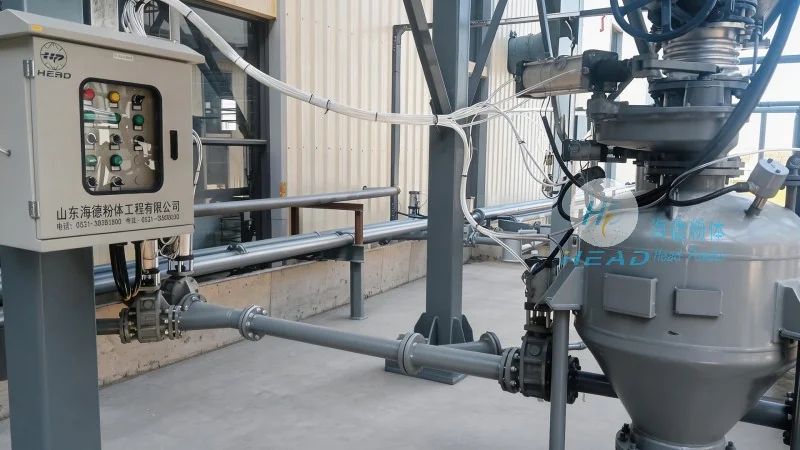
The design of a feather powder conveying system is guided by several critical principles to ensure efficiency, safety, and product quality. One of the most important principles is the minimization of dust generation. This is achieved through the use of enclosed systems and proper sealing of components, which reduces the risk of inhalation and environmental contamination. Another key principle is the control of air flow and pressure. By maintaining consistent air velocity within the pipeline, the system prevents the powder from settling or clogging, ensuring smooth operation. Additionally, the design considers the physical properties of feather powder, such as its fineness and moisture content, to tailor the system's components for optimal performance. For example, the use of flexible hoses or adjustable valves allows for flexibility in handling varying powder characteristics.
How Shandong HeadPowder Engineering Co., Ltd. Enhances Feather Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing advanced feather powder conveying systems tailored to the unique needs of the industry. With a focus on innovation and customer satisfaction, the company leverages years of experience to design systems that meet the highest standards of efficiency and reliability. The company's approach involves a thorough understanding of the client's requirements, from the type of feather powder to the desired conveying distance and capacity. By integrating state-of-the-art technology and materials, HeadPowder ensures that its systems are durable, low-maintenance, and cost-effective. The company's commitment to quality is evident in its adherence to international standards and rigorous testing protocols, which guarantee the performance and safety of its products. Clients benefit from customized solutions that address specific challenges, such as handling fine powders with high moisture content or transporting materials over long distances. The result is a system that not only meets but exceeds industry expectations, providing long-term value and operational efficiency.
Key Advantages of Using a Professional Feather Powder Conveying System
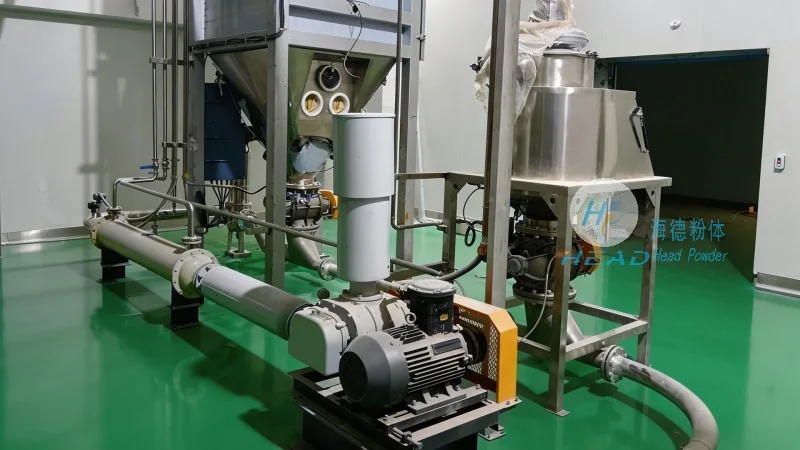
Investing in a professional feather powder conveying system offers numerous advantages for businesses involved in feather processing. One of the primary benefits is improved operational efficiency. By automating the material transport process, companies can reduce labor costs and increase production throughput. The system's ability to handle large volumes of powder consistently ensures that production lines run smoothly without interruptions. Another advantage is enhanced product quality. The enclosed design and controlled air flow prevent contamination and degradation of the feather powder, maintaining its purity and consistency. This is particularly important in industries where the quality of the final product directly impacts market value. Additionally, the system contributes to a safer working environment by minimizing dust exposure and reducing the risk of accidents associated with manual handling of powders. From a cost perspective, the long-term savings from reduced maintenance, lower energy consumption, and improved productivity make the investment highly attractive. The reliability of the system also reduces downtime, ensuring that production schedules are met without delays.