

Working Principle and Features of Sulfate Nickel Powder Handling Systems
For industrial applications involving the transportation and processing of sulfate nickel powder, efficient and reliable handling systems are crucial. This article explores the working principles and key features of such systems, providing insights into their design and operational capabilities. The focus is on understanding how these systems function to ensure safe and effective material handling in various industrial settings.
Working Principle of Sulfate Nickel Powder Conveying Systems
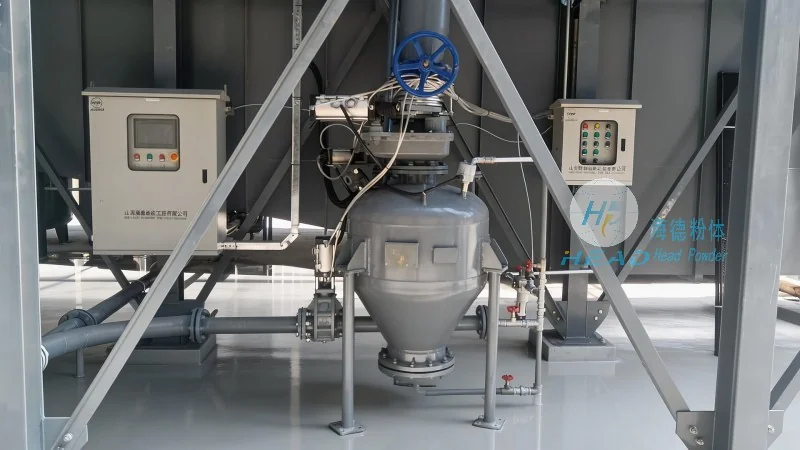
The core working principle of sulfate nickel powder handling systems revolves around the integration of mechanical components designed to move powder from one location to another. These systems typically employ a combination of equipment such as feeders, conveyors, and control mechanisms to manage the flow of material. The process begins with the material being fed into the system, often through a hopper or feeder that regulates the flow rate. From there, the powder is transported via conveyor belts, pneumatic systems, or other conveying methods to the desired destination. Control systems, including sensors and automation, monitor the flow and adjust parameters to maintain optimal performance. This integrated approach ensures consistent and controlled movement of the powder, minimizing issues like clogging or uneven distribution.
The working principle of sulfate nickel powder handling systems is centered on the systematic movement of material through a series of interconnected components. These systems typically start with a feeding mechanism, such as a rotary valve or screw feeder, which controls the initial flow of powder from a storage hopper. The powder then enters a conveying section, which can be either a mechanical conveyor (e.g., belt or chain) or a pneumatic system (e.g., air or vacuum). Mechanical conveyors rely on the physical movement of the material along a path, while pneumatic systems use air pressure to transport the powder through pipes. The choice of conveying method depends on factors like the powder's properties, the distance to be covered, and the required flow rate. Control systems, including PLCs (Programmable Logic Controllers) and sensors, monitor the entire process, adjusting parameters like speed, pressure, or feed rate to maintain consistent performance. This closed-loop control ensures that the system operates efficiently and safely, preventing issues like overloading or material blockages. Additionally, the system may include features like dust collection and filtration to manage airborne particles and maintain a clean working environment.
Key Features of Sulfate Nickel Powder Handling Systems
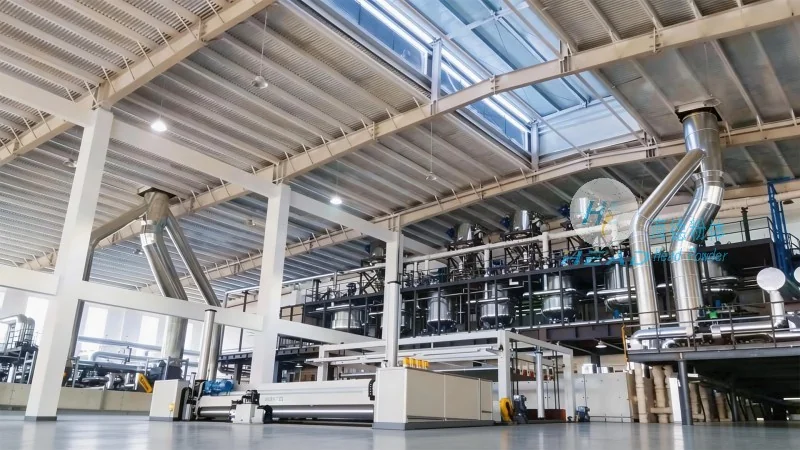
Several key features distinguish effective sulfate nickel powder handling systems, enhancing their performance and reliability. Firstly, the systems are designed with material compatibility in mind, ensuring that the equipment can handle the specific properties of sulfate nickel powder, such as its particle size, moisture content, and flow characteristics. This includes the use of materials like stainless steel or specialized coatings to prevent corrosion and material buildup. Secondly, advanced control technologies are incorporated to provide real-time monitoring and adjustment of the conveying process. Sensors detect variations in flow rate, pressure, or temperature, allowing for immediate corrective actions. Additionally, the systems are equipped with safety features to prevent accidents, such as overload protection and emergency stop mechanisms. Another important feature is the modularity of the design, which allows for easy integration with existing industrial setups and scalability to accommodate varying production needs. These features collectively contribute to the efficiency and safety of sulfate nickel powder handling operations.
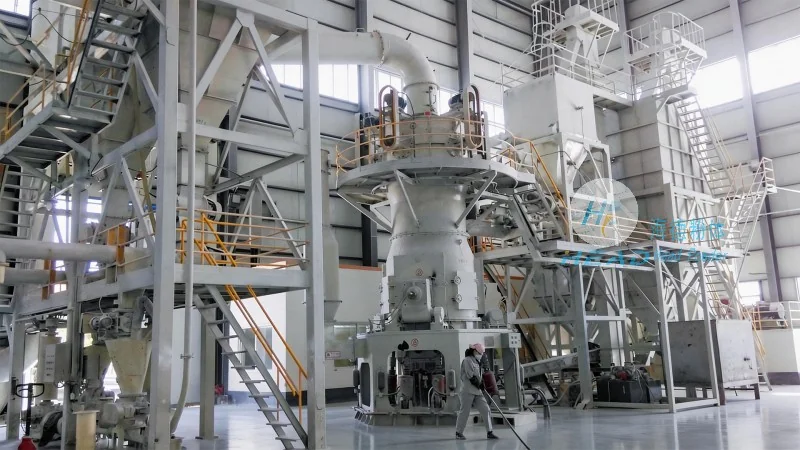
Key features of sulfate nickel powder handling systems include robust construction to withstand the demands of industrial environments. The equipment is often built with corrosion-resistant materials, such as stainless steel, to handle the chemical properties of sulfate nickel and prevent degradation over time. Another critical feature is the integration of advanced automation and monitoring technologies. Sensors and control units provide real-time data on flow rates, pressure, and temperature, enabling operators to make informed decisions and adjust the system as needed. This level of control enhances efficiency and reduces downtime. Safety features are also paramount, with systems incorporating overload protection, emergency stop buttons, and interlocks to prevent accidents. The modularity of the design allows for easy customization and integration with existing production lines, making it adaptable to various industrial applications. Furthermore, the systems are designed for low maintenance, with accessible components and easy-to-replace parts, reducing operational costs and ensuring long-term reliability. These features collectively contribute to the effectiveness and safety of sulfate nickel powder handling operations.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent player in the powder handling industry, specializing in the development and supply of advanced sulfate nickel powder handling systems. Based in Shandong, China, the company has established itself as a leader in providing customized solutions for industrial material handling challenges. With years of experience and a team of skilled engineers, HeadPowder focuses on delivering high-quality, reliable systems that meet the specific needs of its clients. The company’s commitment to innovation is evident in its investment in research and development, which allows it to stay ahead of industry trends and offer cutting-edge technologies. HeadPowder’s systems are designed to enhance productivity, improve safety, and reduce operational costs for businesses dealing with sulfate nickel powder. By prioritizing customer satisfaction and technical excellence, the company has built a strong reputation in the market, serving a wide range of industries including battery manufacturing, chemical processing, and mining. The company’s headquarters in Shandong provides a strategic location for serving clients across China and beyond, with a focus on local and international markets.