

Working Principle and Features of Ammonium Bicarbonate Powder Conveying Line
Ammonium bicarbonate, a widely used chemical in industries such as food processing, pharmaceuticals, and agriculture, requires efficient and reliable handling systems for its transportation. The ammonium bicarbonate powder conveying line is a specialized solution designed to address the unique challenges associated with handling this material. This article explores the working principle and key features of such a system, providing insights into its design, functionality, and practical applications.
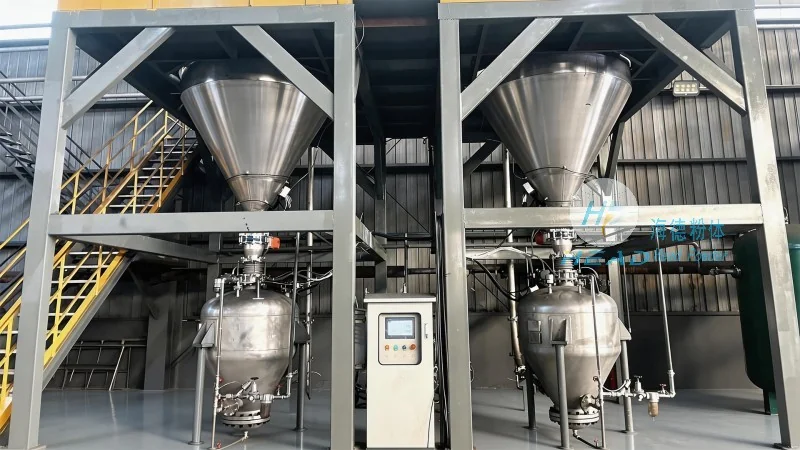
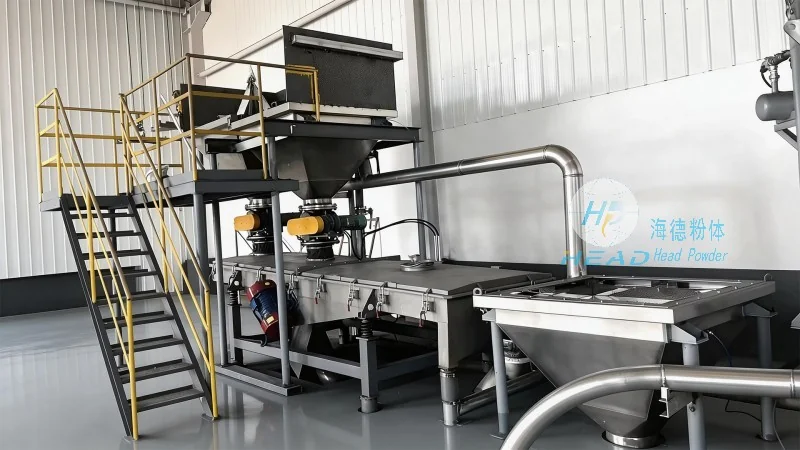
Working Principle of the Ammonium Bicarbonate Powder Conveying Line
The core of the ammonium bicarbonate powder conveying line lies in its ability to transport the material from a source to a destination while maintaining its quality and preventing degradation. The system typically operates through a combination of mechanical components that work in harmony to ensure smooth and continuous flow. One of the primary mechanisms involves the use of a screw conveyor or a pneumatic conveyor, depending on the specific requirements of the application. The screw conveyor, for instance, utilizes a rotating helical screw to move the powder along a closed tube or trough. This method is particularly effective for materials that are free-flowing and non-abrasive, such as ammonium bicarbonate. The screw's rotation creates a positive pressure that pushes the material forward, minimizing the risk of clogging and ensuring consistent throughput. In contrast, pneumatic conveyors use air pressure to transport the powder through a pipeline. This approach is advantageous for materials that are more sensitive to mechanical stress or require a more flexible system. The air pressure creates a negative pressure zone that draws the powder into the pipe, allowing for long-distance transportation without the need for multiple transfer points.
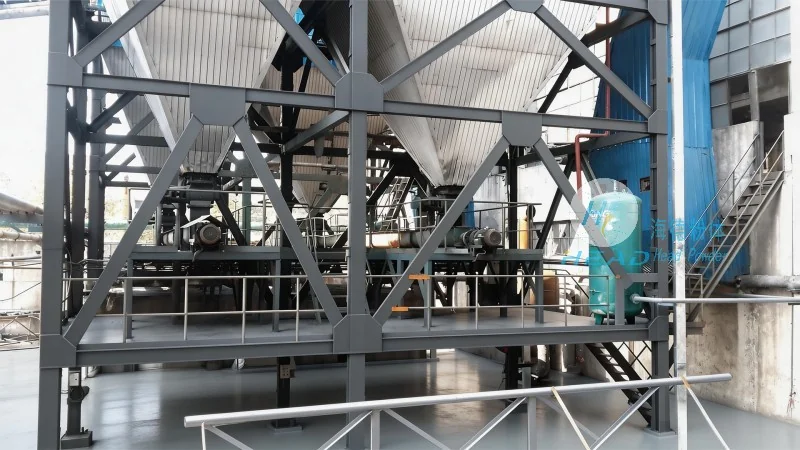
Key Features of the Ammonium Bicarbonate Powder Conveying Line
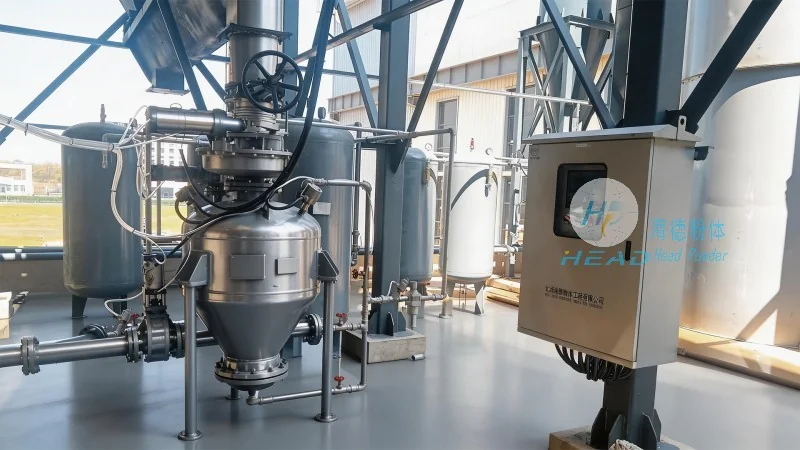
Several critical features distinguish the ammonium bicarbonate powder conveying line from other handling systems. First, the system is designed with corrosion-resistant materials to withstand the chemical properties of ammonium bicarbonate, which can be mildly acidic. The components, including the conveyor tubes, screws, and valves, are often made from stainless steel or other non-reactive metals to prevent contamination and ensure the purity of the material. Second, the system incorporates advanced sealing and dust control mechanisms to maintain a clean and safe working environment. This is crucial for ammonium bicarbonate, as it can be a respiratory irritant if inhaled in large quantities. The use of double-seal or positive pressure systems helps to contain dust and prevent exposure to workers. Third, the conveying line is equipped with monitoring and control systems that allow for real-time tracking of the material flow. Sensors can detect the level of material in the hopper, the speed of the conveyor, and any blockages, enabling operators to take immediate action if issues arise. This feature enhances operational efficiency and reduces downtime. Fourth, the system is designed for easy maintenance and cleaning. The modular design allows for quick disassembly and reassembly of components, facilitating regular cleaning to prevent the buildup of powder residues. This is essential for maintaining the system's performance and extending its lifespan. Finally, the conveying line is scalable, allowing it to be customized to meet the specific needs of different production capacities. Whether for small-scale operations or large industrial plants, the system can be adjusted to handle varying volumes of ammonium bicarbonate, ensuring flexibility and adaptability.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling systems, specializes in providing tailored solutions for various chemical and industrial applications. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses requiring reliable and efficient powder conveying equipment. HeadPowder's team of engineers and technicians leverages years of experience to design and develop systems that meet the unique demands of each client. The company's facilities, located in Shandong, China, are equipped with state-of-the-art technology and stringent quality control measures to ensure that every product meets the highest standards. HeadPowder's dedication to customer satisfaction and technical excellence has earned it a reputation for delivering solutions that not only meet but exceed industry expectations. Whether it's a new installation or an upgrade to an existing system, HeadPowder offers comprehensive support, from initial consultation to after-sales service, ensuring that clients receive the best possible outcome for their powder handling needs.