

Working Principle and Features of Coal Ash Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and production of advanced coal ash powder conveying systems. The company's core product, the coal ash powder conveying system equipment, is engineered to efficiently handle and transport coal ash powder, a byproduct of coal combustion, from various industrial sources to designated disposal or utilization sites. This equipment is crucial for optimizing the handling processes in power plants, cement factories, and other industrial facilities that generate large volumes of coal ash.
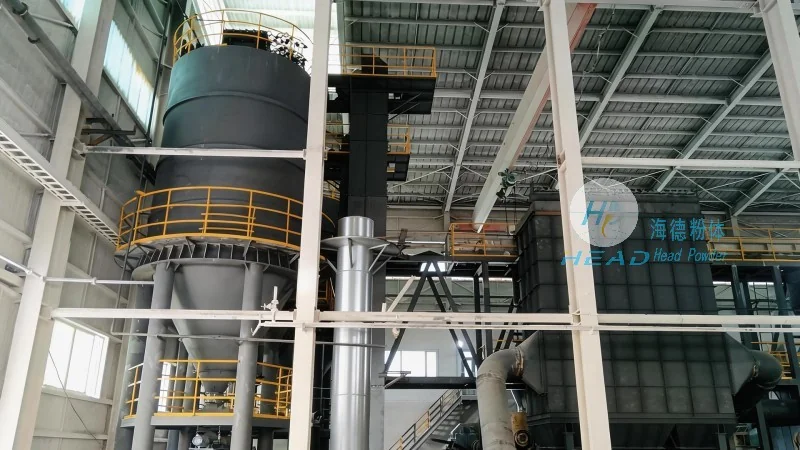
Working Principle of the Coal Ash Powder Conveying System
The coal ash powder conveying system operates on a principle of pneumatic or mechanical transport, depending on the specific design and application requirements. For pneumatic systems, the process typically involves the use of a positive pressure or negative pressure air flow to move the fine coal ash particles through a network of pipes. The system starts with the collection of coal ash from storage silos or hoppers, where it is then fed into a feeding device such as a rotary valve or a screw feeder. The feeder ensures a consistent and controlled flow of the powder into the conveying line. The air, either supplied by a blower or extracted by a vacuum pump, is introduced into the pipeline, creating a flow that carries the ash particles. The velocity of the air is carefully controlled to maintain the ash in a suspended state, preventing clogging and ensuring smooth transport. The conveying line may include bends, vertical sections, and horizontal runs, with appropriate fittings and valves to direct the flow and control the pressure. At the discharge end, the ash is deposited into a receiving hopper or storage tank, where it can be further processed or disposed of. The system also incorporates dust collection and filtration components to ensure environmental compliance and operator safety, as coal ash can be a fine particulate that poses health risks if not properly contained.
Key Features of the Coal Ash Powder Conveying System
The coal ash powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is characterized by several advanced features that enhance its performance, reliability, and efficiency. One of the primary features is its high conveying capacity, which allows for the transport of large volumes of coal ash powder over long distances, typically ranging from several hundred meters to several kilometers. The system is designed with robust materials, such as stainless steel or high-quality carbon steel, to withstand the abrasive nature of coal ash particles and the corrosive effects of moisture or acidic compounds present in the ash. This durability ensures a long service life and minimal maintenance requirements. Another significant feature is the system's flexibility in terms of layout and configuration. It can be customized to fit the specific spatial constraints and operational needs of different industrial sites, with options for both horizontal and vertical transport, as well as complex routing to accommodate multiple discharge points. The control system is equipped with advanced sensors and automation technology, enabling real-time monitoring of pressure, flow rate, and particle concentration. This allows for automatic adjustment of the system parameters to maintain optimal performance and prevent operational issues. Additionally, the system incorporates safety features, including pressure relief valves, emergency shut-off mechanisms, and dust suppression systems, to ensure safe and reliable operation. The energy efficiency of the system is also a notable feature, with optimized air flow and motor control reducing energy consumption compared to traditional conveying methods. The integration of these features makes the coal ash powder conveying system an efficient and reliable solution for handling coal ash in various industrial applications.
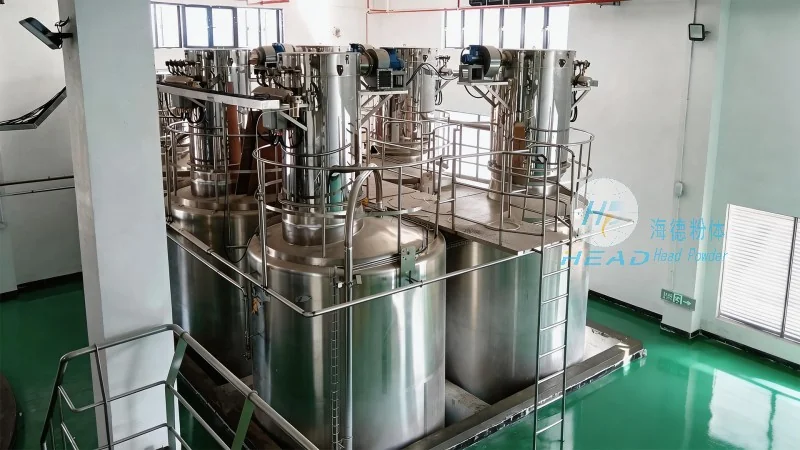
Reliability and Maintenance Considerations
Reliability is a critical aspect of the coal ash powder conveying system, as downtime can lead to significant operational disruptions and increased costs. Shandong HeadPowder Engineering Co., Ltd. employs rigorous quality control measures during the manufacturing process to ensure that all components meet or exceed industry standards. The system's design incorporates redundant components and fail-safe mechanisms to minimize the risk of failure. For example, the feeding devices are equipped with overload protection to prevent damage from excessive material input, and the conveying lines are fitted with pressure sensors to detect blockages or leaks. Regular maintenance is essential to maintain the system's performance and longevity. The company provides comprehensive maintenance services, including routine inspections, component replacement, and troubleshooting support. The use of high-quality materials and precision manufacturing reduces the frequency of maintenance, but periodic checks of the air filtration system, valve operation, and motor performance are recommended to ensure consistent operation. By adhering to a regular maintenance schedule, users can extend the service life of the equipment and maintain its efficiency and reliability.
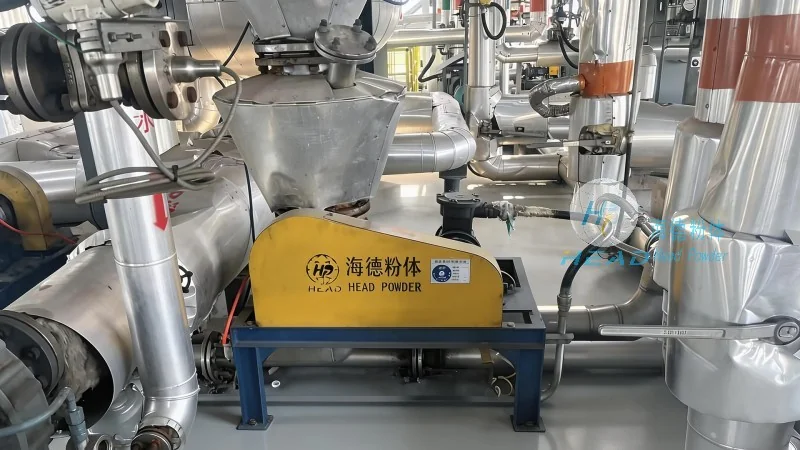
Environmental and Safety Compliance
Environmental and safety compliance are paramount in the design and operation of the coal ash powder conveying system. Coal ash is a fine particulate that can be harmful if inhaled or if it contaminates the environment. The system is equipped with dust collection and filtration systems that capture and neutralize the fine particles, preventing their release into the atmosphere. The filtration units typically use high-efficiency particulate air (HEPA) filters or baghouse filters to ensure that the exhaust air meets environmental regulations. Additionally, the system incorporates safety features to protect operators from potential hazards. The feeding and conveying equipment is enclosed to prevent exposure to dust and moving parts, and emergency stop buttons are strategically placed for quick response in case of an incident. The control system includes interlocks that prevent the system from operating if safety devices are activated, ensuring that operators can safely shut down the equipment when needed. Compliance with local and national environmental regulations is a key consideration, and the system is designed to meet or exceed these standards. The company also provides documentation and certifications to verify that the equipment complies with relevant safety and environmental codes, giving users confidence in its operation.
Customization and Application Flexibility
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial facility has unique requirements, and the coal ash powder conveying system is designed to be highly customizable to meet these needs. The system can be tailored in terms of capacity, length, and configuration to fit the specific layout of the facility. For example, in power plants, the system may need to transport ash from multiple boilers to a central storage area, requiring a network of interconnected pipelines. In cement factories, the system may need to handle ash from different sources and direct it to various processing units. The company's engineering team works closely with clients to assess their operational needs and design a system that optimizes the handling process. The customization options also include the choice of transport method, with pneumatic systems being suitable for long-distance transport and mechanical systems (such as screw conveyors or bucket elevators) being preferred for shorter distances or when the ash contains larger particles. The control system can be integrated with existing plant systems, allowing for seamless operation and data sharing. This flexibility ensures that the coal ash powder conveying system can be adapted to a wide range of industrial applications, from small-scale facilities to large-scale power plants.