

Principle and Working Scene Characteristics of Dilute Phase Powder Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. This article focuses on the principle and working scene characteristics of dilute phase powder pneumatic conveying lines, which are widely used in various industrial applications for efficient material transport.
Understanding Dilute Phase Pneumatic Conveying
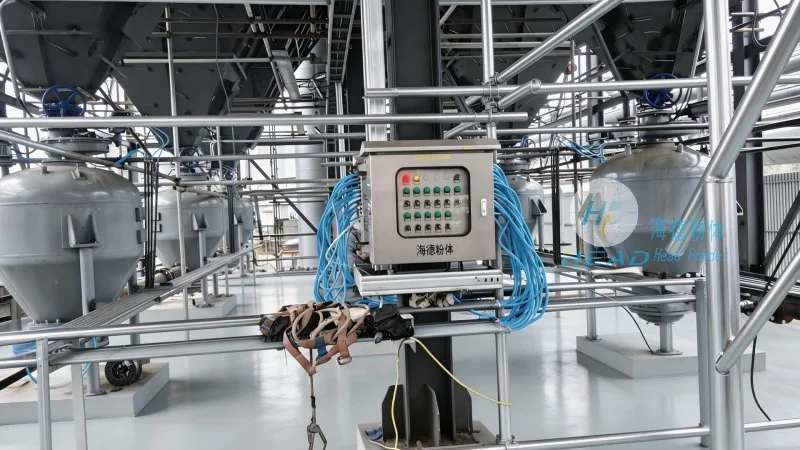
Dilute phase pneumatic conveying systems operate by transporting bulk materials, such as powders and granules, in a low concentration within the conveying air. The core principle involves creating a high-velocity air stream that suspends the particles, allowing them to be carried through pipelines to the destination. This method is distinct from dense phase systems, where materials are conveyed in a more compacted state, typically using lower air velocities and higher pressure differentials.
Key Working Principles
The fundamental principle of dilute phase pneumatic conveying is the balance between air velocity and particle size. For effective transport, the air velocity must exceed the terminal velocity of the particles, ensuring they remain suspended and move smoothly through the system. The system typically includes a blower or compressor to generate the necessary air pressure, a hopper or feeder to introduce the material, and a pipeline network that directs the flow to the receiving point. The process is often controlled by sensors and automation to maintain consistent flow rates and prevent blockages.
Common Working Scene Characteristics
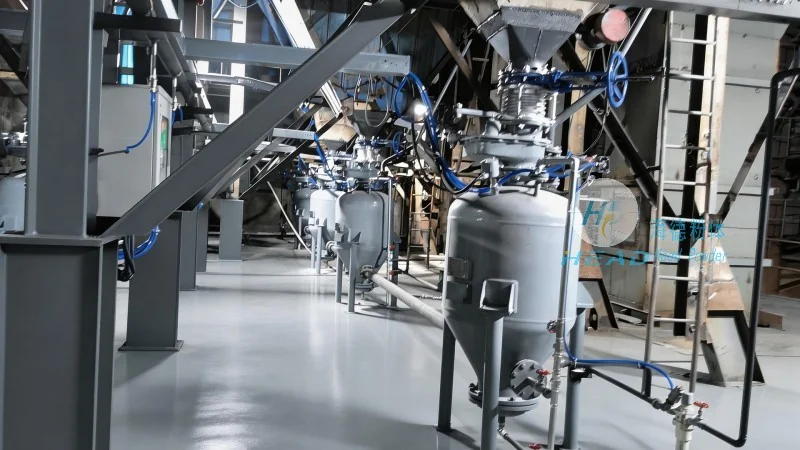
Dilute phase systems are particularly suitable for applications requiring long-distance transport, high throughput, and minimal material degradation. They are commonly used in industries like pharmaceuticals, food processing, chemical manufacturing, and mining, where materials need to be moved from production areas to storage or processing units without significant loss or contamination. The working scene characteristics include:
Long-Distance Transport Efficiency
One of the primary advantages of dilute phase systems is their ability to transport materials over considerable distances with minimal energy consumption compared to other methods like trucking or conveyor belts. The high air velocity ensures that particles are kept in suspension, reducing friction and wear on the pipeline, which extends the system's operational life.
High Throughput and Flexibility
These systems are designed to handle high volumes of material, making them ideal for continuous production processes. The flexibility of the pipeline network allows for easy reconfiguration of the system to accommodate changes in production schedules or material types. This adaptability is crucial in dynamic industrial environments where operational changes are frequent.
Reduced Material Degradation
By maintaining a low concentration of particles in the air stream, dilute phase systems minimize the risk of material degradation due to friction, impact, or exposure to air. This is especially important for sensitive materials like pharmaceutical powders or food products, where quality and purity are paramount. The gentle handling ensures that the material's properties remain intact throughout the conveying process.
Low Maintenance Requirements
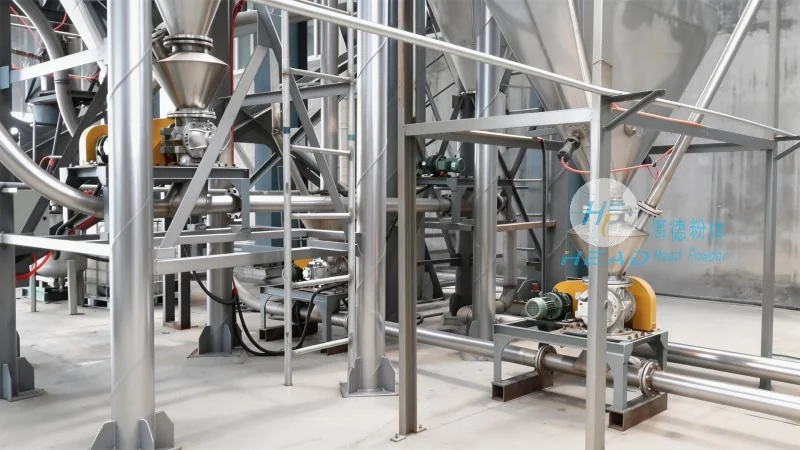
Compared to other bulk material handling systems, dilute phase pneumatic conveying lines generally require less maintenance. The absence of moving parts in the pipeline (except for the blower and feeder) reduces the likelihood of mechanical failures. Regular inspections and cleaning of the system components, such as filters and hoppers, are typically sufficient to maintain optimal performance.
Application Examples
HeadPowder has successfully implemented dilute phase pneumatic conveying systems in various industrial settings. For instance, in a pharmaceutical manufacturing facility, the system was used to transport active pharmaceutical ingredients (APIs) from a production line to a packaging unit, ensuring a clean and efficient process. In a food processing plant, the system conveyed flour and sugar to different processing stages, maintaining the quality and freshness of the ingredients. These applications highlight the versatility and effectiveness of dilute phase systems in handling diverse materials under different operational conditions.
Conclusion
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides comprehensive solutions for dilute phase powder pneumatic conveying systems. By leveraging advanced engineering principles and tailored system designs, the company ensures that clients achieve efficient, reliable, and cost-effective material transport solutions. The working scene characteristics of these systems, including long-distance transport, high throughput, and minimal material degradation, make them a preferred choice for modern industrial applications. As a trusted partner in the engineering sector, HeadPowder continues to innovate and deliver high-quality pneumatic conveying systems that meet the evolving needs of various industries.