

Introduction to the Metering Bin Pump Powder Conveying System: Structure and Working Principle Expla
This article provides an overview of the metering bin pump powder conveying system, a key equipment used in the powder handling industry. The system is designed to efficiently transport bulk powders over long distances with high precision and reliability. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, this system integrates advanced technology to meet the demands of various industrial applications, including chemical, pharmaceutical, and food processing sectors.
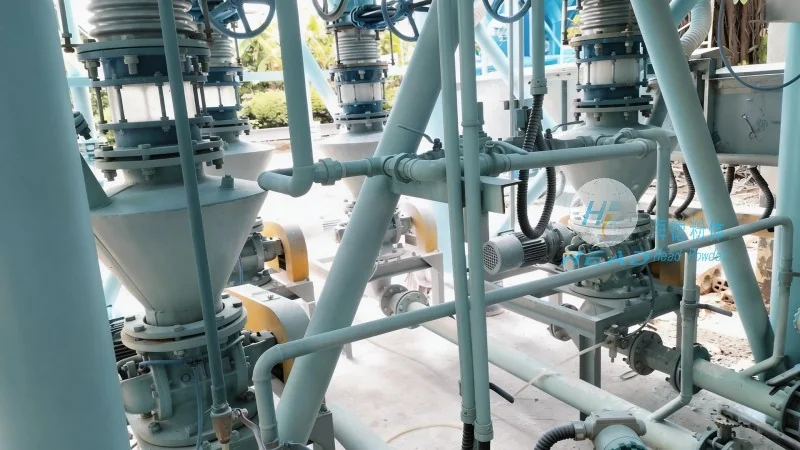
The core component of the metering bin pump is the bin pump itself, which operates on the principle of air pressure to move powders. The system typically consists of a storage bin, a metering device, a pump chamber, and a discharge valve. The storage bin holds the bulk powder, while the metering device ensures an accurate quantity is fed into the pump chamber. As the pump chamber is sealed and pressurized, the powder is forced through the discharge line to the destination. This process allows for precise control over the flow rate and volume of the conveyed material, making it ideal for applications requiring consistent and controlled powder delivery.
One of the key advantages of the metering bin pump system is its ability to handle a wide range of powder characteristics, from fine powders to bulkier materials. The system's design accommodates different particle sizes and flow properties, ensuring smooth and efficient operation. The metering mechanism, often a rotary valve or a screw feeder, regulates the amount of powder entering the pump, preventing overloading and maintaining consistent pressure within the system. This precision is crucial for industries where material consistency directly impacts product quality, such as in pharmaceutical manufacturing where uniform dosage is essential.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced powder handling systems. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. The metering bin pump system is a testament to their expertise, combining robust engineering with user-friendly operation. The company's facilities in Shandong, China, are equipped with state-of-the-art technology and skilled personnel to ensure high-quality production and reliable after-sales support. Clients benefit from the company's commitment to providing tailored solutions that meet specific operational requirements, enhancing overall process efficiency and reducing downtime.
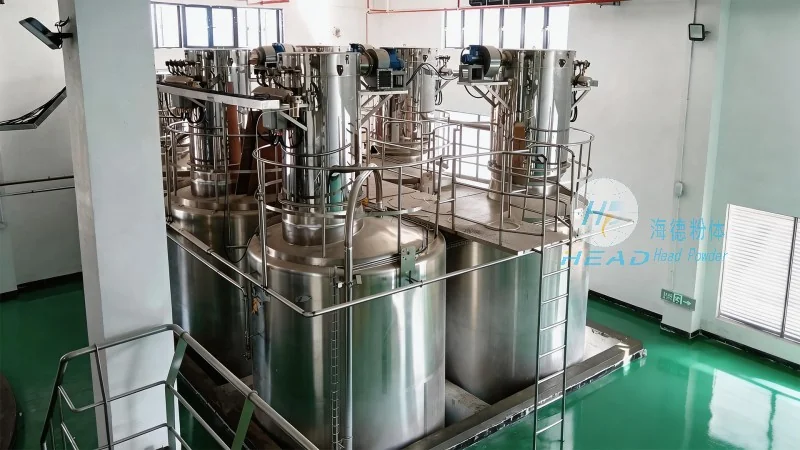
The system's structure includes several critical components that work in harmony to achieve optimal performance. The storage bin is typically made of durable materials like stainless steel or carbon steel, ensuring resistance to corrosion and wear from the conveyed powders. The bin is equipped with a hopper and a discharge port, allowing for easy loading and unloading of materials. The metering device, positioned at the bottom of the bin, controls the flow of powder into the pump chamber. This component is designed to minimize material buildup and prevent clogging, which can occur with certain types of powders. The pump chamber, a sealed vessel, is pressurized using compressed air or other gases, creating the force needed to transport the powder through the discharge line. The discharge valve, located at the end of the line, regulates the flow of the material to the final destination, ensuring a controlled and steady output.
The working principle of the metering bin pump involves a sequence of steps that ensure efficient and accurate powder transport. First, the powder is loaded into the storage bin. The metering device then measures and feeds a precise amount of powder into the pump chamber. As the chamber is pressurized, the powder is pushed through the discharge line. The pressure is maintained until the desired volume is delivered, after which the system resets and prepares for the next cycle. This cyclic operation allows for continuous operation while maintaining consistent flow rates. The system's control system, often integrated with sensors and automation, monitors key parameters such as pressure, flow rate, and level, providing real-time feedback and adjustments to maintain optimal performance.
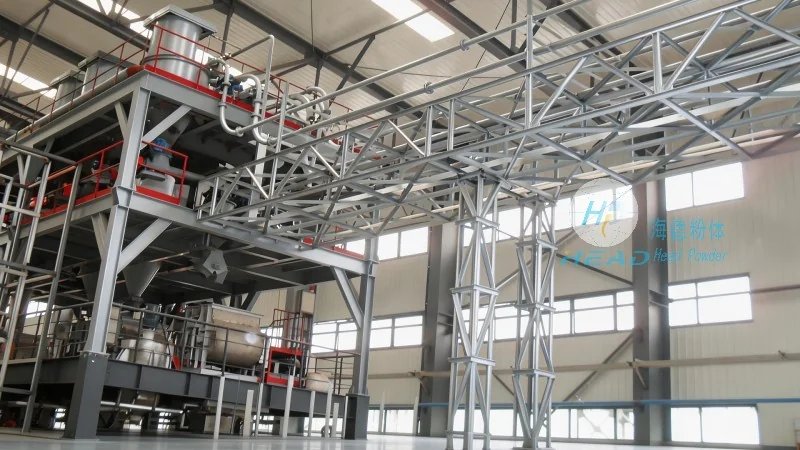
Applications of the metering bin pump system span various industries, each benefiting from the system's unique capabilities. In the chemical industry, the system is used to transport raw materials and finished products, ensuring safe and efficient handling of hazardous powders. The pharmaceutical industry relies on the system for precise dosing of active ingredients, where even minor variations can affect product efficacy. The food processing sector utilizes the system to handle dry ingredients, maintaining hygiene and preventing contamination. Each application leverages the system's ability to deliver consistent, high-quality powder transport, contributing to improved product quality and operational efficiency.
Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its metering bin pump systems to meet evolving industry needs. The company invests in research and development to enhance system performance, durability, and energy efficiency. By staying at the forefront of technology, HeadPowder ensures its products remain competitive and reliable in the market. The company's commitment to customer service extends beyond the initial sale, with dedicated technical support and maintenance services available to clients. This approach builds long-term relationships and ensures that clients receive the support needed to maximize the system's performance and lifespan.
The metering bin pump powder conveying system represents a significant advancement in powder handling technology, offering solutions to the challenges of transporting bulk materials with precision and reliability. By combining advanced engineering with practical design, the system addresses the needs of modern industrial operations, providing a cost-effective and efficient method for powder transport. As industries continue to demand higher standards of material handling, the metering bin pump system remains a vital component in achieving operational excellence. Shandong HeadPowder Engineering Co., Ltd. plays a key role in advancing this technology, providing industries with the tools they need to succeed in a competitive market.