

Common Methods of Grain Conveying
When it comes to efficiently moving grain from one location to another, various methods are employed in the agricultural and food processing industries. Understanding these common grain conveying methods is crucial for optimizing operations, ensuring product quality, and maintaining safety standards. This article explores several prevalent techniques used by professionals in the field, highlighting their applications and benefits.
1. Screw Conveyors: A Versatile Solution for Horizontal and Slight Inclined Transport
Screw conveyors, also known as auger conveyors, are widely used for transporting bulk materials, including grains, in a continuous and controlled manner. These systems consist of a rotating helical screw inside a U-shaped or tubular housing. As the screw rotates, it pushes the material forward, making them ideal for horizontal or slight inclined transport. The design allows for easy integration into existing processing lines and can handle a variety of grain types, from small seeds to larger kernels. One of the key advantages of screw conveyors is their ability to mix materials gently, which is beneficial for maintaining product integrity. They are also relatively low-maintenance and can be easily cleaned, making them suitable for food-grade applications. The HeadPowder Engineering Co., Ltd. offers high-quality screw conveyor systems tailored to meet the specific needs of grain handling operations, ensuring reliable and efficient transport solutions.
2. Bucket Elevators: Efficient Vertical Transport for Bulk Materials
Bucket elevators are essential for vertical or steeply inclined grain transport, providing a reliable method to move materials from lower to higher levels. These systems feature a continuous belt or chain with attached buckets that scoop up the grain as they travel up a vertical or inclined section. Once the buckets reach the top, they tip to discharge the material into a hopper or storage bin. Bucket elevators are known for their high capacity and ability to handle abrasive materials without significant wear. They are commonly used in grain elevators, feed mills, and processing plants where vertical transport is required. The design ensures minimal product degradation and can accommodate different grain sizes and moisture levels. Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing robust bucket elevators that deliver consistent performance and durability, supporting efficient vertical grain handling in various industrial settings.
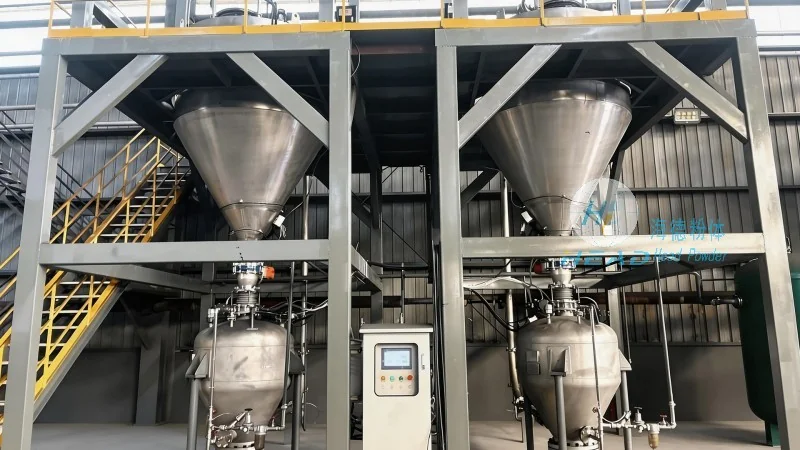
3. Pneumatic Conveying Systems: Air-Driven Transport for Flexible and Dust-Free Operations
Pneumatic conveying systems utilize air pressure to transport grain and other bulk materials through a network of pipes. These systems can be categorized into pressure or vacuum types, each offering unique advantages depending on the application. In pressure systems, compressed air pushes the material through the pipeline, while vacuum systems draw the material using a fan or blower. Pneumatic conveyors are particularly effective for handling fine powders and granular materials, as they can transport materials over longer distances with minimal loss. They also provide a dust-free environment, which is critical for maintaining product quality and worker safety. The flexibility of pneumatic systems allows for easy integration with existing processing equipment and can be adapted to various layout configurations. HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying solutions that ensure efficient, clean, and reliable transport of grain, meeting the demands of modern food processing and agricultural operations.
4. Belt Conveyors: High-Capacity Horizontal Transport for Bulk Grains
Belt conveyors are a classic and widely adopted method for horizontal grain transport, particularly in large-scale storage and handling facilities. These systems consist of a continuous belt that moves over rollers or pulleys, carrying the grain from one point to another. Belt conveyors are known for their high capacity and ability to handle large volumes of material efficiently. They are suitable for both dry and slightly moist grains and can be customized with different belt materials to resist wear and tear from abrasive products. The design allows for easy maintenance and can be extended to cover long distances with multiple sections. Belt conveyors are often used in grain terminals, silos, and processing plants where continuous and reliable transport is essential. Shandong HeadPowder Engineering Co., Ltd. offers durable and efficient belt conveyor systems that enhance the productivity of grain handling operations, ensuring smooth and consistent material movement.
5. Chain Conveyors: Robust and Versatile Transport Solutions for Heavy-Duty Applications
Chain conveyors use a series of interconnected chains to move grain and other bulk materials, making them suitable for heavy-duty and abrasive applications. These systems are often used in environments where other conveyors might experience excessive wear, such as in the handling of large kernels or mixed grains. The chains can be equipped with attachments like buckets or buckets with paddles to enhance material handling capabilities. Chain conveyors provide high load capacity and can operate under challenging conditions, including high temperatures or wet environments. They are commonly found in feed mills, grain processing plants, and industrial facilities where reliability and durability are paramount. HeadPowder Engineering Co., Ltd. manufactures robust chain conveyor systems that deliver consistent performance and longevity, supporting the efficient transport of grain in demanding industrial settings.
6. Vibrating Conveyors: Gentle and Efficient Transport for Sensitive Grains
Vibrating conveyors utilize vibration to move grain along a trough, providing a gentle and controlled transport method that is ideal for sensitive products. These systems consist of a trough that vibrates at specific frequencies, causing the material to move forward due to the shaking motion. Vibrating conveyors are particularly effective for handling fragile grains, such as wheat or barley, as they minimize product damage and maintain quality. They are also suitable for transporting materials with high moisture content or sticky properties, as the vibration helps prevent material buildup and clogging. The design allows for easy cleaning and maintenance, making them suitable for food-grade applications. Shandong HeadPowder Engineering Co., Ltd. offers advanced vibrating conveyor solutions that ensure efficient and gentle transport of grain, preserving product integrity and meeting industry standards.