

What is a Multi-functional Pneumatic Conveying System? What are its Design Principles?
Multi-functional pneumatic conveying systems represent a sophisticated technology in material handling, designed to transport bulk materials efficiently over long distances with minimal disruption to the material's properties. These systems are widely used across various industries, including food processing, pharmaceuticals, chemicals, and manufacturing, due to their ability to handle a diverse range of materials while maintaining product integrity. The core of such systems lies in their ability to combine multiple functions—like conveying, mixing, and dosing—into a single, integrated unit, making them versatile and adaptable to different operational needs.
Understanding the Core Design Principles of Pneumatic Conveying Systems
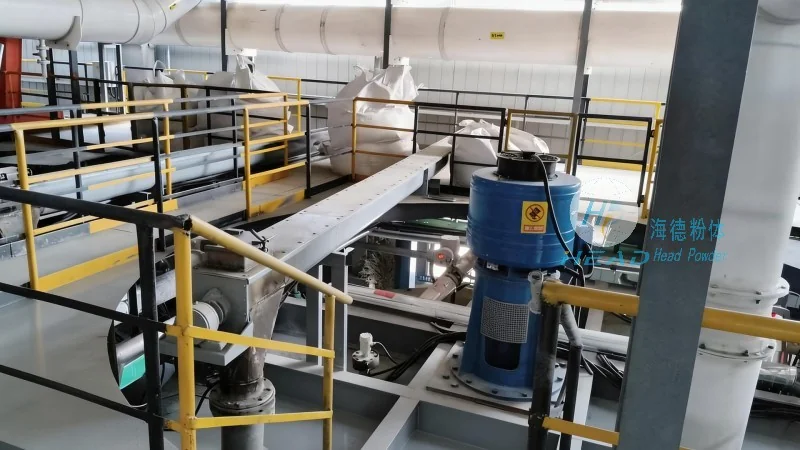
The design principles of multi-functional pneumatic conveying systems revolve around the fundamental physics of fluid dynamics and material flow. At its essence, these systems utilize compressed air or other gases to create a flow that propels bulk materials through a network of pipes. The key design considerations include the selection of the appropriate conveying medium (air or other gases), the design of the feeding and discharge mechanisms, and the integration of control systems to ensure smooth operation. Engineers must carefully calculate the air velocity, pressure, and flow rate to achieve optimal material transport without causing degradation or damage to the product. Additionally, the system's design must account for factors such as material density, particle size, and moisture content, as these variables significantly impact the conveying efficiency and system performance.
Key Components and Their Functional Roles in Multi-functional Systems
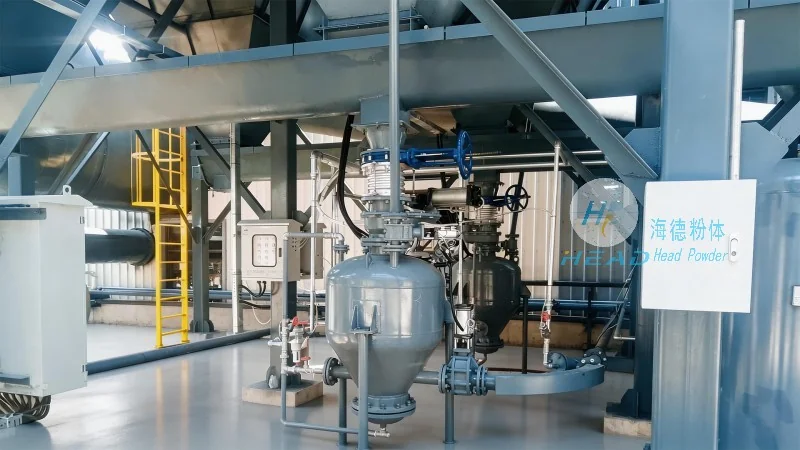
Multi-functional pneumatic conveying systems consist of several critical components, each playing a vital role in the overall operation. The primary components include the air compressor or blower, which generates the necessary pressure to move materials; the conveying pipes, which form the path for material transport; the feeding devices, such as hoppers or rotary valves, that introduce materials into the system; and the control valves and sensors that regulate the flow and pressure. In addition to these, many systems incorporate mixing chambers or dosing units, which allow for the combination of different materials or the precise control of material discharge. The integration of these components into a single system ensures seamless operation and reduces the complexity of material handling processes.
Application Scenarios and Industry Advantages of Multi-functional Pneumatic Conveying
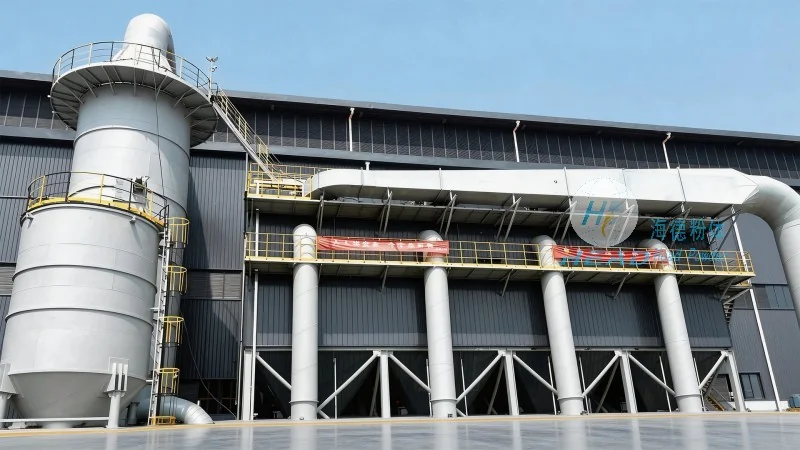
The versatility of multi-functional pneumatic conveying systems makes them suitable for a wide range of applications. In the food industry, for example, these systems are used to transport powders like flour, sugar, or spices while maintaining hygiene and preventing contamination. In pharmaceutical manufacturing, they are employed to handle sensitive materials, such as active pharmaceutical ingredients (APIs), with strict control over particle size and purity. The chemical industry also benefits from these systems, as they can handle corrosive or abrasive materials without causing damage to the equipment. Furthermore, in manufacturing and construction, multi-functional pneumatic conveying systems are used to transport raw materials, such as cement or sand, to production lines efficiently. The ability to handle diverse materials and operate in various environments makes these systems a preferred choice for many industries seeking reliable and efficient material handling solutions.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced pneumatic conveying systems, specializing in the design, development, and production of multi-functional solutions for various industrial applications. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder's products are engineered to meet the highest standards of performance, reliability, and durability, ensuring long-term operational efficiency and customer satisfaction. The company's commitment to customer needs and technological advancement has enabled it to deliver tailored solutions that address the unique challenges of each client.
Contact Information and Location
HeadPowder is headquartered in Shandong, China, with a dedicated team of engineers and technicians dedicated to research and development. The company's facilities are equipped with state-of-the-art equipment and technology, enabling the production of high-quality pneumatic conveying systems that meet international standards. The company's location in Shandong provides easy access to major transportation networks, facilitating the delivery of products to clients across the region and beyond.