

[Negative Pressure Dilute Phase Pneumatic Conveying Equipment: What It Is and Its Design Principles]
For industrial applications requiring efficient and reliable material handling, negative pressure dilute phase pneumatic conveying systems offer a sophisticated solution. These systems are engineered to transport bulk materials through a pipeline using a vacuum or negative pressure to draw material from a source to a destination. Understanding the fundamentals of this technology, along with its design principles, is crucial for optimizing performance and ensuring operational efficiency in various industries.
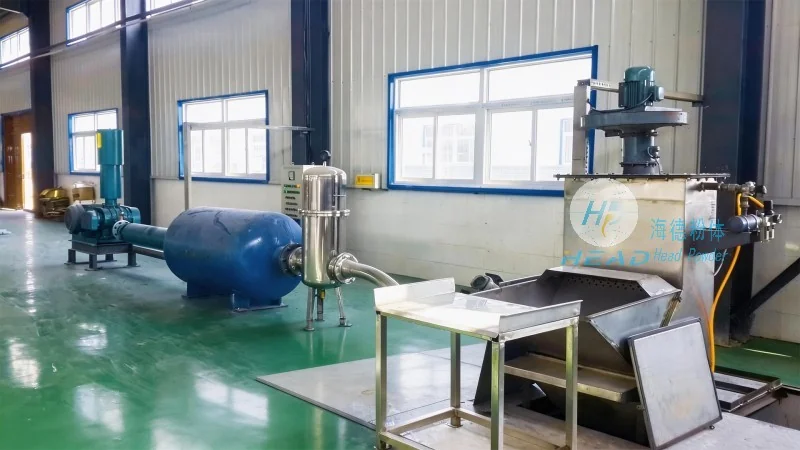
What Is Negative Pressure Dilute Phase Pneumatic Conveying?
Negative pressure dilute phase pneumatic conveying systems operate by creating a vacuum in the conveying line, which draws material particles into the air stream. Unlike positive pressure systems that push material through the pipeline, negative pressure systems pull material from the source, often making them ideal for applications where dust control and material containment are critical. The "dilute phase" refers to the low concentration of material particles in the air stream, which allows for high conveying velocities and reduced system complexity compared to dense phase systems.
Key Design Principles of Negative Pressure Dilute Phase Systems
The design of a negative pressure dilute phase system involves several critical principles that ensure effective material transport. First, the system must be capable of generating sufficient negative pressure to draw material from the source. This typically requires a powerful vacuum pump or fan, which is sized based on the material's properties, such as particle size, density, and moisture content. Second, the pipeline layout is carefully planned to minimize pressure losses and ensure consistent material flow. Factors like pipe diameter, length, and bends are optimized to maintain the required conveying velocity and prevent material deposition or blockages.
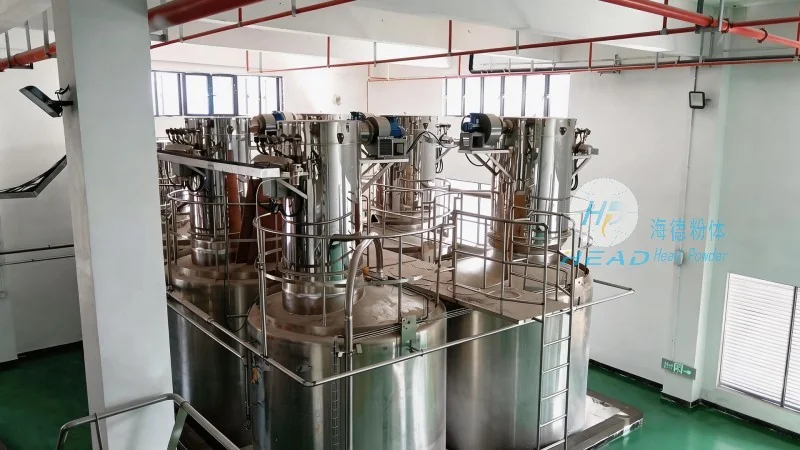
Third, the system incorporates appropriate filtration and separation components to handle the air stream after material transport. This includes cyclones or bag filters that separate the material from the air, allowing the air to be recirculated or discharged safely. The design also considers the source and destination equipment, such as hoppers or silos, which must be integrated seamlessly to facilitate smooth material transfer. Additionally, safety features like pressure relief valves and overpressure protection are essential to prevent system failures and ensure compliance with industrial safety standards.
Applications and Benefits of Negative Pressure Dilute Phase Conveying
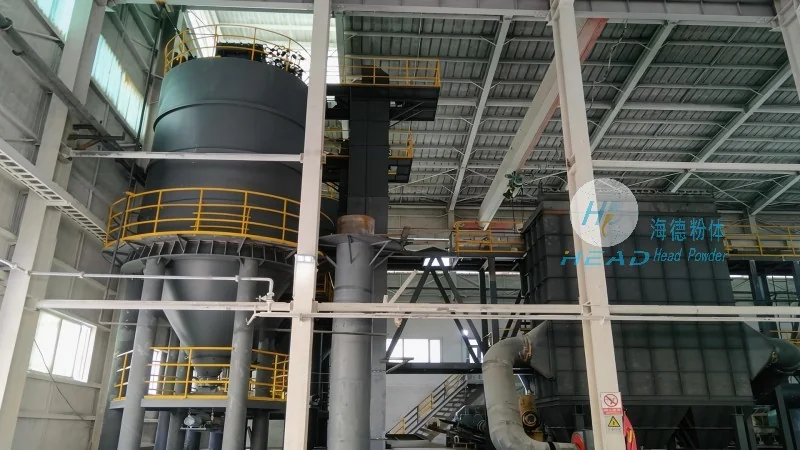
These systems are widely used in industries such as pharmaceuticals, food processing, and chemical manufacturing, where the need for clean, dust-free material handling is paramount. The benefits of negative pressure dilute phase systems include improved process safety, reduced material degradation, and enhanced environmental control. By minimizing dust emissions and preventing material contamination, these systems contribute to higher product quality and operational efficiency. Furthermore, the flexibility of negative pressure systems allows for easy integration into existing production lines, making them a cost-effective solution for upgrading or expanding material handling capabilities.
About Shandong HeadPowder Engineering Co., Ltd.
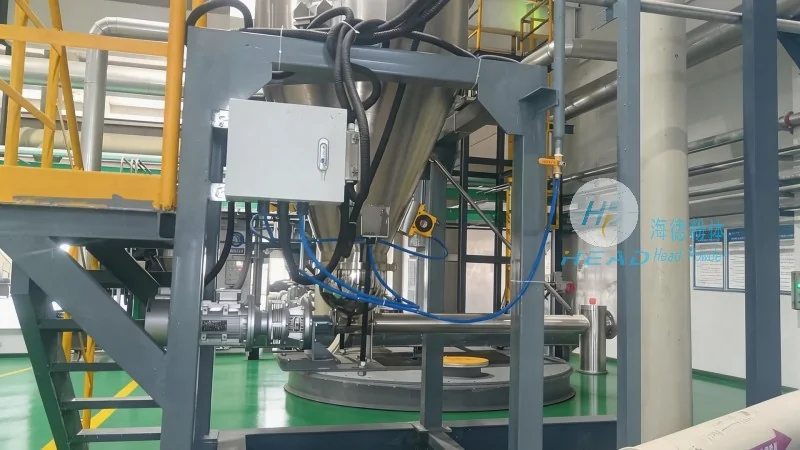
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company has built a reputation for delivering high-quality equipment tailored to the specific needs of various industries. HeadPowder's expertise in negative pressure dilute phase systems ensures that clients receive reliable, efficient solutions that meet their operational requirements. The company's commitment to quality and service has made it a trusted partner for businesses seeking to optimize their material handling processes.
Location and Contact Information
HeadPowder is headquartered in Shandong, China, with a dedicated team of engineers and technicians dedicated to providing comprehensive support for its clients. The company's facilities are equipped with state-of-the-art technology and testing equipment, enabling the development of customized solutions that address the unique challenges of each project. By leveraging its experience and expertise, HeadPowder continues to advance the field of pneumatic conveying, offering cutting-edge solutions that enhance industrial productivity and sustainability.