

What is a Fermented Powder Pneumatic Conveying Machine? And Its Design Principles
For those in the industrial sector dealing with powdered materials, especially fermented powders, understanding the technology behind efficient material handling is crucial. A fermented powder pneumatic conveying machine is a specialized piece of equipment designed to transport these fine powders through a system of air pressure and flow. This article will explore what this machine is and delve into its fundamental design principles, providing insights into how it operates and its importance in industrial processes.
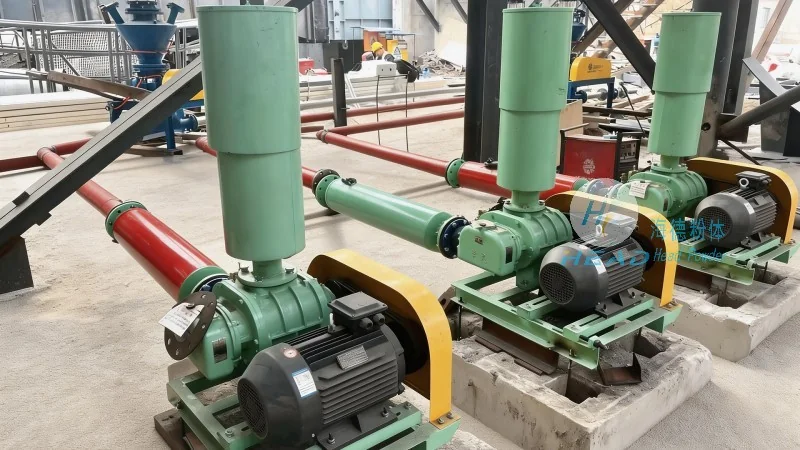
Understanding the Fermented Powder Pneumatic Conveying Machine
A fermented powder pneumatic conveying machine is a system that uses compressed air or other gas to move powdered materials, such as fermented powders, from one location to another. These machines are commonly used in industries like food processing, pharmaceuticals, and chemical manufacturing where the handling of fine powders requires precision and control. The core function of this equipment is to ensure the safe, efficient, and consistent transport of fermented powders, minimizing the risk of dust contamination and material loss.
Key Components and Their Roles
The operation of a fermented powder pneumatic conveying machine relies on several key components that work in tandem to achieve effective material transport. These components typically include a hopper for material storage, a feeder to control the flow of powder, a conveying line where the material is transported, and a receiver for the material's final destination. The system may also incorporate filters to capture any fine particles and maintain air quality, as well as pressure regulators to manage the air pressure within the system.
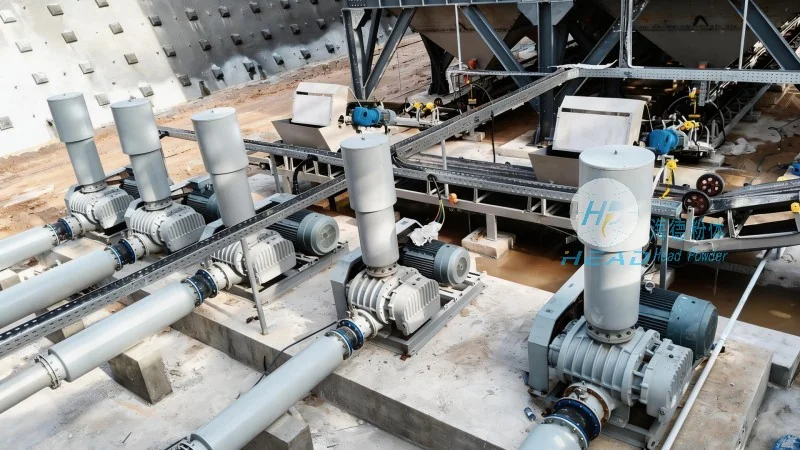
The Design Principles Behind the Machine
The design principles of a fermented powder pneumatic conveying machine are centered around the principles of fluidization and air flow. The machine operates by creating a low-pressure zone at the material inlet and a high-pressure zone at the outlet, causing the air to flow through the conveying line and carry the powder particles along with it. The velocity of the air is a critical factor; it must be sufficient to lift and transport the powder without causing excessive wear on the equipment or creating excessive dust. The design also considers the particle size and density of the fermented powder, as these properties affect the air velocity required for effective transport.
Advantages of Using a Fermented Powder Pneumatic Conveying Machine
Implementing a fermented powder pneumatic conveying machine offers several advantages over traditional material handling methods. One of the primary benefits is the ability to transport materials in a closed system, which helps prevent dust contamination and environmental pollution. This is particularly important for fermented powders, which may contain allergens or other contaminants that need to be contained. Additionally, pneumatic conveying systems can handle materials at a high rate, improving production efficiency and reducing downtime. The equipment is also relatively compact and can be easily integrated into existing industrial setups, making it a flexible solution for various applications.
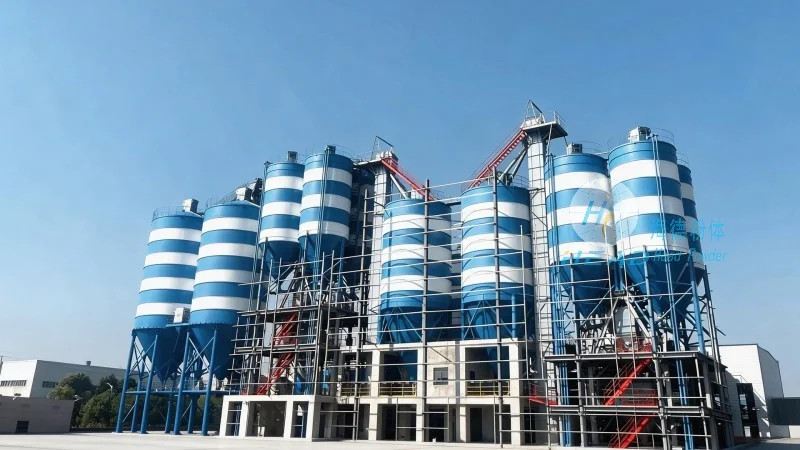
Applications in Industrial Settings
Fermented powder pneumatic conveying machines are widely used in various industrial applications where the handling of fine powders is essential. In the food industry, for example, these machines are used to transport fermented powders used in the production of beverages, snacks, and other food products. In the pharmaceutical industry, they are employed to handle powders used in the manufacturing of medications, ensuring that the materials are transported in a sterile and controlled environment. The chemical industry also utilizes these machines for transporting powders used in the production of fertilizers, coatings, and other chemical products.
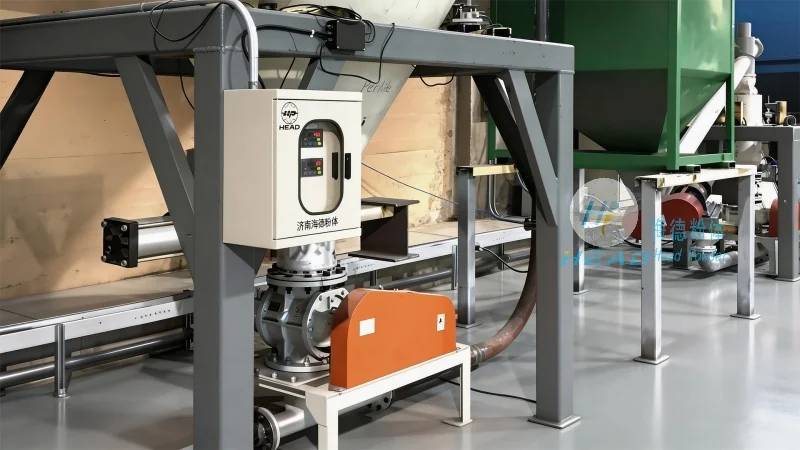
Customization and Integration by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of fermented powder pneumatic conveying machines tailored to meet the specific needs of their clients. With a focus on quality and innovation, the company offers customized solutions that integrate seamlessly into existing industrial processes. The company's expertise lies in understanding the unique properties of fermented powders and designing machines that optimize material transport while minimizing operational costs. By leveraging advanced engineering techniques and materials, Shandong HeadPowder Engineering Co., Ltd. ensures that their products are durable, efficient, and reliable, providing long-term value to their customers.
Conclusion
In conclusion, a fermented powder pneumatic conveying machine is a vital piece of equipment for industries dealing with fine, fermented powders. Its design principles, centered on air flow and fluidization, enable efficient and controlled material transport. The advantages of using such a machine, including dust containment and high transport rates, make it an essential component in modern industrial operations. For those seeking reliable and customized solutions, Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner, providing high-quality equipment that meets the demands of the industry.