

What is Shredded Paper Powder Conveying Equipment? And What Are Its Design Principles?
Shredded paper powder conveying equipment is a specialized system designed to handle and transport fine, shredded paper particles efficiently. This equipment is crucial in various industrial and waste management applications where the safe and effective movement of shredded paper material is required. The design of such equipment is tailored to address the unique challenges posed by the physical properties of shredded paper, including its fine particle size, potential for static charge, and susceptibility to clogging or blockage in traditional conveying systems.
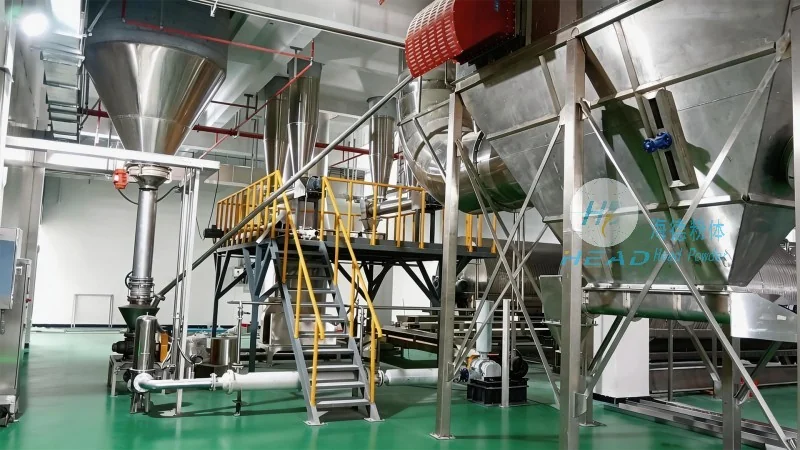
Overview of Shredded Paper Powder Conveying Equipment
Shredded paper powder conveying equipment typically consists of several key components that work in tandem to ensure reliable material transport. These components may include a hopper or feed inlet for receiving the shredded paper, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and a control system to regulate the flow and operation. The equipment is engineered to handle the abrasive and fine nature of shredded paper, minimizing wear and tear on components while maintaining consistent performance.
Design Principles for Efficient Powder Conveying
The design principles behind shredded paper powder conveying equipment focus on maximizing efficiency, minimizing downtime, and ensuring the safety of operators and the environment. Key design considerations include: material handling capacity, which determines the volume of shredded paper that can be processed per hour; the type of conveying mechanism, which affects the speed and uniformity of material movement; and the ability to prevent clogging, which is critical for maintaining continuous operation. Engineers at Shandong HeadPowder Engineering Co., Ltd. employ advanced design methodologies to optimize these factors, ensuring that the equipment meets the specific needs of each application.
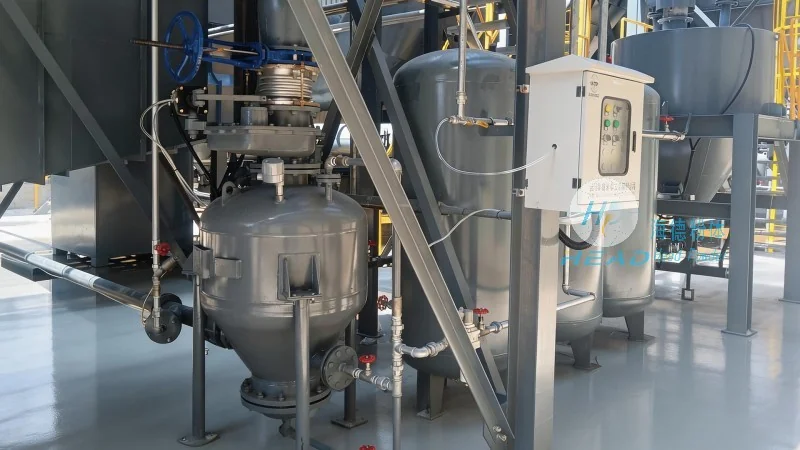
Key Components and Their Functions
Each component of shredded paper powder conveying equipment plays a vital role in the overall system. The hopper or feed inlet is designed to accommodate the shredded paper material, providing a consistent feed to the conveyor. The conveyor mechanism, whether it is a screw conveyor, pneumatic system, or belt conveyor, is selected based on the material's properties and the desired conveying distance. For example, screw conveyors are often used for horizontal or slight incline transport due to their ability to handle fine powders without excessive pressure, while pneumatic conveyors are suitable for longer distances or when the material is highly abrasive. The control system, which may include sensors and variable speed drives, allows for real-time monitoring and adjustment of the conveying process, enhancing efficiency and reducing waste.
Material Handling and Safety Considerations
When handling shredded paper powder, safety is a top priority. The equipment is designed with features that minimize the risk of dust explosions, such as proper grounding to dissipate static charge and the use of explosion-proof components where necessary. Additionally, the design ensures that the material is contained within the system, preventing airborne dust from spreading and causing health hazards. The equipment is also constructed from materials that are resistant to corrosion and wear, ensuring long-term durability and low maintenance costs. Shandong HeadPowder Engineering Co., Ltd. adheres to strict safety standards and regulations, ensuring that their conveying equipment meets or exceeds industry requirements for both performance and safety.
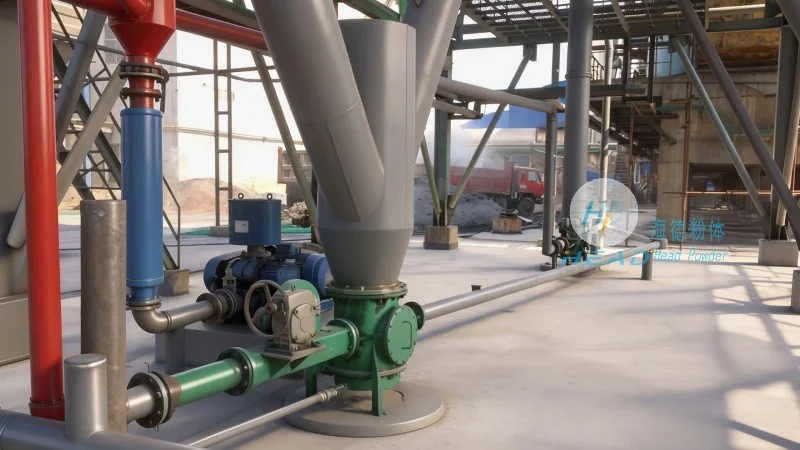
Applications and Industry Use Cases
Shredded paper powder conveying equipment is widely used in various industries, including waste management, recycling, and industrial processing. In waste management facilities, the equipment is used to transport shredded paper from collection bins to processing units, where it may be further processed into pulp or other materials. In recycling plants, the equipment helps move shredded paper to sorting and baling equipment, facilitating the recycling process. Industrial applications may include the use of shredded paper as a raw material in manufacturing processes, where the equipment ensures a consistent supply of material to production lines. The versatility of shredded paper powder conveying equipment makes it an essential tool in modern material handling operations.
Advantages of Shredded Paper Powder Conveying Equipment
There are several advantages to using specialized shredded paper powder conveying equipment over traditional methods. First, the equipment is highly efficient, with the ability to transport large volumes of material with minimal energy consumption. Second, it reduces the risk of material loss or contamination, as the system is enclosed and controlled. Third, the equipment is designed for low maintenance, with components that are easy to replace and service, reducing downtime and operational costs. Finally, the equipment is scalable, allowing it to be customized to meet the specific needs of different applications, from small-scale operations to large industrial facilities. These advantages make shredded paper powder conveying equipment a cost-effective and reliable solution for handling shredded paper material.